Why Is a Cleanroom Dehumidifier Essential?
A cleanroom can look spotless while its air quietly carries too much moisture. Humidity affects particles, materials, equipment, and worker comfort. It can also disturb pressure balance and make contamination controls harder to maintain. This is why a Cleanroom Dehumidifier deserves serious attention in pharmaceutical, electronics, medical device, and research environments.
In practice, humidity control begins with measured conditions, not guesses. Sensors placed at representative points can reveal moisture changes near doors, airlocks, cooling coils, and production equipment. A dehumidifier then removes excess water vapor before condensation appears on ducts, ceilings, or sensitive surfaces. That protection supports more stable processes and reduces avoidable maintenance problems. Small changes matter.
However, installing any unit is not enough. The system must match room volume, air changes, temperature, process loads, and required humidity limits. Experienced facility teams review trend data, calibration records, filter condition, and drainage performance. They also confirm that airflow does not create dead zones or disturb critical work areas. Poor sizing can waste energy and still leave wet corners.
No system is perfect. Door openings, seasonal weather, cleaning activities, and equipment heat can create unexpected moisture loads. Regular monitoring helps identify these weaknesses before they become expensive failures. A thoughtful Cleanroom Dehumidifier strategy combines engineering calculations, practical observation, documented maintenance, and ongoing verification. Its value is not only drier air. It is greater control, clearer evidence, and more dependable cleanroom performance.
What Is a Cleanroom Dehumidifier?
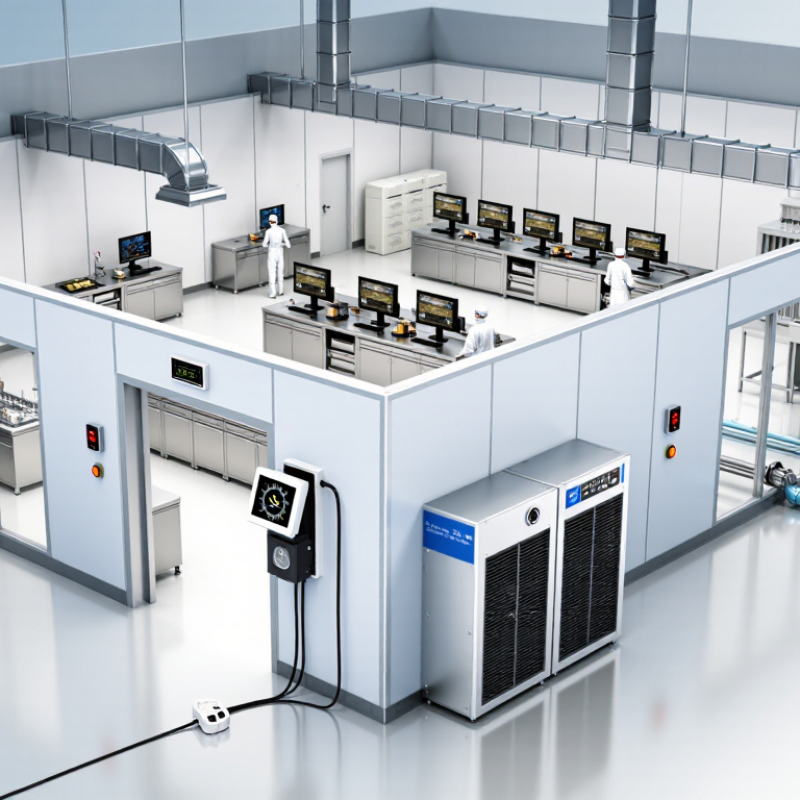
A cleanroom dehumidifier is a controlled air-treatment system that removes excess moisture from cleanroom air. It helps maintain a stable relative humidity level, often selected according to the process, materials, and facility requirements. Unlike an air purifier, it does not mainly remove particles. Its primary task is moisture control.
Many systems use cooled coils, desiccant material, or both. Moist air passes through the equipment, where water vapor is condensed or absorbed. Drier air then returns through the room’s circulation system. Sensors continuously measure temperature and humidity near critical work areas. Small changes matter. A few hours of high humidity can cause condensation, corrosion, packaging problems, or unstable powders.
In practice, operators should check sensor readings against independent instruments. Calibration cannot be treated as a one-time task. Filters, drain lines, coils, and desiccant components also need documented inspection. A neglected drain may create standing water, even when the display looks normal. That detail is easy to miss.
A reliable system must match the room’s airflow, heat load, door activity, and production schedule. Oversizing may cause unnecessary cycling and uneven conditions. Undersizing may leave corners damp. Validation records should connect equipment performance with actual room conditions, not only factory specifications. Perfect control is difficult, and assumptions sometimes fail during seasonal weather changes.
Why Is a Cleanroom Dehumidifier Essential?
Moisture Content of Air at 20°C
At 20°C, air can hold approximately 17.3 g/m³ of water vapor at 100% relative humidity. The chart shows how absolute moisture content increases as relative humidity rises. A cleanroom dehumidifier helps maintain a stable humidity setpoint, reducing the risk of condensation, material moisture absorption, corrosion, and process variation.
Why Humidity Control Matters in Cleanrooms
Why Humidity Control Matters in Cleanrooms
Humidity control protects more than comfort. It supports particle control, product stability, operator safety, and reliable production results. ISO 14644-1:2015 classifies cleanrooms by airborne particle concentration, but it does not prescribe one universal humidity range. Each facility must define limits according to its process, materials, and risk assessment.
The U.S. Environmental Protection Agency recommends keeping indoor relative humidity below 60%, ideally between 30% and 50%, to reduce moisture-related microbial growth. Cleanroom operators often use tighter limits.
Excess moisture can leave condensation on cold surfaces, encourage corrosion, and affect powders or hygroscopic materials. Dry air creates another problem. The ASHRAE Handbook reports that low humidity increases electrostatic discharge risk, especially when sensitive equipment and insulating materials are present.
Small details matter. A poorly sealed door can admit damp air during every material transfer. A dehumidifier helps remove this hidden load before it disturbs room conditions.
Continuous monitoring also matters, because a displayed average can conceal short humidity spikes. FDA guidance on pharmaceutical manufacturing emphasizes controlled environmental conditions and documented monitoring, not assumptions.
No setpoint is perfect. A limit suitable for sterile filling may not suit a powder process. Facilities should review sensor location, seasonal changes, and recovery time after door openings.
In practice, humidity control works best when linked to airflow, pressure, cleaning, and maintenance records. The difficult part is often not installing equipment. It is noticing the quiet variation before it becomes a batch problem.
Key Benefits for Contamination and Process Control
A cleanroom dehumidifier protects more than comfort. It stabilizes moisture where particles, microbes, and sensitive materials can disrupt production. Excess humidity can create condensation on cooling coils, walls, tools, and exposed product surfaces. Even a small wet patch can become a contamination concern.
ISO 14644-1:2015 classifies cleanrooms by airborne particle concentration. For example, an ISO Class 5 room allows no more than 3,520 particles per cubic metre at 0.5 micrometres. Humidity is not a particle-class requirement, but it influences particle behavior, static charge, and cleaning performance. ASHRAE’s HVAC Applications guidance identifies moisture control as an important part of reducing microbial growth and protecting processes. The risk is often gradual.
Process control also depends on repeatable moisture conditions. Hygroscopic powders may absorb water and change flow characteristics. Coatings can dry unevenly. Electronic assemblies may face static-related handling problems when humidity falls too low. A dehumidifier helps maintain the specified relative humidity, especially when outdoor air loads change quickly.
Practical experience still matters. Sensors can drift, doors may remain open, and operators may overlook wet insulation. That is why calibrated humidity probes, alarm limits, and documented trend reviews deserve attention. ASHRAE Standard 55 commonly references 30% to 60% relative humidity for general occupied environments, but cleanrooms often require tighter, process-specific limits. The wrong target can be as troublesome as no target.
How to Choose and Maintain the Right Unit
Why Is a Cleanroom Dehumidifier Essential?
How to Choose and Maintain the Right Unit
A cleanroom dehumidifier controls moisture that ordinary air-conditioning may leave behind. Excess humidity can support microbial growth, damage sensitive materials, and disturb powder handling. It may also cause condensation on cold surfaces. In controlled manufacturing, stable humidity protects both product quality and process repeatability.
Choose the unit according to room volume, air changes, infiltration, personnel, and moisture released by equipment. A small office-style unit is rarely suitable. Check its capacity at the actual operating temperature, not only the advertised rating. Desiccant systems often perform better when very low humidity is required. Refrigerant systems can be practical for moderate targets. The required setpoint depends on the process. Many facilities operate near 40–50% relative humidity, but this range is not universal. Validate it against product and regulatory requirements.
Maintenance must be scheduled, recorded, and verified. Inspect filters, coils, desiccant wheels, drain lines, seals, and alarm functions. Clean accessible surfaces without releasing particles into the room. Calibrate humidity and temperature sensors against a traceable reference. Compare the control display with an independent meter. Small differences matter.
A common mistake is selecting capacity from room size alone. Moisture loads change when doors open or production increases. Review trend data each month. Check dew point near critical equipment. Replace parts before performance becomes unstable, although replacement intervals should follow measured condition rather than guesswork. Maintenance plans sometimes look complete but overlook drainage. That detail can become a serious failure.



 Português do Brasil