Global purchasing demands more than attractive samples. Buyers need consistent color, durable surfaces, and dependable delivery across different markets. Uv Cured Printing helps meet these expectations by curing ink instantly with ultraviolet light. The process creates sharp graphics on rigid materials, including acrylic, glass, metal, wood, and coated boards. Finished products can leave the printer almost immediately. That shorter production cycle may support tighter packaging and shipping schedules.
The practical value becomes clearer through real orders. A retail display may arrive with clean edges after a long ocean journey. A branded panel may resist light scratches during warehouse handling. However, no printing method is perfect. Poor surface preparation, unsuitable ink, or incorrect curing can reduce adhesion. Color differences may also appear between batches, especially when materials change. Experienced suppliers should provide material testing, color references, curing records, and pre-shipment photographs. These details make international communication more reliable.
Trust matters.
Global orders also require responsible planning. Packaging should protect corners, surfaces, and delicate mounting parts. Product specifications must remain clear, including dimensions, tolerances, finishes, and approved artwork. Regional safety, labeling, and import requirements should be checked before production. Reliable manufacturers explain these limits instead of promising impossible results. They should also discuss recyclable packaging, waste reduction, and realistic lead times. Uv Cured Printing can be an efficient choice, but its success depends on disciplined preparation. The strongest decision combines technical evidence, supplier experience, and honest review of each product’s actual use.
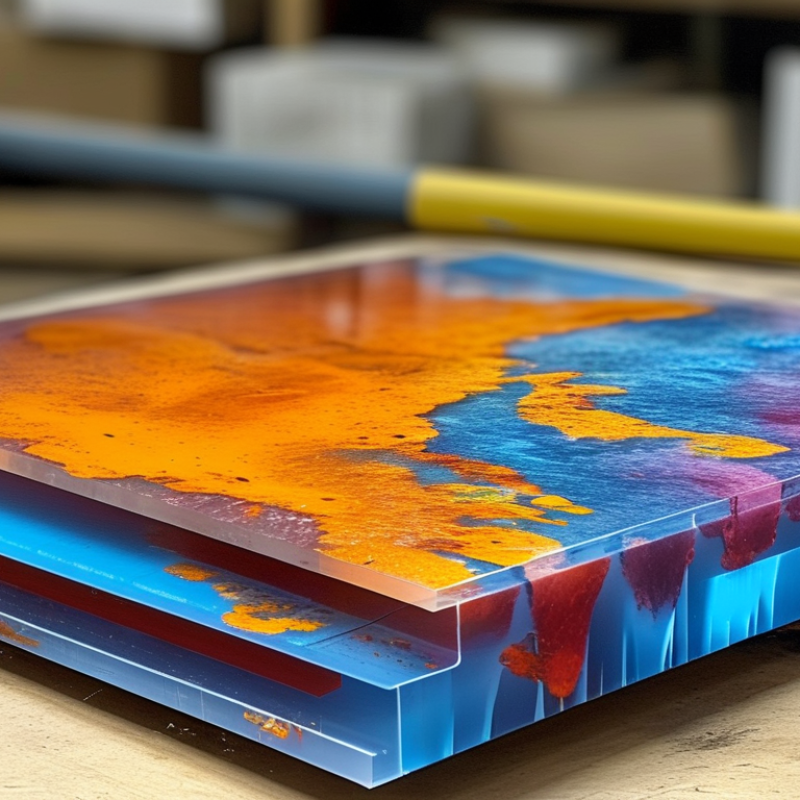
UV-cured printing suits global orders because finished products can be handled almost immediately. Its main advantage comes from 100% solids inks and instant polymerization. These inks contain no traditional solvent that evaporates during drying. Instead, ultraviolet energy triggers a chemical reaction, converting liquid ink into a solid film.
In production, this difference is easy to notice. A printed panel can leave the press with minimal waiting time. It can then move to inspection, packing, and international shipping. The cured surface often delivers sharp text, dense color, and strong adhesion on materials such as coated board, acrylic, glass, and selected plastics. However, substrate testing remains essential. Surface energy, texture, and heat sensitivity can change the result.
Reliable printing requires more than a fast curing lamp. Operators should check lamp intensity, ink laydown, surface cleanliness, and curing speed. A simple rub test can reveal weak adhesion before packing begins. Color samples should also be approved under consistent lighting. In my experience, “instant” does not mean every print is equally durable. Thick ink layers, dark colors, or poorly maintained lamps may need closer inspection. That small weakness matters. Careful records, repeatable settings, and honest quality checks make international deliveries more dependable.
Why Choose UV Cured Printing for Global Orders?
UV cured printing can improve production efficiency for international orders. RadTech reports that UV LED curing may reduce energy use by up to 70%. This figure is significant, but it is not automatic. Results depend on lamp power, print speed, substrate, and curing settings.
In practical production, UV LED systems cure ink immediately under focused light. Printed sheets can move directly to cutting, packing, or inspection. This reduces waiting time and may lower heat exposure on sensitive materials. Lower energy demand also supports more predictable operating costs across facilities. Still, I would not treat the 70% figure as a guarantee. A poorly calibrated system can waste energy and create uneven curing.
Tips: Ask suppliers for measured energy data, not general promises. Compare wattage, curing speed, maintenance needs, and expected service life. Request samples on your actual materials. Small tests often reveal issues that specifications miss. Keep records from each production run, including lamp settings and rework rates. This evidence helps teams improve future global orders.
Global orders often face rough handling, long transit times, and changing warehouse conditions. UV cured printing helps protect printed surfaces during these demanding journeys. The ink hardens immediately under ultraviolet light. This leaves the surface dry before sheets are stacked, packed, or moved.
That timing matters. Wet or partially dried ink can transfer between stacked sheets, creating set-off marks. Friction can also cause scuffing around edges, dark areas, and fine text. With a properly cured surface, cartons are less likely to show rubbing damage during loading and unloading. Printed colors and sharp details remain easier to inspect when shipments arrive across borders.
Printed colors and sharp details remain easier to inspect when shipments arrive across borders.
Still, instant curing is not a perfect solution. I have seen poor results when the curing energy was too low or the material was difficult to print. Surface testing remains essential. A simple rub test, tape test, and visual inspection can reveal weak adhesion before packing. Ink coverage, substrate texture, and packaging pressure also affect performance.
Careful packing still matters. Use protective sheets when needed, avoid excessive stacking pressure, and allow space for handling. These small decisions reduce avoidable marks. Reliable global shipping depends on both the printing process and the preparation around it.
Global orders face abrasion, humidity, sunlight, and uneven storage. UV curing hardens ink immediately under ultraviolet energy. This creates a crisp surface with little waiting time. Yet “cured” does not mean permanently damage-proof.
ASTM D3359 measures coating adhesion using a crosshatch and pressure-sensitive tape. Its 0B-to-5B scale records coating removal. A 5B result shows no visible squares lifting. Lower ratings reveal weak bonding, especially on textured or low-energy substrates.
ISO 4892-3 exposes samples to fluorescent UV and condensation cycles. Typical cycles use eight hours of UV at 60°C, followed by four hours of condensation at 50°C. These conditions imitate outdoor stress, but they cannot represent every climate. A 2024 Smithers industry report forecasts strong digital-print growth through 2028, increasing demand for repeatable durability evidence. Market forecasts vary by segment, so broad predictions need caution.
Tips: Request test panels from the actual substrate. Record ASTM D3359 ratings before shipment. Ask for ISO 4892-3 cycle details, irradiance, and color-change measurements. Check edges, folds, and dark panels after testing. A perfect laboratory score still cannot predict every warehouse. That uncertainty deserves documentation.
Global orders demand more than sharp color and fast delivery. They also require responsible production across varied environmental standards. UV cured printing can support this goal through low-VOC inks and 100% solids formulations. These inks cure under ultraviolet light instead of relying on solvent evaporation. Less solvent can improve air quality around the pressroom.
In practical production, operators may notice less solvent odor near the equipment. There is also less wet ink waiting for drying or disposal. A cured sheet can often move directly to cutting, packing, or inspection. That shorter workflow may help international orders maintain consistent schedules. However, low-VOC does not mean impact-free. UV lamps consume energy, and uncured ink still requires careful handling. Some substrates need adhesion tests, rub tests, and full-cure checks.
For dependable export production, printers should request current safety data and VOC documentation. They should verify curing performance at the actual press speed, lamp intensity, and material thickness. Records matter. A retained test sheet can explain why one batch performed differently during transit. Requirements vary by destination, product use, and local waste rules. I would avoid promising universal compliance without reviewing those details. A cautious review may take longer, but it reduces costly surprises.
| Evaluation Dimension | Conventional Solvent Printing | Water-Based Printing | UV-Cured, 100% Solids Printing | Global-Order Relevance |
|---|---|---|---|---|
| Formulation basis | Uses organic solvents that evaporate during drying. | Uses water as the primary carrier; additives or co-solvents may still be present. | Uses reactive components that polymerize under UV light. A true 100% solids formulation contains no intentionally added evaporative carrier. | A clear formulation description supports environmental documentation across different markets. |
| VOC potential | Generally higher VOC potential because solvent carriers evaporate. | Generally lower VOC potential than solvent systems, but the actual level depends on the formulation. | Typically very low VOC emissions during curing when a 100% solids formulation is used; confirm the exact value in the product SDS or technical data sheet. | Lower VOC potential can simplify reviews against regional air-quality requirements, subject to local rules. |
| Drying or curing mechanism | Solvent evaporation followed by film formation. | Water evaporation, often supported by heated air or controlled drying. | Photopolymerization initiated by UV energy; the printed layer solidifies when adequately exposed. | Fast curing can reduce handling time and support shorter production-to-shipment schedules. |
| Typical post-print handling | May require ventilation, drying time, and solvent-emission controls. | May require additional drying time, especially at high ink coverage or in humid conditions. | Can normally be handled immediately after complete curing, provided the print surface passes quality and adhesion checks. | Reduces the risk of blocking, smearing, or transfer during packing when curing is properly controlled. |
| Material utilization | Part of the applied ink volume is lost as solvent evaporates. | Part of the applied volume is water or other carrier that evaporates during drying. | The cured film is formed mainly from the applied ink solids; there is no carrier-loss mechanism in a genuine 100% solids system. | Supports more predictable ink consumption and helps reduce evaporative material loss. |
| Substrate flexibility | Commonly used on selected flexible films and coated materials. | Often effective on absorbent or specially coated substrates; drying performance varies by material. | Can print on many non-porous materials, including coated boards, plastics, glass, metal, and selected flexible substrates, subject to ink adhesion testing. | Broad substrate compatibility can reduce the need for separate processes for different destination markets. |
| Environmental compliance checkpoint | Review VOC limits, ventilation requirements, worker exposure controls, and waste-handling obligations. | Review formulation additives, wastewater or rinse-water handling, and local VOC requirements. | Review the SDS, photoinitiator content, residual-monomer information, curing validation, and end-use restrictions. | Compliance is determined by the complete ink, substrate, process, and end use—not by the printing technology alone. |
| Best-fit benefit | Useful where strong solvent resistance and flexible-film performance are required. | Useful where water-based chemistry and absorbent-substrate compatibility are priorities. | Combines low-VOC potential, rapid curing, high material utilization, and broad substrate options. | A practical option for international orders that need documented environmental performance and efficient fulfillment. |
Note: “Low-VOC” and “100% solids” claims should be verified against the specific ink’s safety data sheet, technical data sheet, curing conditions, and the regulations applicable in the destination country. UV curing does not automatically make every printed product suitable for food contact, medical, or other regulated applications.
| Cookie | Duration | Description |
|---|---|---|
| AWSALB | 7 days | AWSALB is a cookie generated by the Application load balancer in the Amazon Web Services. It works slightly different from AWSELB. |
| AWSALBCORS | 7 days | This cookie is used for load balancing services provded by Amazon inorder to optimize the user experience. Amazon has updated the ALB and CLB so that customers can continue to use the CORS request with stickness. |
| cookielawinfo-checkbox-advertisement | 1 year | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Advertisement". |
| cookielawinfo-checkbox-analytics | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytic / Performance". |
| cookielawinfo-checkbox-functional | 11 months | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional". |
| cookielawinfo-checkbox-necessary | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Strictly Necessary". |
| cookielawinfo-checkbox-performance | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance". |
| cookielawinfo-checkbox-preferences | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Preferences." |
| elementor | never | This cookie is used by the website's WordPress theme. It allows the website owner to implement or change the website's content in real-time. |
| viewed_cookie_policy | 11 months | The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data. |
| Cookie | Duration | Description |
|---|---|---|
| CONSENT | 16 years 4 months | These cookies are set via embedded youtube-videos. They register anonymous statistical data on for example how many times the video is displayed and what settings are used for playback.No sensitive data is collected unless you log in to your google account, in that case your choices are linked with your account, for example if you click “like” on a video. |
| _ga | 2 years | This cookie is installed by Google Analytics. The cookie is used to calculate visitor, session, campaign data and keep track of site usage for the site's analytics report. The cookies store information anonymously and assign a randomly generated number to identify unique visitors. |
| _gat_gtag_UA_47200144_1 | 1 minute | This cookie is set by Google and is used to distinguish users. |
| _gid | 1 day | This cookie is installed by Google Analytics. The cookie is used to store information of how visitors use a website and helps in creating an analytics report of how the website is doing. The data collected including the number visitors, the source where they have come from, and the pages visted in an anonymous form. |
| _hjAbsoluteSessionInProgress | session | This cookie is used to count how many times a website has been visited by different visitors. This is done by assigning the visitor an ID, so the visitor does not get registered twice. |
| _hjFirstSeen | 30 minutes | This is set by Hotjar to identify a new user’s first session. It stores a true/false value, indicating whether this was the first time Hotjar saw this user. It is used by Recording filters to identify new user sessions. |
| _hjid | 1 year | This cookie is set by Hotjar. This cookie is set when the customer first lands on a page with the Hotjar script. It is used to persist the random user ID, unique to that site on the browser. This ensures that behavior in subsequent visits to the same site will be attributed to the same user ID. |
| _hjIncludedInPageviewSample | session | This cookie is used to detect whether the user navigation and interactions are included in the website’s data analytics. |
| Cookie | Duration | Description |
|---|---|---|
| IDE | 1 year 24 days | This cookie is used by Google DoubleClick and stores information about how the user uses the website and any other advertisement before visiting the website. This is used to present users with ads that are relevant to them according to the user profile. |
| NID | 6 months | This cookie is used to a profile based on user's interest and display personalized ads to the users. |
| test_cookie | 15 minutes | This cookie is set by doubleclick.net. The purpose of the cookie is to determine if the user's browser supports cookies. |
| VISITOR_INFO1_LIVE | 5 months 27 days | This cookie is set by Youtube it is used to track the information of the embedded YouTube videos on a website. |
| YSC | session | This cookies is set by Youtube and is used to track the views of embedded videos. |
| yt-remote-connected-devices | never | These cookies are set via embedded youtube-videos. |
| yt-remote-device-id | never | These cookies are set via embedded youtube-videos. |
| Cookie | Duration | Description |
|---|---|---|
| qtrans_front_language | 1 year | This cookie is set by qTranslate WordPress plugin. The cookie is used to manage the preferred language of the visitor. |