Why Choose a Screw Air Compressor?
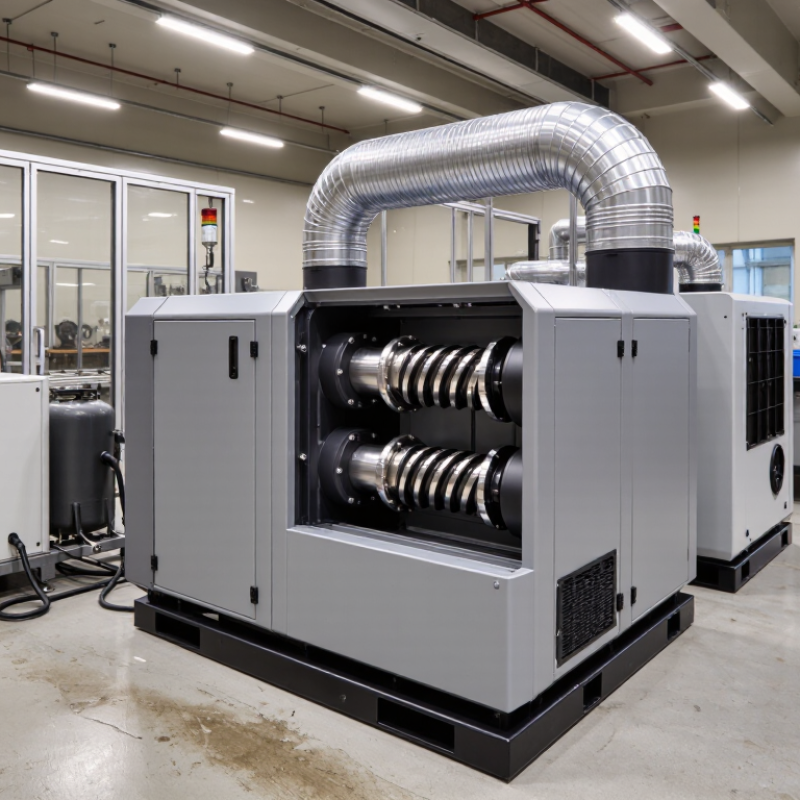
Choosing the right air system affects production speed, energy use, and maintenance costs. A screw air compressor is often selected for stable, continuous compressed-air demand. Its rotating twin screws deliver a steady flow without the repeated impact of piston movement. This can support factories, workshops, packaging lines, and automated equipment.
The practical advantage becomes clearer during long operating shifts. A properly sized unit can run smoothly while maintaining consistent pressure. Oil-injected models may also include cooling and separation systems for demanding industrial work. Oil-free designs serve applications where air purity is especially important. However, the machine is not automatically the best choice for every business. A small workshop with occasional tool use may spend too much on unused capacity.
Real decisions require more than comparing purchase prices. Engineers usually review flow requirements, pressure losses, duty cycles, ambient temperature, and available service support. Manufacturer data and recognized industry guidance should inform this assessment. Installation details matter too. A clean intake, suitable ventilation, and regular filter replacement can protect performance. Condensation may still appear in poorly designed systems. That detail is easy to overlook.
Experience also shows that efficiency claims need careful checking. Variable-speed control can reduce wasted energy during changing demand, but savings depend on actual operating patterns. Maintenance records, noise levels, access to spare parts, and technician expertise should influence the final decision. Some assumptions may prove wrong after installation. A reliable choice is not simply the most advanced model. It is the compressor that matches real demand, operating conditions, and long-term responsibilities.
How Twin-Screw Compression Delivers Stable Airflow at 7–13 bar
Why Choose a Screw Air Compressor?
How Twin-Screw Compression Delivers Stable Airflow at 7–13 bar
Twin-screw compressors use two intermeshing rotors to compress air continuously. This differs from piston compressors, which deliver pulsating airflow. At 7–13 bar, continuous compression helps maintain steady pressure for pneumatic tools, packaging lines, and automated valves. The airflow feels smoother at the point of use.
Variable-speed control can adjust rotor speed as demand changes. A receiver, correctly sized dryer, and clean filters still matter. Without them, pressure can fluctuate despite a good compressor. CAGI Performance Verification Data Sheets compare flow, pressure, input power, and specific power under defined conditions. These values help engineers assess real operating efficiency rather than relying on catalogue claims.
It is easy to overstate the benefit.
The U.S. Department of Energy’s Improving Compressed Air System Performance guide reports that leaks may waste 20–30% of compressor output in poorly maintained systems. That loss can hide the advantages of stable twin-screw compression. Field checks should include pressure at the compressor and at the farthest machine. A two-bar drop across piping, filters, or dryers may reveal the real problem. ISO 1217 provides standardized methods for measuring compressor capacity and power, supporting more reliable comparisons between operating units. Stable airflow is therefore a system result, not only a rotor design feature.
Why Choose a Screw Air Compressor?
Twin-screw compression uses continuous rotary compression to maintain a steady discharge pressure with low pulsation across the typical 7–13 bar operating range. The representative operating profile below shows the pressure remaining close to each setpoint during constant air demand.
Why Variable-Speed Drives Can Reduce Compressor Energy Use by up to 35%
Why Choose a Screw Air Compressor?
Why Variable-Speed Drives Can Reduce Compressor Energy Use by up to 35%
A screw air compressor suits facilities needing steady, reliable compressed air. Its rotary design supports continuous operation with fewer sudden pressure changes. Yet the motor can waste energy when production demand changes. A fixed-speed compressor keeps running near full capacity, even during quieter periods. Variable-speed drives adjust motor speed to match real-time air demand. This reduces unloading time and unnecessary electrical consumption. Smaller speed changes can produce noticeable savings over long operating hours.
In a properly sized system, energy reductions can reach up to 35%. The exact result depends on pressure settings, leakage, duty cycles, and maintenance quality. The honest answer is less perfect: savings are not guaranteed. An energy audit should measure demand before equipment selection. Installers should also check air storage, pipe restrictions, and control settings. A pressure sensor and power meter can reveal problems that sound alone cannot detect. That evidence makes the investment easier to evaluate.
Tips: Record compressor power during busy and quiet shifts. Repair leaks near couplings, drains, and hoses. Avoid setting pressure higher than the process requires. Review filters regularly, because blockage increases operating resistance. Allow room for future demand, but do not oversize casually. That mistake can reduce efficiency.
How Air-Leak Losses Can Reach 20–30% of Compressed-Air Output
Why Choose a Screw Air Compressor?
A screw air compressor suits facilities that need steady air throughout long production shifts. Its rotary design delivers a smoother flow than many intermittent compressor types. However, the compressor itself may not be the largest source of energy loss. Air leaks can consume 20–30% of compressed-air output in poorly maintained systems.
I have seen leaks hidden behind machines, under hoses, and around quick couplers. Some sounded like a faint hiss, while others required ultrasonic detection. A small leak may seem harmless. Several hundred small leaks are not. The compressor then runs longer, increases power use, and struggles to maintain working pressure. This creates heat, noise, and avoidable maintenance work.
Leak control needs measurement, not guesswork. Record compressor running hours, system pressure, and production demand. Check pipe joints during quiet periods. An ultrasonic survey can locate leaks that ordinary listening misses. Repair results should be verified, because a repaired fitting can still leak under vibration. A simple assumption can be wrong.
Screw compressors can support this work through stable output and suitable control systems. Variable-speed operation may reduce waste when demand changes, but it cannot fix an open pipe joint. Correct sizing matters too. An oversized unit may cycle inefficiently, while an undersized unit may run continuously. The best decision combines load data, pressure requirements, maintenance access, and a realistic leak-reduction plan.
How ISO 8573-1 Classifies Compressed-Air Purity for Different Industries
Choosing a screw air compressor begins with purity, not only pressure or energy use. ISO 8573-1:2010 defines compressed-air purity through particles, water, and oil. Each category receives a class from 0 to 9. Class 0 is the strictest, but it does not mean zero contamination. Users must define the limits and test methods. That detail is often missed.
Food processing may require very low oil and microbial risk at the point of use. Electronics manufacturing needs controlled particles and moisture. Pharmaceutical production usually demands tighter limits, validated filtration, and documented testing. A designation such as Class 1:2:1 describes particles, water, and oil separately. For oil, Class 1 allows no more than 0.01 mg/m³ total oil under the standard’s conditions. Water Class 1 can require a pressure dew point below -70°C.
A screw compressor does not automatically produce clean air. Oil-injected designs need separators, filters, dryers, and careful drain management. Oil-free designs still require downstream filtration and clean distribution piping. The U.S. Department of Energy’s Improving Compressed Air System Performance sourcebook reports that leaks can waste 20–30% of compressor output in poorly maintained systems. That waste also increases contamination risk when pressure falls. The imperfect part is practical: a precise class target can still fail when sampling is weak, filters are overloaded, or maintenance records are incomplete. ISO 8573-1 should guide testing, not replace it.
Which Screw Compressor Size Matches Demand, Duty Cycle, and Pressure?
Why Choose a Screw Air Compressor?
Which screw compressor size matches your demand, duty cycle, and pressure? Start with measured air demand, not motor horsepower. The U.S. Department of Energy reports that compressed air can consume 10% of industrial electricity. Its system sourcebook also notes that leaks may waste 20–30% of compressor output. A 75 kW machine may look impressive, yet it can run inefficiently at low demand. That creates heat, cycling, and unnecessary energy costs.
Check free air delivery at your required pressure. A compressor rated at 8 bar may deliver less air at 10 bar. Record peak flow, average flow, and overnight demand for at least one production week. Then compare those figures with the compressor’s duty cycle. Continuous processes usually need a unit designed for stable base-load operation. Intermittent tools may need storage capacity instead of a larger compressor. Pressure loss matters, too. A long, narrow pipe can quietly force higher discharge pressure.
Tips: Keep a demand log. Test for leaks during shutdown. Size for real peaks, not guesses. The Compressed Air and Gas Institute recommends using standardized performance data when comparing compressor packages. ISO 1217 testing also helps verify flow and power claims. Still, field conditions can differ from laboratory results. I have seen “correctly sized” systems struggle after filters became blocked. Leave practical margin, but question every extra kilowatt. Oversizing feels safe. It often is not.



 Português do Brasil