Why Choose a High Speed Diaper Packing Machine?
A High-speed diaper packing machine can transform a busy production line. It combines faster bagging, controlled counting, and consistent sealing in one coordinated system. For manufacturers, the attraction is clear: more finished packs can leave the line each hour.
“Speed has value only when accuracy and product protection keep pace,” says Dr. Elena Marquez, a packaging automation specialist with experience in hygiene-product manufacturing. Her observation reflects a practical truth. A machine may run quickly, yet poor alignment can crush diapers, wrinkle film, or create weak seals.
A High-speed diaper packing machine typically uses servo-driven feeding, optical sensors, and programmable counting systems. These features help maintain pack quantity and reduce unnecessary manual handling. Picture the process: diapers arrive in an even stack, the film wraps tightly, and a sensor checks the pack before sealing. Small details matter.
Less waste matters too.
Stable speed can support predictable labor planning and lower film consumption. However, speed alone should never define the purchase decision. Operators must examine changeover time, cleaning access, noise, maintenance support, and compatibility with different diaper sizes.
The fastest machine is not always the best machine. A poorly matched system can cause downtime during product changes. That weakness is easy to overlook.
This article explores why manufacturers choose high-speed packing technology, where it delivers measurable value, and which limitations deserve careful review. It also considers real production conditions, because impressive specifications do not automatically guarantee reliable daily performance.
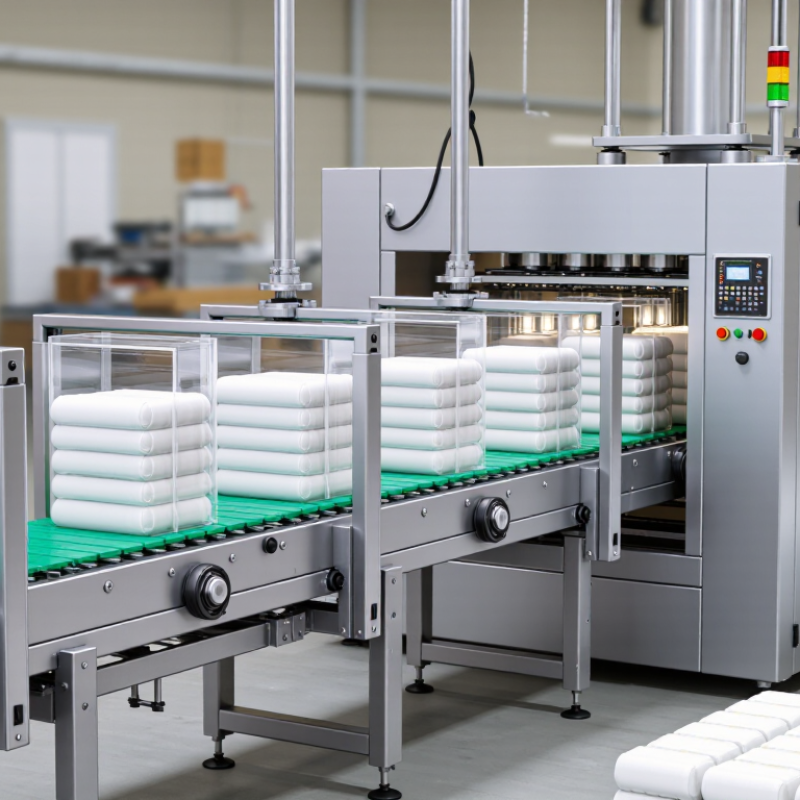
Define High-Speed Diaper Packing: 60–120 Bags per Minute
Why Choose a High Speed Diaper Packing Machine?
Define High-Speed Diaper Packing: 60–120 Bags per Minute
High-speed diaper packing usually means producing 60 to 120 sealed bags every minute. At 60 bags per minute, the machine completes one bag each second. At 120 bags per minute, that interval falls to half a second. This definition gives manufacturers a practical reference, rather than relying on vague claims. However, the actual result depends on diaper size, bag dimensions, folding accuracy, and product arrangement.
In daily production, the machine must coordinate feeding, counting, stacking, bag opening, filling, sealing, and discharge. A stable line should keep bags aligned while maintaining consistent seal pressure. Operators also watch film tension, sensor response, and rejected packs. Small delays can reduce output quickly. A five-minute adjustment may affect hundreds of bags.
Speed alone is not enough. A fast machine that creates open seals or uneven stacks may increase waste and inspection time. Experienced teams test performance with the intended diaper type and packaging material. They record continuous output, changeover time, stoppages, and acceptable pack quality. The advertised 120 bags per minute may only apply to selected conditions. That caveat matters. Real production can be slower, especially during size changes or material variation. Careful testing often reveals more than a single impressive number.
Why Choose a High Speed Diaper Packing Machine? — Define High-Speed Diaper Packing: 60–120 Bags per Minute
The following production benchmarks explain how high-speed diaper packing affects output, cycle time, labor planning, and production efficiency. Values are calculated from the stated bagging speed and are not tied to any company or brand.
| Operating Speed | Cycle Time per Bag | Theoretical Output per Hour | Estimated Good Output per Hour* | Theoretical Output per 8-Hour Shift | Typical Production Benefit |
| 60 bags/min | 1.00 second | 3,600 bags | 3,060 bags | 28,800 bags | Suitable for consistent medium-volume production and flexible product changeovers. |
| 75 bags/min | 0.80 second | 4,500 bags | 3,825 bags | 36,000 bags | Provides a useful balance between packing capacity, equipment utilization, and operating flexibility. |
| 90 bags/min | 0.67 second | 5,400 bags | 4,590 bags | 43,200 bags | Helps support higher daily demand while reducing the number of packing lines required for the same target. |
| 105 bags/min | 0.57 second | 6,300 bags | 5,355 bags | 50,400 bags | Appropriate for high-throughput operations that need greater capacity within limited floor space. |
| 120 bags/min | 0.50 second | 7,200 bags | 6,120 bags | 57,600 bags | Maximizes line capacity for large-volume production, provided feeding, sealing, film supply, and quality control keep pace. |
*Estimated good output assumes an 85% effective operating rate after allowing for normal stops, material loading, adjustments, inspections, and minor downtime. Actual output varies with diaper size, bags per pack, package dimensions, film properties, changeover frequency, reject rate, and machine configuration. Theoretical output is calculated as bags per minute × 60 minutes × 8 hours.
Map the Packing Process: Feeding, Counting, Stacking, Sealing, and Coding
Why Choose a High Speed Diaper Packing Machine?
A high speed diaper packing machine connects feeding, counting, stacking, sealing, and coding in one controlled process. The feeding system moves diapers steadily from the production line. Guided belts help prevent tilted products and sudden gaps. Small errors grow. Stable feeding protects every later step.
Counting sensors identify the required quantity for each pack. Servo-driven mechanisms then stack diapers with consistent alignment.
Operators should test different sizes, absorbency levels, and packaging speeds before full production. A setting that works for newborn diapers may fail with larger products.
That is often overlooked. Practical trials reveal problems that manuals cannot predict.
The sealing unit controls film tension, temperature, and pressure. These settings influence package strength and appearance. Excess heat can damage the film, while weak pressure may create open edges.
After sealing, the coding system prints production dates, batch details, or traceable information. Cameras or manual checks can verify readability. Coding errors are easy to miss during a fast shift. Regular inspection remains necessary.
High speed improves output, but it also exposes poor calibration quickly. A reliable machine should support clear adjustments, safe access, accurate counting, and consistent records throughout the packing process.
Measure Real Output with the 85% World-Class OEE Benchmark
Why Choose a High Speed Diaper Packing Machine?
Measure Real Output with the 85% World-Class OEE Benchmark
A high-speed diaper packing machine should be judged by real output, not its advertised speed. The 85% OEE benchmark offers a practical reference for serious production planning. OEE combines availability, performance, and quality. For example, a machine may run 600 packs per minute, but frequent film changes reduce its actual result. Ten-minute stops, jammed bags, and rejected packs quickly change the calculation. Real output matters more than impressive numbers.
A reliable assessment records every shift. Track planned production time, stop duration, running speed, and accepted packs. Then separate mechanical losses from material issues and operator delays. A clean dashboard helps engineers find repeated problems. A five-minute sensor adjustment may protect hundreds of packs each hour. However, 85% is not guaranteed. Real plants rarely maintain it every shift. A first calculation can also be too optimistic. Teams should check downtime records against production reports and review the method regularly.
Tips: Measure OEE over several weeks, not one unusually strong shift. Record minor stops, even those lasting under two minutes. Compare identical products and package sizes. Train operators to report causes clearly, without blaming individuals. Check seal quality at the packing line, not only in final inspection. If performance remains below 85%, improve one loss category at a time. A slower, stable machine may sometimes deliver more accepted packs than a faster machine with repeated stoppages.
Compare Labor, Film Waste, Downtime, and Production Capacity
Why Choose a High Speed Diaper Packing Machine?
Labor costs often rise quietly during each packing shift. A high-speed machine can reduce repetitive loading, counting, sealing, and case preparation. One operator may monitor several stations instead of manually checking every pack. However, staffing needs depend on layout, product variety, and changeover skill. More speed does not remove the need for trained supervision.
Film waste deserves close attention. Precise film feeding can reduce loose edges, uneven seals, and rejected packs. On a busy line, small errors can consume hundreds of meters of film each day. Servo control and automatic tension adjustment help maintain consistent package length. Still, waste figures must come from your own production records, not a sales estimate.
Downtime affects capacity more severely than a slower rated speed. A jammed conveyor, sensor fault, or long film change can stop the entire line. In practical audits, operators should record stoppage minutes, restart time, and common fault locations. A machine rated for 800 packs per minute may produce less if it stops frequently. That number is only a reference. Maintenance access, spare parts, and changeover procedures often decide real output. High speed helps most when uptime remains stable, though this assumption should be tested during normal production.
Why Choose a High Speed Diaper Packing Machine?
Comparison of labor requirements, film waste, downtime, and production capacity
Based on a representative operating comparison: labor decreases from 2 operators to 1, film waste from 4.5% to 2.0%, unplanned downtime from 12% to 6%, and production capacity increases from 120 to 300 diapers per minute. The chart shows the resulting percentage improvement when moving to a high-speed packing machine.
Select Key Specifications for Different Diaper Sizes and Pack Formats
Why Choose a High Speed Diaper Packing Machine?
A high-speed diaper packing machine must match the product, not only the target output. During production trials, operators should measure diaper length, width, thickness, and absorbent core position. These details determine the correct infeed width and folding clearance. A newborn diaper may require gentle compression, while larger sizes need stronger airflow control and wider conveying space.
Pack format also changes the specification. Pillow bags, block-bottom bags, and multi-pack bundles need different film paths and sealing units. Check the machine’s adjustable bag length, film width range, sealing temperature, and cutter accuracy.
For example, a six-diaper pack may need a shorter stroke than a twenty-four-diaper family pack. Servo-driven adjustment can reduce changeover time, but only when recipes are correctly stored and verified.
Do not chase speed alone.
A practical line should maintain stable stacking, clear barcode positioning, and consistent seals at the required rate. Sensors should detect missing diapers, tilted stacks, and empty film rolls. Operators also need safe access for cleaning and format changes. Small details matter.
One common mistake is selecting maximum speed before testing the smallest and largest sizes. Production data may expose uneven compression or film wrinkles. That feedback should change the specification, even if the original plan looked efficient. Pilot tests with real materials remain more reliable than catalogue numbers.



 Português do Brasil
