Why Choose a Burr Oak Fin Press for Your Business?
Choosing the right fin press can shape production quality, operating costs, and customer trust. For many manufacturers, a Burr Oak Fin Press offers a practical path toward stable, repeatable fin production. Its value should be judged through real factory needs, not brand recognition alone.
In a working metal shop, small details matter. Coil thickness, material hardness, fin height, and pitch can change performance quickly. A suitable press can help maintain accurate forming across long production runs. Consistent feeding also reduces scrap, rework, and unexpected downtime. Operators may appreciate clear controls, accessible tooling, and service support when schedules become demanding. These features matter beside the machine’s headline speed.
Still, careful evaluation is essential. No press can correct poor material preparation or careless setup. We have seen strong equipment deliver weak results when tooling alignment was ignored. That is an uncomfortable lesson, but an important one. Buyers should compare output requirements, energy use, tooling options, maintenance access, and training support. Sample testing can reveal issues that brochures hide. Ask for documented specifications and realistic production references.
A Burr Oak Fin Press may suit businesses seeking dependable fin forming and scalable capacity. The best choice depends on your products, workforce, floor space, and growth plans. Review the complete process before committing. Reliable production comes from the machine, the method, and the people operating it. Performance is built daily.
What Is a Burr Oak Fin Press and How Does It Work?
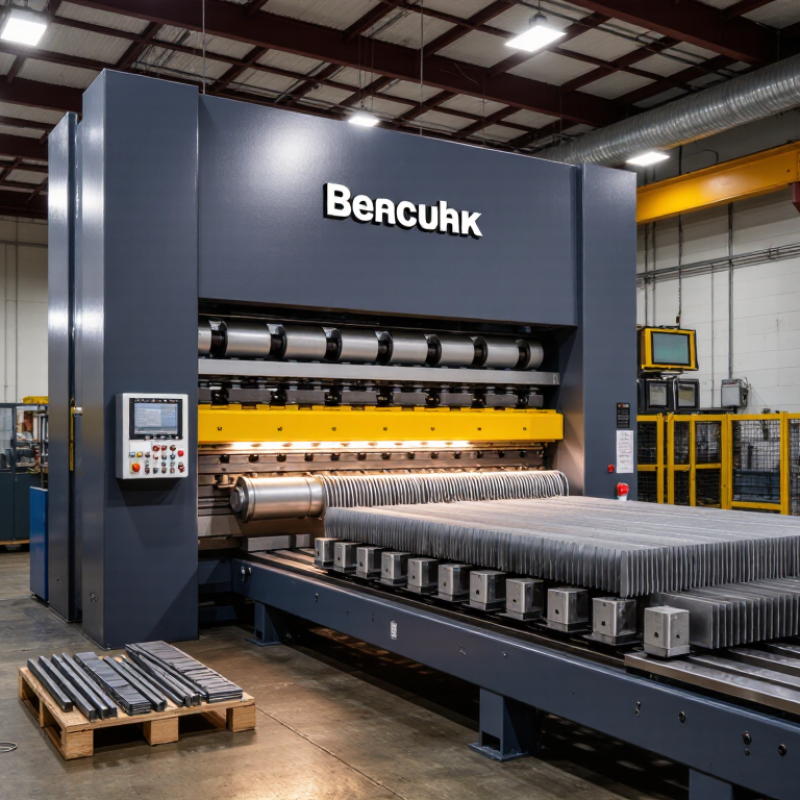
A burr oak fin press is an industrial machine for producing thin metal fins used in heat exchangers, radiators, and cooling systems. The name may describe a machine configuration or a specialized production system. Its main task is simple: shape flat metal strip into repeated fins with accurate spacing.
The process begins with a coil of aluminum or another suitable metal. Feed rollers guide the strip into a forming die. Inside the press, punches cut holes, collars, louvers, or edges while the material advances in measured steps. A crankshaft or servo mechanism controls each stroke. The die then forms the fin profile and separates finished pieces when required. Consistent pitch matters. Small errors can reduce airflow and create difficult assembly problems.
For a business, this equipment can improve output and reduce manual handling. It also supports repeatable dimensions across long production runs. Operators should check die wear, strip tension, lubrication, and scrap levels every shift. These details sound minor. They are not. A poorly aligned tool may create burrs, wrinkles, or uneven fin height. In my experience, faster pressing is not always better; stable feeding often protects quality more effectively. Capacity estimates should include setup time, maintenance, material changes, and occasional faults. No press runs perfectly forever. A practical purchase decision should also consider guarding, operator training, replacement tooling, noise control, and access to qualified technical support.
Key Features That Define Burr Oak Fin Press Performance
Why Choose a Precision Fin Press for Your Business?
Key Features That Define Fin Press Performance
A reliable fin press begins with a rigid frame and controlled forming pressure. These features help produce fins with consistent height, spacing, and edge quality. In practical shop use, alignment matters as much as pressing force. A small tool shift can create uneven channels across a full coil. Servo-driven control can improve repeatability during long production runs. Operators can also adjust speed, stroke length, and feed distance for different materials. That flexibility reduces setup time when production requirements change.
Tooling quality directly affects output. Hardened forming dies resist wear and help maintain accurate fin geometry. A stable feeding system prevents scratches, buckling, and inconsistent pitch. Safety guards, emergency stops, and clear controls support dependable daily operation. No machine removes every risk. Setup mistakes still happen. Regular inspections remain essential.
Tips: Check die alignment before each shift. Measure fin height at several points, not just one. Record pressure, speed, and material thickness during testing. These notes help technicians repeat successful settings. Leave room for adjustment; real materials rarely behave perfectly. A press may perform well in trials, yet reveal vibration or feeding issues during extended production. Reviewing those details honestly leads to better maintenance decisions and more reliable output.
How a Burr Oak Fin Press Supports Efficient Fin Production
Efficient fin production depends on controlled forming, steady material flow, and repeatable machine settings. A well-designed fin press supports these requirements during demanding production runs. It shapes thin metal strips with consistent pitch, height, and profile. That consistency helps heat exchangers maintain predictable airflow and thermal performance.
Operators can adjust feed speed, forming pressure, and tool alignment for different materials. Copper and aluminum may require different settings. Small changes matter. A practical operator checks the first pieces with calipers before increasing production speed. This simple step can reveal uneven ridges, burrs, or shifting alignment early. It also reduces avoidable scrap.
The press should provide clear access for cleaning and routine inspection. Lubrication points, cutting edges, and guide components need regular attention. In real workshops, maintenance is sometimes delayed during busy orders. That is a weakness, not a feature. A written inspection schedule can improve reliability without slowing the line significantly. Accurate controls also help newer operators produce acceptable fins sooner, although training remains necessary. No fin press removes every production risk. Material variation, worn tooling, and incorrect setup can still affect results. Careful records make those problems easier to trace and correct.
Industries and Applications Served by Burr Oak Fin Presses
Why Choose a Burr Oak Fin Press for Your Business?
A burr oak fin press forms precise fins for heat exchangers, radiators, condensers, and evaporators. Its value appears across automotive, HVAC, refrigeration, power electronics, and aerospace production. In practice, fin height, pitch, and material thickness directly affect airflow and thermal transfer. A stable press helps reduce variation between batches. The U.S. Department of Energy identifies industrial heat management as an important efficiency opportunity. That demand is not abstract.
The IEA Global EV Outlook 2024 reported nearly 14 million electric car sales in 2023. Battery packs, inverters, and charging systems all require dependable thermal control. Fin presses support the aluminum components used in these cooling assemblies. HVAC manufacturers face another expanding market. The IEA’s Future of Cooling report estimates that space cooling could triple electricity demand by 2050. Efficient coils will matter more.
A burr oak fin press also serves commercial refrigeration, data-center cooling, and specialized aircraft systems. These applications often require repeatable forming, narrow tolerances, and careful material handling. Production teams can adjust tooling for copper or aluminum strip. That flexibility supports different product sizes without replacing the entire process. The fit is not automatic. Poor tooling design can create fin distortion, excess scrap, or weak joints. Operators should verify press capacity, feed accuracy, maintenance access, and inspection methods before purchase. This practical review is sometimes overlooked.



 Português do Brasil