What Is a Painting Line and How Does It Work?
A Painting Line is an integrated production system that cleans, coats, cures, and inspects products. It may handle steel frames, automotive panels, appliances, or aluminum parts. Each stage affects the next. A poorly prepared surface can ruin an otherwise excellent coating.
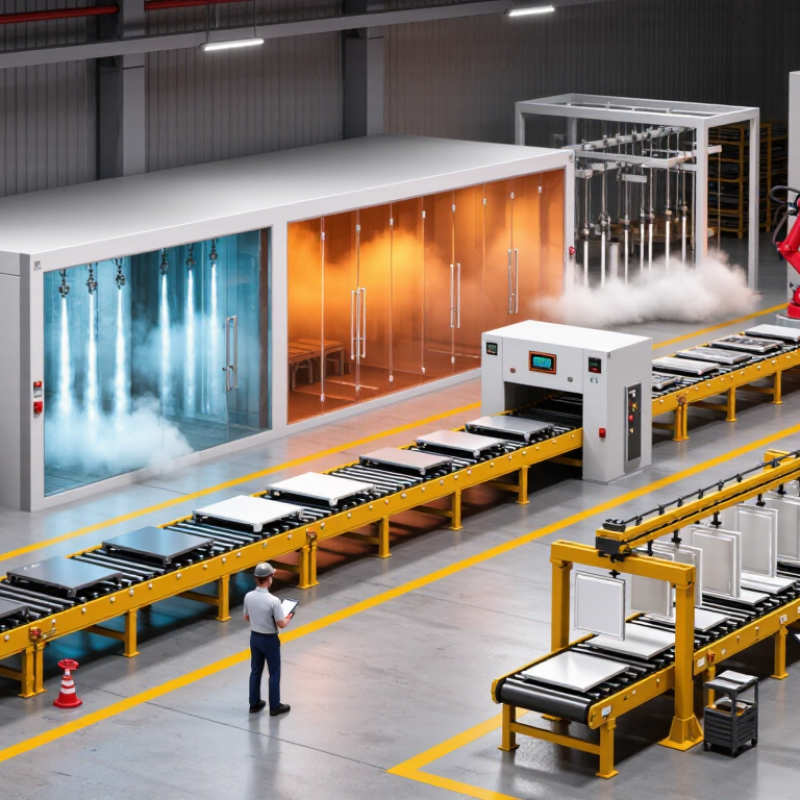
The process usually begins with loading and pretreatment. Parts may pass through washing, degreasing, rinsing, and drying zones. They then enter a spray booth or powder application area. A curing oven follows. Temperatures, conveyor speed, humidity, and film thickness must remain controlled. Small changes matter. A few seconds of extra curing can alter gloss, adhesion, or color. Rick Kline Jr., a long-time powder-coating industry editor, states the practical principle clearly: “A coating line is a system, not a single machine.” That view remains useful, although real facilities are rarely so predictable.
Market data explains the growing attention. Grand View Research valued the global paints and coatings market at approximately USD 206.56 billion in 2022. It projects continued expansion through 2030. MarketsandMarkets also forecasts growth in industrial coatings, driven by infrastructure, transportation, and manufacturing demand. These reports describe market direction, not guaranteed factory performance. That distinction matters.
A modern Painting Line can improve transfer efficiency, repeatability, and labor control. It can also consume significant energy and create costly bottlenecks. Engineers therefore balance output against air movement, oven efficiency, maintenance access, and defect rates. The best design is not always the fastest one. Sometimes, slower is more reliable. A clear understanding of each zone helps managers choose equipment, diagnose defects, and improve results without hiding the system’s imperfections.
What a Painting Line Is and What It Is Designed to Do
What Is a Painting Line and How Does It Work?
A painting line is a connected production system for cleaning, coating, drying, and checking manufactured parts. It is designed to create an even finish while reducing handling, overspray, and production delays. In a typical facility, parts travel on hooks, racks, or a conveyor through several controlled areas. The line may apply primer, color, and protective coatings. Consistency matters most.
Before coating begins, workers or machines remove oil, dust, rust, and loose particles from each surface. Cleaning improves adhesion. Drying prevents trapped moisture beneath the paint film. A spray booth then applies coating through calibrated nozzles, while airflow guides excess material toward filtration equipment. Technicians adjust spray pressure, distance, and conveyor speed according to the part’s shape. Small changes can affect the final texture. Heat or controlled air cures the coating after application, and sensors help maintain stable temperature and humidity.
Quality checks usually include visual inspection, coating-thickness measurements, and adhesion testing. Workers look for runs, pinholes, uneven edges, and missed areas. A reliable line records these results for process control and future maintenance. However, no painting line is flawless. A clogged nozzle, dirty hanger, or rushed cleaning cycle can reduce quality quickly. This is where practical judgment matters. Automated settings provide control, but experienced operators still notice details that sensors may miss. The process needs review.
Main Stages and Equipment in a Painting Line
What Is a Painting Line and How Does It Work?
Main Stages and Equipment in a Painting Line
A painting line is a connected production system for cleaning, coating, drying, and inspecting parts. It keeps each stage moving at a controlled speed. Operators load components onto a conveyor, where fixtures hold them securely. Poor positioning can leave hidden areas uncoated. That small error matters.
The process usually starts with surface preparation. Washing tanks, spray nozzles, and air knives remove oil, dust, and moisture. Some lines include chemical treatment equipment to improve coating adhesion. After preparation, parts enter the painting booth. Reciprocating spray machines or manual spray guns apply the coating evenly. Ventilation systems capture overspray and maintain stable airflow. Filters require regular inspection because blocked filters can change spray patterns.
Next, a flash-off zone allows solvents or water to escape before curing. Drying ovens then use controlled heat and airflow to harden the coating. Temperature sensors monitor the oven at several points, not just near the entrance. A conveyor drive controls residence time, while safety interlocks stop equipment during abnormal conditions. Inspection stations check color, gloss, film thickness, and surface defects. Digital gauges help, but experienced inspectors still notice texture changes that instruments may miss. No line is perfectly stable. Humidity, fixture wear, and cleaning habits can gradually affect results. A detailed maintenance record often reveals problems before they become visible on finished parts.
How Parts Move Through the Painting Process
What Is a Painting Line and How Does It Work?
A painting line moves parts through controlled preparation, coating, curing, and inspection stages. Parts usually begin on hooks, racks, or pallets. A conveyor sets the travel speed. It also controls spacing between parts.
The process often starts with washing and surface treatment. These steps remove oil, dust, and light oxidation. After rinsing, parts enter a drying zone. A spray booth then applies paint through manual, automatic, or mixed equipment.
Airflow carries overspray toward filters. The coated parts continue through a flash-off area before entering the curing oven. Temperature sensors monitor the oven, while operators check film thickness and surface appearance.
The International Federation of Robotics reported 553,052 industrial robot installations worldwide in 2022. That figure shows why automated movement is expanding. Yet robots cannot correct every poor decision. A dirty hook can mark a finished panel. Uneven spacing can create shadows and thin coating areas.
The U.S. Environmental Protection Agency’s AP-42 guidance treats spray application, flash-off, and curing as separate emission sources. This supports careful control at each stage.
A line may appear smooth from outside, but small delays can disturb the entire sequence. In practice, operators still need to question conveyor speed, oven balance, and inspection frequency. Perfect consistency is the goal. It is not always the result.
Factors That Affect Painting Line Quality and Efficiency
What Is a Painting Line and How Does It Work?
A painting line moves prepared parts through cleaning, coating, drying, and curing stations. Its quality depends on how consistently each station performs. Surface preparation is a major factor. Oil, dust, and moisture can cause craters, weak adhesion, or uneven color. Clean surfaces create a stable foundation.
Coating viscosity must match the equipment and product requirements. If the paint is too thick, spray patterns may become rough. If it is too thin, runs and poor coverage can appear. Operators should check temperature, mixing time, and viscosity during production. Small changes matter. No setting stays perfect.
Line speed also affects film thickness and output. A faster conveyor can reduce curing time and leave soft areas. Excessive spray pressure may create overspray and waste. Booth temperature, humidity, airflow, and filter condition influence both appearance and safety. Regular measurements are more reliable than visual guesses. Even experienced teams can miss gradual filter blockage. That mistake deserves review, not blame. Preventive maintenance should include nozzles, pumps, conveyors, ovens, and inspection tools. Sample panels and coating-thickness readings help confirm process stability. When defects repeat, recording their location and timing can reveal whether the cause is equipment, material, or operator technique.
What Is a Painting Line and How Does It Work?
Factors That Affect Painting Line Quality and Efficiency
The chart shows the theoretical relationship between coating-line speed and wet film thickness. It assumes a constant coating flow rate of 1 liter per minute and a coated width of 1 meter. Under these conditions, increasing line speed reduces the amount of coating applied per unit area, which can affect coverage, leveling, drying, and final paint quality.
In practice, operators balance line speed, pump flow, coating viscosity, nozzle or applicator settings, substrate preparation, oven temperature, and ventilation to achieve consistent film thickness and efficient production.



 Português do Brasil
