Industrial pipe fittings connect, redirect, divide, or close sections of a piping system. Their shapes may look simple on a bench, but each choice affects flow, pressure control, installation, and maintenance. A socket elbow, threaded tee, and welded reducer are not interchangeable. The correct option depends on pipe material, service conditions, connection method, and the space available around the line. Small details matter.
Roy A. Parisher, coauthor of Piping and Pipeline Calculations, is a relevant piping-design authority. A practical principle consistent with that field is: “Choose a fitting for its service conditions and connection—not appearance alone.” This is an editorial paraphrase, not a verified verbatim quotation. That distinction matters. Trustworthy technical guidance should separate a sourced quotation from an original summary.
This guide examines common industrial pipe fittings, including elbows, tees, reducers, couplings, unions, caps, and flanges. It explains what each fitting does, where it is typically used, and which selection details deserve attention. For example, a reducer changes pipe size, while an elbow changes direction. A flange allows a bolted connection that can be opened for inspection or repair. Yet naming a fitting is only the start. Material compatibility, pressure and temperature ratings, dimensions, and joining standards must also be checked against project requirements. A fitting can appear suitable and still fail the application. That is easy to overlook.
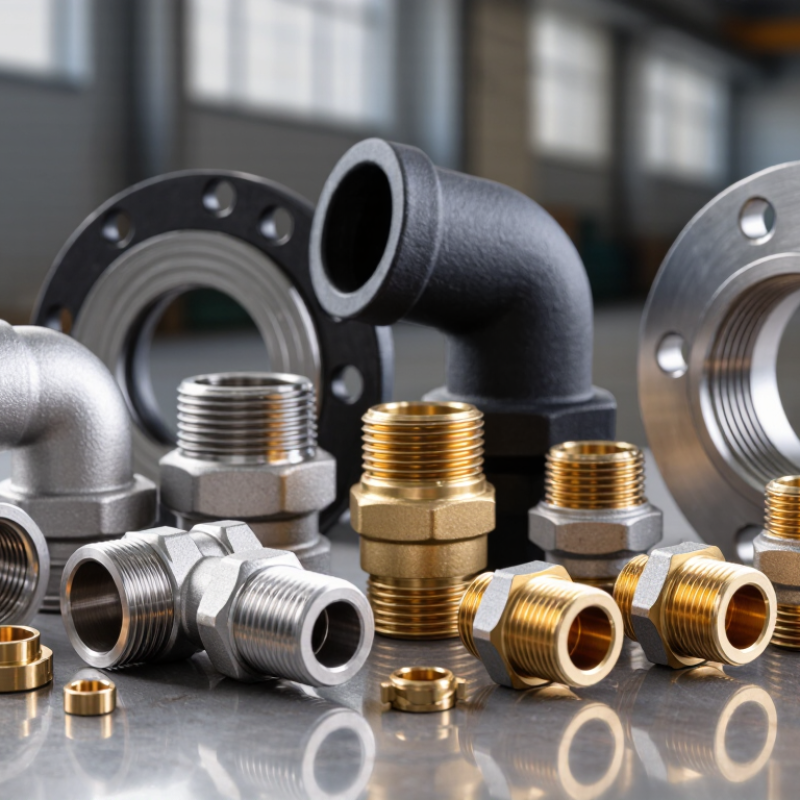
Industrial pipe fittings are commonly classified by shape and connection type. Elbows redirect flow; tees create branches; reducers change pipe diameter; caps close an open end. These shapes solve different layout problems, from turning around a beam to joining a smaller instrument line.
ASME B16.9 covers factory-made wrought butt-welding fittings from NPS 1/2 through NPS 48. That scope gives engineers a practical dimensional reference, not a substitute for checking the actual drawing.
Connection type determines how a fitting joins the pipe. Butt-weld ends are beveled and welded around the joint, while socket-weld fittings receive pipe inserted into a socket before welding. Threaded fittings screw together, and flanged fittings bolt across a gasketed face.
ASME B16.11 covers forged socket-welding and threaded fittings from NPS 1/8 through NPS 4.
Small detail. It matters.
A mismatched wall thickness or end preparation can complicate fit-up on the shop floor.
For selection, compare the fitting shape with the route, then verify size, material, pressure, temperature, and connection details against the project specification. A tee may look right on a sketch but create a poor branch entry for the flow. I still check the spool drawing carefully; a fitting name alone is not enough. Standards data helps, but real installation clearances and inspection access deserve equal attention.
Elbows redirect flow, tees create a branch, and crosses split flow in four directions. Their geometry affects pressure loss, access, and support needs.
Flow of Fluids, Technical Paper No. 410, lists resistance coefficients near 0.3 for a long-radius 90-degree elbow and about 1.0 for flow through a tee branch. These are reference values, not guarantees. Actual loss changes with fitting geometry, pipe size, and flow conditions.
A long-radius elbow is often chosen when space allows; a short-radius turn fits tighter layouts but can add resistance. A tee’s branch may need extra attention because flow leaves the main line at an angle. Crosses can simplify compact layouts, yet four-way junctions may complicate balancing and inspection.
Details matter. ASME B16.9 covers factory-made wrought butt-welding fittings from NPS 1/2 through NPS 48, including dimensional requirements. In practice, matching the fitting schedule and material to the pipe is essential. I would still verify the layout against actual operating conditions: drawings can make a crowded junction look simpler than it is.
Reducers connect pipes of different diameters while keeping the transition controlled.
A concentric reducer narrows evenly around the centerline, while an eccentric reducer keeps one side flat. That flat edge can help limit trapped air or liquid in some horizontal lines, but orientation depends on the system. Check the drawings before installation.
Fit matters. Match the reducer’s material, wall thickness, and connection type to the adjoining pipe. A small mismatch can complicate welding or create an uneven internal step.
Caps close an open pipe end; couplings join two pipe sections. Both must suit the line’s pressure, temperature, and service conditions.
A cap may look simple, yet its rating and joining method matter just as much as the pipe’s. Couplings are commonly used for straight connections, but available designs vary in length and assembly method.
Small details count. Before fitting, inspect threads, bevels, and sealing surfaces for damage or debris. I have seen a clean-looking connection cause trouble when the parts were not checked together.
Even careful planning can miss a site-specific constraint, so confirm dimensions and installation requirements against the approved piping documents.
Butt-weld fittings join pipe ends through a welded connection, creating a smooth internal passage when properly aligned. ASME B16.9 covers factory-made wrought fittings from NPS ½ through NPS 48. That range is a useful specification, not a promise that every fitting suits every service. NPS is a nominal size; it does not state the pipe’s exact outside diameter. The standard sets key dimensions and tolerances for components such as elbows, tees, reducers, and caps.
On a shop floor, a 90-degree elbow may look interchangeable with another of the same NPS. Its wall thickness, material, schedule, and radius still need checking against the piping design. ASME B16.9 provides the fitting dimensions; the applicable piping code, such as ASME B31.3, informs system design requirements. Pressure suitability depends on the full design, not the size range alone. Small mismatch, big headache. I would verify markings and dimensions before welding, even when paperwork looks complete.
Tips: Match the fitting’s NPS, schedule, material, and end preparation to the pipe. Check the drawing and governing code, then inspect bevels and alignment before welding. A quick check can prevent a costly fit-up correction.
Forged fittings connect small-bore pipe runs where compact, robust joints matter. ASME B16.11 specifies threaded fittings in Classes 2,000, 3,000, and 6,000, and socket-weld fittings in Classes 3,000, 6,000, and 9,000. These class numbers are not direct pressure ratings in psi. Allowable pressure depends on material, temperature, and the applicable piping code. A label alone is not enough.
The standard covers dimensions, tolerances, and marking for forged socket-welding and threaded fittings (ASME B16.11-2021). Threaded fittings can simplify assembly where welding is impractical, but thread sealing and inspection need care. Socket-weld fittings use a fillet weld around the pipe end; fit-up and weld quality affect reliability. In field work, even a small gap or misalignment can complicate inspection. Worth checking twice.
Tip: Confirm the fitting class, material grade, pipe schedule, and service temperature against the project specification. Do not choose a class by number alone. Keep traceable material records, and verify that the selected fitting and joining method suit the actual operating conditions.
| Fitting Type | Common Configurations | Connection Style | ASME B16.11 Class Designations | Typical Function |
|---|---|---|---|---|
| Elbow | 45° and 90° changes in direction | Threaded or socket-weld | Threaded: 2,000, 3,000, 6,000; socket-weld: 3,000, 6,000, 9,000 | Redirects flow through a piping system. |
| Tee | Equal and reducing branches | Threaded or socket-weld | Threaded: 2,000, 3,000, 6,000; socket-weld: 3,000, 6,000, 9,000 | Connects a branch line to a run. |
| Cross | Four-way intersecting connections | Threaded or socket-weld | Threaded: 2,000, 3,000, 6,000; socket-weld: 3,000, 6,000, 9,000 | Joins four pipe paths at an intersection. |
| Coupling | Full coupling; equal or reducing designs where specified | Threaded or socket-weld | Threaded: 2,000, 3,000, 6,000; socket-weld: 3,000, 6,000, 9,000 | Joins two pipe ends in line. |
| Half coupling | Single-end connection for a branch or outlet | Threaded or socket-weld, as specified | Class availability depends on fitting type and connection style | Provides a compact connection from a pipe or fitting. |
| Cap | End closure | Threaded or socket-weld | Class availability depends on fitting type and connection style | Closes the end of a pipe or fitting. |
| Plug | Male-threaded closure | Threaded | Threaded class designation depends on the fitting specification | Closes a female-threaded opening. |
| Bushing | Reducing threaded connection | Threaded | Threaded class designation depends on the fitting specification | Connects different nominal pipe sizes at a threaded opening. |
| Union | Three-piece detachable connection | Threaded | Threaded class designation depends on the fitting specification | Allows a piping section to be disconnected for maintenance. |
Note: ASME B16.11 class designations identify fitting classes, not a universal pressure rating in psi. Allowable pressure depends on factors such as material, temperature, connection type, and the applicable piping code. Confirm the standard edition and fitting-specific requirements for the intended service.
| Cookie | Duration | Description |
|---|---|---|
| AWSALB | 7 days | AWSALB is a cookie generated by the Application load balancer in the Amazon Web Services. It works slightly different from AWSELB. |
| AWSALBCORS | 7 days | This cookie is used for load balancing services provded by Amazon inorder to optimize the user experience. Amazon has updated the ALB and CLB so that customers can continue to use the CORS request with stickness. |
| cookielawinfo-checkbox-advertisement | 1 year | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Advertisement". |
| cookielawinfo-checkbox-analytics | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytic / Performance". |
| cookielawinfo-checkbox-functional | 11 months | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional". |
| cookielawinfo-checkbox-necessary | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Strictly Necessary". |
| cookielawinfo-checkbox-performance | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance". |
| cookielawinfo-checkbox-preferences | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Preferences." |
| elementor | never | This cookie is used by the website's WordPress theme. It allows the website owner to implement or change the website's content in real-time. |
| viewed_cookie_policy | 11 months | The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data. |
| Cookie | Duration | Description |
|---|---|---|
| CONSENT | 16 years 4 months | These cookies are set via embedded youtube-videos. They register anonymous statistical data on for example how many times the video is displayed and what settings are used for playback.No sensitive data is collected unless you log in to your google account, in that case your choices are linked with your account, for example if you click “like” on a video. |
| _ga | 2 years | This cookie is installed by Google Analytics. The cookie is used to calculate visitor, session, campaign data and keep track of site usage for the site's analytics report. The cookies store information anonymously and assign a randomly generated number to identify unique visitors. |
| _gat_gtag_UA_47200144_1 | 1 minute | This cookie is set by Google and is used to distinguish users. |
| _gid | 1 day | This cookie is installed by Google Analytics. The cookie is used to store information of how visitors use a website and helps in creating an analytics report of how the website is doing. The data collected including the number visitors, the source where they have come from, and the pages visted in an anonymous form. |
| _hjAbsoluteSessionInProgress | session | This cookie is used to count how many times a website has been visited by different visitors. This is done by assigning the visitor an ID, so the visitor does not get registered twice. |
| _hjFirstSeen | 30 minutes | This is set by Hotjar to identify a new user’s first session. It stores a true/false value, indicating whether this was the first time Hotjar saw this user. It is used by Recording filters to identify new user sessions. |
| _hjid | 1 year | This cookie is set by Hotjar. This cookie is set when the customer first lands on a page with the Hotjar script. It is used to persist the random user ID, unique to that site on the browser. This ensures that behavior in subsequent visits to the same site will be attributed to the same user ID. |
| _hjIncludedInPageviewSample | session | This cookie is used to detect whether the user navigation and interactions are included in the website’s data analytics. |
| Cookie | Duration | Description |
|---|---|---|
| IDE | 1 year 24 days | This cookie is used by Google DoubleClick and stores information about how the user uses the website and any other advertisement before visiting the website. This is used to present users with ads that are relevant to them according to the user profile. |
| NID | 6 months | This cookie is used to a profile based on user's interest and display personalized ads to the users. |
| test_cookie | 15 minutes | This cookie is set by doubleclick.net. The purpose of the cookie is to determine if the user's browser supports cookies. |
| VISITOR_INFO1_LIVE | 5 months 27 days | This cookie is set by Youtube it is used to track the information of the embedded YouTube videos on a website. |
| YSC | session | This cookies is set by Youtube and is used to track the views of embedded videos. |
| yt-remote-connected-devices | never | These cookies are set via embedded youtube-videos. |
| yt-remote-device-id | never | These cookies are set via embedded youtube-videos. |
| Cookie | Duration | Description |
|---|---|---|
| qtrans_front_language | 1 year | This cookie is set by qTranslate WordPress plugin. The cookie is used to manage the preferred language of the visitor. |