Automotive Stamping Tooling is where vehicle design meets repeatable production. A die must shape sheet metal accurately, withstand thousands of press cycles, and remain practical to maintain. Small details matter: a draw radius, a springback adjustment, or a worn cutting edge can affect part fit and production flow. The suppliers in this overview are assessed through capabilities such as die design, engineering support, manufacturing scale, and global service—not a single universal ranking.
The market context is changing. OICA reported 93.5 million motor vehicles produced worldwide in 2023, underscoring the scale that stamping operations must serve. The International Energy Agency’s Global EV Outlook 2024 estimated nearly 14 million electric-car sales in 2023, about 18% of global car sales. Electrification can shift body structures and material choices, increasing demands on tooling development. Yet the transition is uneven. Not every plant faces the same requirements.
A useful technical lens comes from Professor Peter Groche, a sheet-metal-forming researcher: “Reliable forming depends on controlling material flow, tool geometry, and process variation.” This is a paraphrase of the engineering principles associated with his research, not a verbatim quotation. It highlights a practical test for suppliers: can they turn complex part designs into stable, repeatable production? The answer depends on the application, plant, and support model. That nuance is easy to miss in a top-ten list.
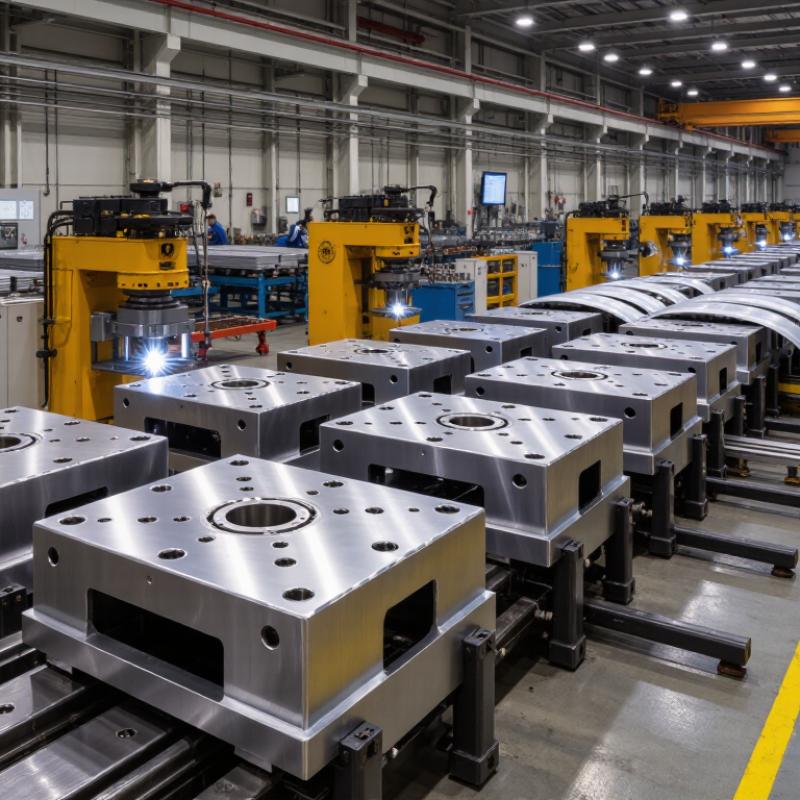
Automotive stamping tooling suppliers design and build the dies that shape sheet metal into vehicle components. Their work can include engineering, die machining, tryout, press-line integration, and tool maintenance. A supplier may deliver a single production die or manage a complete tooling package. It is not automatically a stamping-parts producer or a press manufacturer. The boundary can blur when firms offer several services.
Demand is tied to vehicle production, but production figures do not measure tooling sales. The International Organization of Motor Vehicle Manufacturers reported 93.5 million vehicles produced worldwide in 2023, up from 85.0 million in 2022. The International Energy Agency’s Global EV Outlook 2024 estimated nearly 14 million electric-car sales in 2023, about 18% of global car sales. These figures help explain why supplier assessments should consider production capacity and experience with changing body structures. They do not prove a supplier’s market share. A fair comparison also checks tool size, material capability, delivery record, and support near customer plants. Rankings can still be imperfect; public data rarely separates tooling revenue from wider manufacturing services.
Global vehicle production reached 93.5 million units in 2023, according to OICA. That figure offers stamping-tooling suppliers a clear view of the industry’s scale, but it is not a direct measure of tooling orders. The number is impressive. Still, it can mislead. Vehicle mix, regional output, and model changeovers all affect the type and timing of tooling demand. A plant producing compact cars may need different die designs and press capacity than one building larger vehicles.
Stamping tools form body panels and structural components through repeated, controlled press operations. At this production scale, reliable tool performance matters: small alignment issues can create visible panel defects or disrupt production schedules. Suppliers must consider material behavior, die maintenance, dimensional accuracy, and the time needed to validate a tool. Production totals alone cannot show these details. They do, however, help explain why manufacturers value suppliers that can support consistent output across changing programs.
Tips: Treat the 93.5 million figure as context, not a forecast. Compare it with regional production plans, vehicle types, and launch schedules. Ask how a supplier manages tool trials, wear checks, and design changes. One detail is easy to overlook: a schedule that works on paper may still leave too little time for adjustments.
When comparing automotive stamping tooling suppliers, IATF 16949 is a useful starting point, not a performance guarantee. Check that certification covers the actual manufacturing site and relevant processes. Ask how corrective actions, process changes, and inspection records are managed. That matters.
Press capacity should match the part, material, and production rate. Compare tonnage with bed size, stroke, shut height, and feeder limits. Ask suppliers to demonstrate the proposed setup using a representative coil or blank. A press may have ample force but insufficient space for a complex die. Numbers alone can mislead.
Die life is harder to compare than press specifications. Request documented hit counts, maintenance intervals, repair history, and the conditions behind those figures. A die running thicker high-strength steel may wear differently from one stamping mild steel. Review how the supplier tracks edge wear, cracking, and dimensional drift during production. Also examine spare-insert availability and response times for repairs. These details affect downtime as much as the quoted lifespan. Records are not always perfectly comparable, so treat unusually high life claims cautiously and ask for context.
A comparison of the top automotive stamping tooling suppliers should look beyond plant locations. Global reach matters when engineering teams, die-build shops, and service crews can work across regions. A local technician can check a worn draw surface without waiting for distant support. That can reduce downtime, though it does not guarantee a fast repair.
Tooling scope also separates suppliers. Some build progressive dies for high-volume parts; others focus on transfer or tandem dies for larger panels. Useful evidence includes press-size capability, simulation methods, tryout capacity, and documented checks for springback and surface finish. Ask how design changes move from engineering to the shop floor. Details matter.
Customer base offers another practical signal. Suppliers serving both vehicle manufacturers and component makers may understand different launch pressures, production volumes, and quality requirements. Still, a long customer list says little about the team assigned to a specific project. Review comparable parts, regional spare-parts access, and the handoff between design and production. Footprint charts can look impressive; actual support is less tidy. A supplier with fewer sites may respond better in one region, while a large network may offer broader backup. Compare the work, not just the map.
A view of common tooling categories across the supplier landscape—not a company ranking.
Progressive, transfer, tandem, blanking and piercing, draw and form, and restrike and calibration dies are established categories of automotive stamping tooling. Each bar marks one category; bar lengths do not represent supplier counts, market share, or capability ratings. Supplier footprints and customer bases vary, and comparable data is not consistently disclosed.
For automotive stamping tooling suppliers, expertise in AHSS forming shows in the first tryout, not just in a polished simulation. The IEA’s Global EV Outlook 2024 reports nearly 14 million electric-car sales in 2023, about 18% of global car sales. As vehicle structures evolve, dies must form stronger grades while holding tight dimensions around bends, holes, and mating flanges. WorldAutoSteel’s AHSS Application Guidelines explain why grade-specific forming behavior and springback compensation matter. Small errors matter.
Dimensional control should be demonstrated with measured parts. A capable team checks die-face geometry, monitors binder pressure, and compares stamped panels against CAD using scanning or coordinate measurement. It then links deviations to practical adjustments, such as draw-bead changes or revised compensation. The evidence should include repeat runs, not one attractive sample. A clean simulation is not proof; even experienced teams can underestimate how material variation shifts a flange after unloading.
Tips: Ask suppliers how they validate springback across material batches, and request inspection results from a full-size panel. Check whether their reports identify measurement method, tolerance, and correction history. Don’t accept “within spec” without the numbers. One overlooked datum can mislead an entire build.
Evaluation framework: The rows below are ten supplier-selection criteria, not a ranked list of named companies. They focus on verifiable capabilities; actual performance and acceptance limits should be confirmed for each part, material, and program.
| No. | Evaluation area | Why it matters for AHSS tooling | Evidence to request | How to compare suppliers |
|---|---|---|---|---|
| 1 | AHSS material and grade experience | Advanced high-strength steels vary in strength, ductility, and forming behavior. Tooling designed for one grade or thickness may not transfer directly to another. | Completed part examples showing steel grade, thickness, forming process, and production outcome; material specifications should identify the applicable grade and standard. | Compare experience with the specific grades and thicknesses in the part specification. Do not treat experience with one AHSS grade as proof of capability with all grades. |
| 2 | Formability analysis and simulation | Forming simulation can help identify risks such as thinning, wrinkling, and potential splits before production tooling is finalized. | Simulation reports showing input material data, boundary conditions, predicted risk areas, and correlation with tryout or production results. | Assess whether the supplier validates predictions against physical trials and documents changes made when simulation and measured results differ. |
| 3 | Springback prediction and compensation | Elastic recovery after forming can affect shape and fit, especially in high-strength materials. Compensation is part- and process-specific. | Before-and-after geometry data, compensation records, and measurement results from representative formed parts. | Compare demonstrated dimensional improvement across iterations, using the same measurement method and agreed drawing requirements. |
| 4 | Die design and process engineering | Draw, trim, restrike, and other operations must work together to achieve the required geometry and stable production. | Process plan, operation sequence, die design reviews, and documented checks for material flow, access, and part handling. | Review the supplier’s reasoning for the chosen operation sequence and how design risks are resolved before die build. |
| 5 | Dimensional measurement capability | Consistent inspection is necessary to determine whether a part meets its drawing and to diagnose dimensional variation. | Inspection plans, calibrated equipment records, coordinate-measuring-machine or scanning reports, and measurement-system studies where applicable. | Confirm that the measurement method, datum scheme, and reporting format match the customer’s requirements. There is no single universal tolerance for all stamped parts. |
| 6 | Tryout and dimensional correction | Physical tryout reveals real process effects that may not be fully captured in design or simulation. | Tryout schedules, issue logs, corrective-action records, and inspection results from successive tool iterations. | Compare the clarity of root-cause analysis, response to measured deviations, and evidence that corrections were verified. |
| 7 | Tool materials, wear, and maintenance planning | Tool material and surface choices influence wear behavior and maintenance needs; suitability depends on material, volume, and process conditions. | Tool-material specifications, wear-risk assessment, maintenance instructions, and any relevant production or tool-life records. | Evaluate whether recommendations are supported by comparable applications and include practical inspection and maintenance intervals. |
| 8 | Press and production-process compatibility | Press capacity, shut height, bed dimensions, feed, and handling arrangements constrain how a die can be run. | Press requirements, die-interface drawings, tonnage or load assessments, and documented production-line checks. | Check compatibility against the actual production press and line layout rather than relying on general equipment capability claims. |
| 9 | Quality-system and change control | Controlled documentation helps keep tooling revisions, inspection methods, and production requirements aligned. | Current quality-system certificates where required, revision histories, nonconformance records, and formal engineering-change procedures. | Verify certificate scope and validity directly, and assess how changes are reviewed, approved, and communicated through the program. |
| 10 | Program delivery and technical support | Tooling programs depend on coordinated design, build, tryout, and launch activities, including timely resolution of technical issues. | Milestone plans, staffing and escalation arrangements, issue-response records, and references for comparable program scope. | Compare documented delivery performance and support arrangements against the program schedule, location, and launch requirements. |
| Cookie | Duration | Description |
|---|---|---|
| AWSALB | 7 days | AWSALB is a cookie generated by the Application load balancer in the Amazon Web Services. It works slightly different from AWSELB. |
| AWSALBCORS | 7 days | This cookie is used for load balancing services provded by Amazon inorder to optimize the user experience. Amazon has updated the ALB and CLB so that customers can continue to use the CORS request with stickness. |
| cookielawinfo-checkbox-advertisement | 1 year | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Advertisement". |
| cookielawinfo-checkbox-analytics | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytic / Performance". |
| cookielawinfo-checkbox-functional | 11 months | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional". |
| cookielawinfo-checkbox-necessary | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Strictly Necessary". |
| cookielawinfo-checkbox-performance | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance". |
| cookielawinfo-checkbox-preferences | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Preferences." |
| elementor | never | This cookie is used by the website's WordPress theme. It allows the website owner to implement or change the website's content in real-time. |
| viewed_cookie_policy | 11 months | The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data. |
| Cookie | Duration | Description |
|---|---|---|
| CONSENT | 16 years 4 months | These cookies are set via embedded youtube-videos. They register anonymous statistical data on for example how many times the video is displayed and what settings are used for playback.No sensitive data is collected unless you log in to your google account, in that case your choices are linked with your account, for example if you click “like” on a video. |
| _ga | 2 years | This cookie is installed by Google Analytics. The cookie is used to calculate visitor, session, campaign data and keep track of site usage for the site's analytics report. The cookies store information anonymously and assign a randomly generated number to identify unique visitors. |
| _gat_gtag_UA_47200144_1 | 1 minute | This cookie is set by Google and is used to distinguish users. |
| _gid | 1 day | This cookie is installed by Google Analytics. The cookie is used to store information of how visitors use a website and helps in creating an analytics report of how the website is doing. The data collected including the number visitors, the source where they have come from, and the pages visted in an anonymous form. |
| _hjAbsoluteSessionInProgress | session | This cookie is used to count how many times a website has been visited by different visitors. This is done by assigning the visitor an ID, so the visitor does not get registered twice. |
| _hjFirstSeen | 30 minutes | This is set by Hotjar to identify a new user’s first session. It stores a true/false value, indicating whether this was the first time Hotjar saw this user. It is used by Recording filters to identify new user sessions. |
| _hjid | 1 year | This cookie is set by Hotjar. This cookie is set when the customer first lands on a page with the Hotjar script. It is used to persist the random user ID, unique to that site on the browser. This ensures that behavior in subsequent visits to the same site will be attributed to the same user ID. |
| _hjIncludedInPageviewSample | session | This cookie is used to detect whether the user navigation and interactions are included in the website’s data analytics. |
| Cookie | Duration | Description |
|---|---|---|
| IDE | 1 year 24 days | This cookie is used by Google DoubleClick and stores information about how the user uses the website and any other advertisement before visiting the website. This is used to present users with ads that are relevant to them according to the user profile. |
| NID | 6 months | This cookie is used to a profile based on user's interest and display personalized ads to the users. |
| test_cookie | 15 minutes | This cookie is set by doubleclick.net. The purpose of the cookie is to determine if the user's browser supports cookies. |
| VISITOR_INFO1_LIVE | 5 months 27 days | This cookie is set by Youtube it is used to track the information of the embedded YouTube videos on a website. |
| YSC | session | This cookies is set by Youtube and is used to track the views of embedded videos. |
| yt-remote-connected-devices | never | These cookies are set via embedded youtube-videos. |
| yt-remote-device-id | never | These cookies are set via embedded youtube-videos. |
| Cookie | Duration | Description |
|---|---|---|
| qtrans_front_language | 1 year | This cookie is set by qTranslate WordPress plugin. The cookie is used to manage the preferred language of the visitor. |