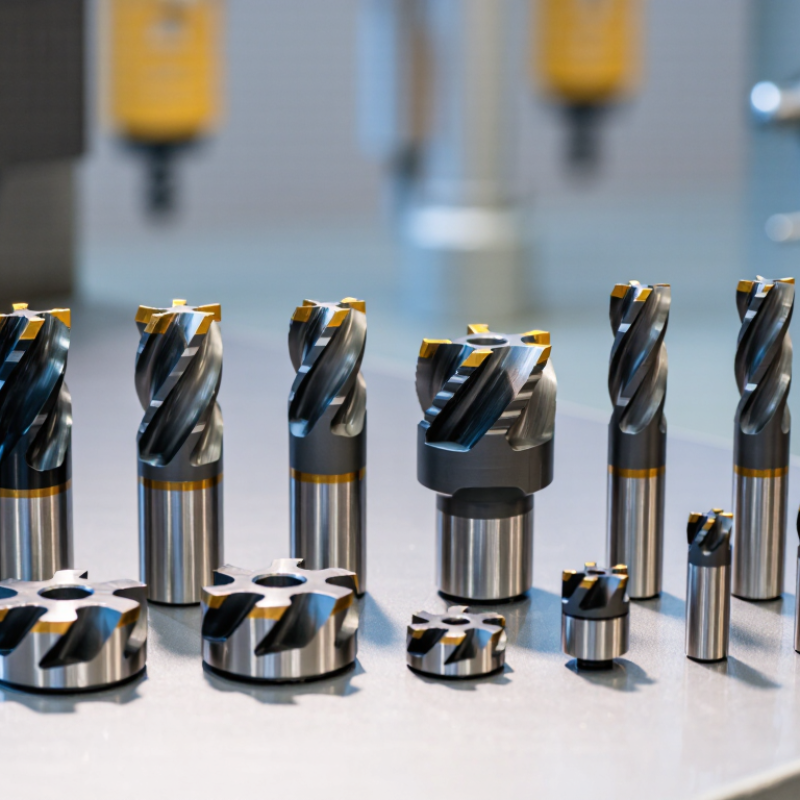
Choosing a Chamfering Cutter is not simply a matter of selecting the sharpest tool. Buyers must match cutter geometry, material, angle, diameter, coating, and machine capability. A 45-degree cutter may suit a general deburring task, while a carbide indexable cutter may perform better on repeated production runs. Small details matter. A poor choice can leave burrs, chatter marks, or an uneven edge.
Dr. Tony L. Schmitz, a respected machining dynamics researcher, offers a valuable principle: “The tool, workpiece, and process must be considered as one dynamic system.” This idea guides the comparison behind the Top 10 Types of Chamfering Cutters for Buyers. Each type has a practical role, from countersink cutters and adjustable chamfer mills to solid carbide and insert-based designs. Their performance changes with steel hardness, aluminum’s tendency to build up, spindle speed, coolant use, and workholding stability.
No list is perfect. Some cutter categories overlap, and supplier descriptions are not always consistent. Buyers should still verify dimensions, included angles, cutting-edge quality, and replacement-part availability. Look closely at the finished edge under bright light. It should appear clean, continuous, and free from tearing. A trial cut on the actual material remains more reliable than a catalog promise. This guide therefore focuses on useful differences, common limitations, and purchasing details that can prevent expensive mistakes. Good tooling saves time. Better judgment saves more.
Top 10 Types of Chamfering Cutters for Buyers?
Chamfering cutters remove sharp edges, prepare weld joints, and guide fasteners into holes. The 45° cutter is the general-purpose choice. It creates a balanced edge break and usually needs less cutting force than steeper profiles. A 90° cutter produces a wider, flatter recess for countersunk screw heads. It demands better spindle rigidity and careful feed control. Small errors become visible rings.
The ten common families include solid-carbide, high-speed-steel, indexable, single-flute, multi-flute, countersink, back-chamfer, deburring, adjustable, and form cutters. Buyers should match the angle with material hardness, hole diameter, coating, and machine stability. ISO 13715 provides guidance for defining undefined edges, but it does not replace a production trial. That distinction matters.
Grand View Research estimated the global cutting-tools market at about USD 23 billion in 2023, with growth continuing through 2030. This expansion reflects wider machining demand, but market size cannot identify the correct cutter. U.S. Cutting Tool Institute and AMT monthly reports also track cutting-tool shipments by value, showing why purchasing teams should compare tool life, not only unit price. In practice, a 45° tool may last longer on aluminum, while a 90° tool may improve seating accuracy in steel. I have seen drawings specify an angle without stating edge width. That is a costly omission. Test one cutter, inspect the burr, and measure the finished chamfer before ordering hundreds.
| No. | Chamfering Cutter Type | Common Included Angle | Typical Cutting Edge | Suitable Materials | Typical Industrial Uses | Key Advantages | Buyer Considerations |
|---|---|---|---|---|---|---|---|
| 1 | Single-Flute Chamfer Mill | 90° | One cutting edge | Aluminum Plastics Soft steel | Edge breaking, deburring, countersinking, and light chamfering on CNC machines. | Good chip clearance and reduced cutting force; useful for softer materials. | Choose a rigid tool holder and suitable feed rate; less productive than multi-flute tools in some operations. |
| 2 | Two-Flute Chamfer Mill | 90° | Two cutting edges | Aluminum Steel Brass | General-purpose chamfering, countersinking, and profiling. | Balanced option between productivity, chip space, and surface finish. | Confirm flute geometry and coating compatibility with the workpiece material. |
| 3 | Multi-Flute Chamfer Mill | 45° or 90° | Three or more cutting edges | Steel Stainless steel Non-ferrous alloys | High-volume edge finishing and consistent chamfer production. | Higher potential feed rate and efficient material removal when machine rigidity is adequate. | Smaller chip gullets require proper chip evacuation and stable machining conditions. |
| 4 | Indexable Chamfer Cutter | 45°, 60°, or 90° | Replaceable carbide inserts | Cast iron Steel Stainless steel | Production chamfering, heavy-duty edge preparation, and large workpieces. | Insert replacement can restore cutting performance without replacing the cutter body. | Check insert availability, screw security, runout, and the required chamfer width. |
| 5 | Solid Carbide Chamfer Mill | 45° or 90° | Integrated carbide cutting edges | Hardened steel Tool steel Titanium alloys | Precision CNC machining, small components, and hard or abrasive materials. | High rigidity, good wear resistance, and accurate edge geometry. | Higher purchase cost; avoid excessive tool deflection and use appropriate coolant practices. |
| 6 | High-Speed Steel Chamfer Cutter | 45° or 90° | HSS cutting edges | Mild steel Brass Aluminum | Manual milling, maintenance work, low-to-medium production, and general workshop use. | Lower cost and greater toughness than carbide in interrupted or less rigid setups. | Use lower cutting speeds than carbide; edge life may be shorter in abrasive materials. |
| 7 | Micro Chamfer Cutter | 45° or 90° | Small-diameter precision edge | Tool steel Aluminum Engineering plastics | Medical components, electronics parts, miniature molds, and fine mechanical components. | Designed for very small chamfers and detailed edge control. | Requires low runout, high spindle accuracy, and careful tool handling to prevent breakage. |
| 8 | Back Chamfer Cutter | 45° or 60° | Offset or undercutting edge | Steel Aluminum Non-ferrous metals | Chamfering the rear side of holes, slots, and features that are difficult to access from the front. | Performs front and back edge preparation with reduced workpiece repositioning. | Verify clearance, tool reach, machine travel, and the required pilot or neck diameter. |
| 9 | Adjustable Chamfer Cutter | Usually 45° or 90° | Adjustable blade or insert position | Steel Aluminum Cast iron | Variable chamfer widths, repair work, and applications with changing edge requirements. | One cutter can cover a range of chamfer dimensions when correctly set. | Setup accuracy is critical; inspect locking mechanisms and verify repeatability before production. |
| 10 | Combination Chamfer and Countersink Cutter | Typically 90° | Chamfering and countersinking geometry | Steel Aluminum Brass | Preparing holes for flat-head fasteners while also removing sharp edges. | Combines two operations and can reduce tool changes in repetitive work. | Match the included angle and cutting diameter to the fastener head and hole specification. |
Top 10 Types of Chamfering Cutters for Buyers
A ten-type list is useful, but not perfect. Cutting conditions can change the best choice. Geometry remains the first buying decision. Single-angle cutters suit standard edge breaks. Double-angle cutters create two controlled faces. Multi-angle cutters handle complex profiles. Radius cutters soften edges and reduce stress concentration. Back-chamfer cutters work inside holes and narrow channels. Countersink cutters prepare screw seats. Deburring cutters remove burrs after drilling or milling. These shapes match different cutting applications.
Flute design affects chip evacuation, rigidity, and surface quality. Two-flute cutters leave more space for chips in soft aluminum. Three-flute designs balance productivity and stability. Four-flute cutters can improve finish on rigid machines. Variable-flute options may reduce vibration, although results depend on setup. Solid carbide cutters offer high stiffness for hardened materials. High-speed steel cutters remain practical for lower speeds and frequent resharpening. Indexable cutters can reduce replacement costs during heavy production.
Industry reports show why selection deserves attention. Grand View Research valued the global cutting tools market at about USD 24.6 billion in 2023, with continued growth projected through 2030. Mordor Intelligence also identifies automation and precision machining as major market drivers. However, market growth does not guarantee a correct cutter choice. A harder tool may fail in a weak spindle. More flutes may trap chips. Check material, chamfer width, machine power, coolant, and workholding before purchasing. Small trials often expose assumptions that catalog charts miss.
Comparison by typical included angle, flute configuration, and cutting application
The chart compares common cutter configurations using their typical included angles. Single-angle and countersink tools are commonly available with two to six flutes, while back-chamfer tools often use two to four flutes and indexable designs use replaceable inserts. Select the geometry according to the required edge break, countersink standard, material, access direction, and desired surface finish.
Choosing a chamfering cutter starts with the workpiece, not the catalog photograph.
HSS cutters are tough, economical, and easier to resharpen. They suit mild steel, aluminum, plastics, and interrupted cuts at moderate speeds. Their edge can tolerate vibration better than carbide. Still, HSS loses hardness quickly when heat builds near the cutting edge.
Carbide cutters support higher cutting speeds and maintain a sharper edge on stainless steel, cast iron, and hardened alloys. They resist wear well, but they are less forgiving. A small runout error or sudden impact can chip the tip.
In practical testing, rigid toolholding and accurate setup matter as much as cutter grade. We sometimes blame the material when the real problem is poor alignment.
TiAlN coatings add another layer of protection. Depending on composition and testing method, hardness can reach about 3,500 HV. The coating helps reduce flank wear and withstand elevated cutting temperatures. It works best on a suitable carbide substrate with controlled feeds and adequate chip evacuation.
Coating alone cannot rescue a weak edge. Dry cutting may be useful for selected steels, but not every machine or workpiece responds well. Check the manufacturer’s cutting data, then verify it with a short trial cut. A slightly lower speed often produces a cleaner chamfer and longer tool life.
For buyers comparing chamfering cutters, sizing begins with the shank diameter. It must match the holder, not merely enter it. ISO 286-2:2010 defines tolerance classes for fits and holes. For an 8 mm pilot bore, an H7 tolerance allows roughly 0.015 mm variation. That small allowance matters. A loose pilot can create chatter, uneven chamfer width, and premature edge wear.
Pilot size should follow the finished hole, cutter geometry, and material condition. Do not assume a larger pilot improves stability. A pilot 0.03 mm undersize may guide poorly, while an oversize pilot can bind after thermal expansion. In shop inspections, measure the pilot with a calibrated micrometer and check the actual bore separately. NIST Technical Note 1297 stresses repeatability, calibration, and measurement uncertainty. The test is simple. The judgment is not.
Shank diameter also affects stiffness and holder balance. ISO 1940-1:2015 links rotating-tool balance quality with permissible unbalance, but it does not replace runout verification. A 0.02 mm total indicated runout target should be checked near the cutting edge, not only at the shank. Use a clean holder, consistent gauge pressure, and at least two angular positions. Realistically, 0.02 mm may be difficult on worn equipment. That is worth recording, not hiding.
For buyers comparing the top 10 types of chamfering cutters, geometry is only the starting point. Common options include single-angle, double-angle, back-chamfer, countersink, deburring, indexable, solid-carbide, modular, adjustable, and form cutters. Each suits a different edge condition. Solid carbide can hold a crisp edge in hardened steel, but it may chip during interrupted cuts. Indexable designs reduce replacement cost, yet inserts add runout and setup variables. In practice, “longer life” is meaningless without fixed workpiece, coolant, and wear limits.
Feed rate should be tested with tool diameter, included angle, material, and spindle power recorded. ISO 3685:1993 provides a framework for tool-life testing, while ISO 13399 standardizes digital cutting-tool data. ISO 13399 does not guarantee cutting performance. That distinction is often missed. Use supplier starting values, then run short trials at three feed levels. Record edge wear after every batch. A 10% feed increase may improve throughput, but excessive rubbing can shorten life sharply. Taylor-style tool-life calculations help compare trends, not predict every corner.
Tips: Request ISO 13399 fields before importing tools into CAM software. Check cutting diameter, usable length, corner radius, and handedness. Calculate cost per finished edge, not cost per cutter. Include regrinding, scrap, changeover minutes, and inspection time. Keep a simple spreadsheet. It exposes weak assumptions. Test one less aggressive setting, too. The fastest cycle is not always the cheapest.
| Cookie | Duration | Description |
|---|---|---|
| AWSALB | 7 days | AWSALB is a cookie generated by the Application load balancer in the Amazon Web Services. It works slightly different from AWSELB. |
| AWSALBCORS | 7 days | This cookie is used for load balancing services provded by Amazon inorder to optimize the user experience. Amazon has updated the ALB and CLB so that customers can continue to use the CORS request with stickness. |
| cookielawinfo-checkbox-advertisement | 1 year | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Advertisement". |
| cookielawinfo-checkbox-analytics | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytic / Performance". |
| cookielawinfo-checkbox-functional | 11 months | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional". |
| cookielawinfo-checkbox-necessary | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Strictly Necessary". |
| cookielawinfo-checkbox-performance | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance". |
| cookielawinfo-checkbox-preferences | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Preferences." |
| elementor | never | This cookie is used by the website's WordPress theme. It allows the website owner to implement or change the website's content in real-time. |
| viewed_cookie_policy | 11 months | The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data. |
| Cookie | Duration | Description |
|---|---|---|
| CONSENT | 16 years 4 months | These cookies are set via embedded youtube-videos. They register anonymous statistical data on for example how many times the video is displayed and what settings are used for playback.No sensitive data is collected unless you log in to your google account, in that case your choices are linked with your account, for example if you click “like” on a video. |
| _ga | 2 years | This cookie is installed by Google Analytics. The cookie is used to calculate visitor, session, campaign data and keep track of site usage for the site's analytics report. The cookies store information anonymously and assign a randomly generated number to identify unique visitors. |
| _gat_gtag_UA_47200144_1 | 1 minute | This cookie is set by Google and is used to distinguish users. |
| _gid | 1 day | This cookie is installed by Google Analytics. The cookie is used to store information of how visitors use a website and helps in creating an analytics report of how the website is doing. The data collected including the number visitors, the source where they have come from, and the pages visted in an anonymous form. |
| _hjAbsoluteSessionInProgress | session | This cookie is used to count how many times a website has been visited by different visitors. This is done by assigning the visitor an ID, so the visitor does not get registered twice. |
| _hjFirstSeen | 30 minutes | This is set by Hotjar to identify a new user’s first session. It stores a true/false value, indicating whether this was the first time Hotjar saw this user. It is used by Recording filters to identify new user sessions. |
| _hjid | 1 year | This cookie is set by Hotjar. This cookie is set when the customer first lands on a page with the Hotjar script. It is used to persist the random user ID, unique to that site on the browser. This ensures that behavior in subsequent visits to the same site will be attributed to the same user ID. |
| _hjIncludedInPageviewSample | session | This cookie is used to detect whether the user navigation and interactions are included in the website’s data analytics. |
| Cookie | Duration | Description |
|---|---|---|
| IDE | 1 year 24 days | This cookie is used by Google DoubleClick and stores information about how the user uses the website and any other advertisement before visiting the website. This is used to present users with ads that are relevant to them according to the user profile. |
| NID | 6 months | This cookie is used to a profile based on user's interest and display personalized ads to the users. |
| test_cookie | 15 minutes | This cookie is set by doubleclick.net. The purpose of the cookie is to determine if the user's browser supports cookies. |
| VISITOR_INFO1_LIVE | 5 months 27 days | This cookie is set by Youtube it is used to track the information of the embedded YouTube videos on a website. |
| YSC | session | This cookies is set by Youtube and is used to track the views of embedded videos. |
| yt-remote-connected-devices | never | These cookies are set via embedded youtube-videos. |
| yt-remote-device-id | never | These cookies are set via embedded youtube-videos. |
| Cookie | Duration | Description |
|---|---|---|
| qtrans_front_language | 1 year | This cookie is set by qTranslate WordPress plugin. The cookie is used to manage the preferred language of the visitor. |