What Are the Top 10 Pipe Swaging Machines?
Choosing among the top 10 Pipe Swaging Machines requires more than comparing purchase prices. A reliable Pipe Swaging Machine must form tubes consistently, protect surface quality, and maintain stable dimensions across repeated production cycles. The International Federation of Robotics’ World Robotics 2024 report highlights continuing industrial automation growth, making programmable controls and production monitoring increasingly important. Yet automation alone does not guarantee better results.
This guide evaluates ten machines through practical manufacturing criteria. These include forming force, compatible tube diameters, material range, tooling changeover time, stroke control, dimensional repeatability, operator safety, and after-sales support. Energy consumption also matters. The U.S. Department of Energy’s Better Plants resources encourage manufacturers to measure equipment efficiency, not merely output speed. A machine that completes one cycle faster may still cost more when compressed air, electricity, tooling, and maintenance are included.
Real workshop conditions can be unforgiving. A stainless-steel tube may show marking after one poorly aligned stroke. A small die error can create an oval end, causing leakage during assembly. ISO 12100 provides a useful framework for machinery risk assessment, while ISO 9001 principles support traceable quality control. However, published specifications are not always directly comparable. Some suppliers report maximum force, while others emphasize finished diameter or motor power. That makes rankings partly subjective. This list therefore combines documented specifications with application experience, serviceability, and realistic production needs. The “best” machine depends on your tube material, daily volume, tolerances, and available budget. There is no universal winner.
What Is a Pipe Swaging Machine and How Does It Work?
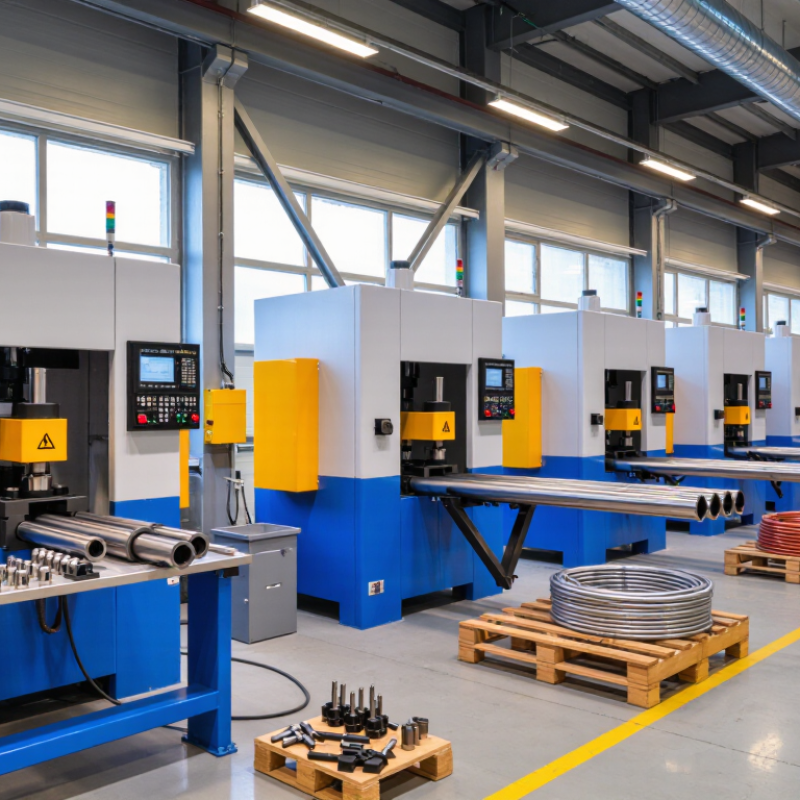
A pipe swaging machine reduces or expands a pipe’s end to create a controlled connection. Unlike cutting tools, it reshapes the metal while preserving the pipe’s basic length. The machine is used in plumbing, heat-transfer systems, automotive assemblies, and industrial fabrication. Common workpieces include steel, copper, aluminum, and selected alloy pipes.
How does it work? The operator places the pipe over a forming die or inside a matching tool. A hydraulic, mechanical, or servo-driven system then applies steady radial pressure. The die moves inward, outward, or along a shaped path. This action changes the pipe diameter and forms features such as tapers, steps, and socket ends. Accurate alignment matters. Even a small offset can cause uneven walls, surface marks, or a poor fit.
The top 10 pipe swaging machines may differ in capacity, control method, tooling range, and production speed. A compact manual unit suits repair work, while a programmable machine supports repeatable factory output. In practice, operators should check material thickness, die condition, lubrication, and final dimensions. The process is not perfectly forgiving. Excessive force can crack hardened tubing, while insufficient force may leave an incomplete shape. A careful trial piece helps, although it can slow production. That trade-off deserves attention. Reliable results also depend on calibrated measuring tools, documented settings, and trained operators who can recognize defects before installation.
Key Criteria for Evaluating Pipe Swaging Machines
Evaluating the top 10 pipe swaging machines requires more than comparing maximum force. Start with pipe materials, outside diameters, wall thicknesses, and required profiles. A suitable machine should cover the real production range, not an impressive brochure maximum. Check forming force, die alignment, stroke control, and repeatability under heat and vibration. ISO 12100 emphasizes risk assessment and safer machine design. Guarding, two-hand controls, emergency stops, and safe die changes need documented verification.
Cycle time matters, but measure the complete cycle. Include loading, clamping, forming, unloading, and inspection. Deloitte’s 2024 smart manufacturing survey found that 86% of manufacturing leaders viewed smart manufacturing as important to competitiveness. This supports demand for traceable controls and production data. Look for recipe storage, force monitoring, alarm history, and exportable records. Yet connectivity can become expensive clutter. If operators cannot understand a screen with gloves on, the feature has failed.
Energy and maintenance also separate credible candidates. The U.S. Department of Energy’s Improving Compressed Air System Performance sourcebook reports that leaks can waste 20–30% of compressor output. For pneumatic auxiliaries, inspect leak detection, standby consumption, and service access. Hydraulic versions need filtration, hose quality, temperature control, and leak containment. Calculate five-year costs, including dies, calibration, training, downtime, and spare parts. I would request sample parts from three materials and test them independently. Ratings alone are not evidence. A small trial may reveal springback, ovality, or inconsistent end length that a polished demonstration hides.
Performance, Applications, and Limitations of Each Machine
What Are the Top 10 Pipe Swaging Machines?
Performance depends on wall thickness, alloy, diameter, and production volume.
Rotary Swager
The rotary swager delivers fast, repeatable reductions for automotive tubes and aerospace fittings. Its limitation is tooling cost and noise.
Hydraulic Swager
A hydraulic swager handles larger diameters with strong forming force. It suits structural tubing, but cycle times can be slower.
Mechanical Eccentric Swager
A mechanical eccentric swager offers high output for standardized parts. It struggles with frequent size changes.
CNC Rotary Swagers
CNC rotary swagers improve dimensional control and support complex profiles. However, programming and maintenance require trained technicians.
Radial Forging Machines
Radial forging machines produce deep reductions with excellent material flow. They fit heavy-wall pipe, though their footprint is substantial.
Orbital Swagers
Orbital swagers reduce localized sections with lower impact loads. They are useful for medical and precision assemblies, but tooling alignment is critical.
Tube-End Forming Machines
Tube-end forming machines create beads, flares, and grooves efficiently. They are less suitable for long, continuous reductions.
Roll Swagers
Roll swagers provide smooth surfaces and stable geometry. Their limitation is weaker performance on irregular profiles.
Pneumatic Bench Swagers
Pneumatic bench swagers remain practical for repair shops and low-volume work. They are affordable, but operator consistency can vary.
Hot Swaging Lines
Hot swaging lines process difficult alloys with lower forming resistance. They support high-strength applications, yet heating adds energy demand and oxidation control.
The International Energy Agency reports that industry uses about 37% of global final energy demand in Energy Technology Perspectives 2024. The U.S. Department of Energy also identifies process heat as a major industrial energy burden. These figures make efficient forming cycles worth measuring, not assuming.
Real workshops know the ranking is not absolute. A smaller CNC machine may outperform a larger hydraulic unit on repeatability. My own caution is simple: published capacity rarely reveals setup time, scrap rates, or operator learning curves.
How to Choose the Right Pipe Swaging Machine for Your Needs
What Are the Top 10 Pipe Swaging Machines?
Choosing among the top ten pipe swaging machines starts with the pipe, not the machine name. Check material, outside diameter, wall thickness, and the required reduction. Stainless steel may need steadier force than mild steel. Copper often needs gentler forming. A rotary swager suits repeated, accurate reductions, while a hydraulic model handles larger pipes and heavier workloads. Mechanical machines can be economical for regular production. CNC systems add programmable control and consistent results.
Think about your real workshop conditions. Measure available floor space, electrical capacity, noise levels, and operator skill. Confirm that suitable dies are available for your pipe sizes. Die changes should feel secure, not awkward. Ask about stroke length, maximum force, cycle time, and emergency controls. A machine that works quickly but overheats during an afternoon shift is not a practical choice. It may look impressive in a catalogue.
I have seen operators choose capacity far above their daily needs, then struggle with energy use and maintenance. That mistake is easy to repeat. A smaller machine may provide better control for thin-wall tubing, but it could limit future orders. Review sample swages before purchasing. Inspect roundness, surface marks, end alignment, and wall thinning under actual settings. Service access matters too. If a worn die requires specialized support, downtime can become expensive. Leave room for doubt, and test the machine with your most difficult pipe rather than your easiest one.
This chart compares ten common nominal pipe sizes by standard outside diameter. Pipe swaging machine capacity should exceed the largest required outside diameter and accommodate the material, wall thickness, forming length, and production volume. The outside-diameter values are based on ASME B36.10M dimensional references; always verify the actual tube or pipe specification before selecting equipment.



 Português do Brasil
