High quality exotic piping products from approved manufacturers - We are the market leaders

Who Are the Top 10 Acrylic Based UV Resin Suppliers?

Acrylic Based Uv Resin serves many roles in coatings, inks, adhesives, and 3D-printing formulations. Buyers often compare cure speed, adhesion, clarity, viscosity, and resistance to yellowing. Yet a resin that performs well on a supplier’s test panel may behave differently on a production line. Substrate, lamp wavelength, film thickness, and additives all matter. Small details matter.

This guide examines ten suppliers through practical purchasing criteria: product range, technical documentation, customization, quality controls, and access to application support. It also considers whether suppliers publish useful data, such as viscosity ranges, recommended curing conditions, and storage guidance. A polished catalog is helpful, but it cannot replace a representative sample and a controlled trial. Ask for current technical data sheets and confirm that specifications match the grade under review.

Supplier fit depends on intended use, production volume, region, and required performance. Some companies may suit broad industrial sourcing, while others may offer more focused formulation support. That distinction is not always obvious from a website. The ranking should therefore be treated as a starting point, not a guarantee of the best purchase. Verify claims directly, compare samples under the same conditions, and document results before scaling up. The best choice is the one that meets measurable requirements consistently, with support that remains dependable after the first order. Even then, surprises happen. A careful comparison reduces them, but never removes every uncertainty.
Who Are the Top 10 Acrylic Based UV Resin Suppliers?

Define Acrylic UV Resin Chemistry: Oligomers, Monomers, and Photoinitiators

Who Are the Top 10 Acrylic Based UV Resin Suppliers?

Define Acrylic UV Resin Chemistry: Oligomers, Monomers, and Photoinitiators

Acrylic UV resin is a reactive blend, not a single ingredient. Oligomers form its backbone and strongly influence hardness, flexibility, adhesion, and viscosity. A supplier’s oligomer choice can change how a coating feels on a cured surface. Some acrylated urethanes bend well; epoxy acrylates often deliver harder films. These are tendencies, not guarantees. Formulation details matter.

Monomers reduce viscosity and join the polymer network during curing. Their chemistry affects flow, shrinkage, and final flexibility, so “low viscosity” alone says little about performance. Photoinitiators absorb suitable light and create reactive species that start polymerization. Match their absorption range to the lamp and the film thickness. Otherwise, the surface may cure while deeper layers remain soft. Small details matter. Grand View Research’s UV-curable coatings market report estimated a 2023 global market of about US$7.1 billion, with growth projected at roughly 8% annually through 2030. That scale reflects broad demand, but it does not prove every resin suits every process. Compare technical data sheets, test adhesion on the actual substrate, and check cure under your production lamp. A datasheet can still leave unanswered questions.

Map Curing Technology: UV-A at 315–400 nm and LED Peaks at 365/385/395 nm

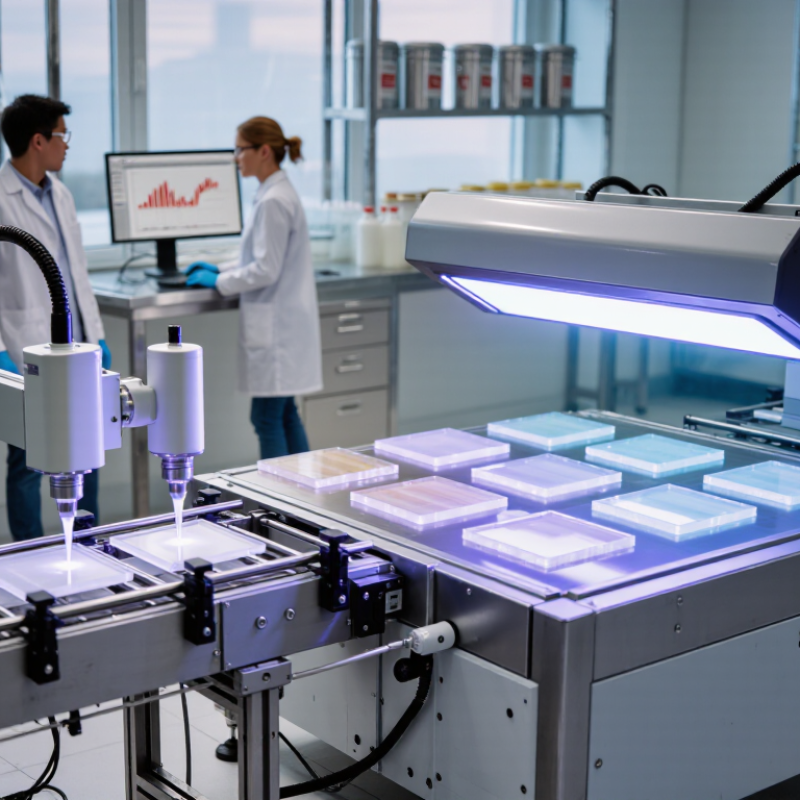
For acrylic-based UV resin suppliers, the key question is not simply whether a resin cures under UV light. It is whether the photoinitiator system matches the lamp’s emission spectrum. ISO 21348:2007 defines UV-A as 315–400 nm, placing 365, 385, and 395 nm LEDs inside the same broad band. Their peaks are not interchangeable, though. A 395 nm peak sits just 5 nm below the band’s upper limit, while 365 nm sits 50 nm above its lower limit. Small differences matter.

Ask suppliers for the LED’s measured emission curve, not only its stated peak. Then compare it with the resin’s absorption data, recommended irradiance, and curing dose. A peak wavelength alone does not show how much light falls outside the peak. Check the cured film at its actual thickness; a clear surface can hide incomplete curing below. I would also record exposure time and lamp distance, because bench tests can mislead. That detail gets missed. IEC 62471:2006 provides a photobiological-safety framework for evaluating optical radiation, while ISO 21348 supplies the wavelength-band reference. Use these technical references alongside supplier test data, and treat any “works with all UV LEDs” claim cautiously. A practical comparison starts with three columns: 365, 385, and 395 nm.

Compare Supplier Metrics: Viscosity, Cure Dose (mJ/cm²), Shrinkage, and VOC

Viscosity affects how an acrylic-based UV resin flows, levels, and holds its shape. Compare values only when test temperature and measurement method match. A resin measured at 25°C may behave differently on a cool production floor. Ask suppliers for the spindle, speed, and temperature used. Small details matter.

Cure dose, reported in mJ/cm², indicates the energy needed under stated test conditions. Check wavelength, lamp type, film thickness, and exposure time before comparing figures. A low dose is not automatically better if the resin cures unevenly in deeper areas. Shrinkage deserves equal attention. It can pull at edges, distort thin parts, or stress a bond. Request the test method and sample geometry, not just a percentage. A tidy table can mislead.

VOC data should specify what was measured and how. Ask for a test report and clarify whether the figure covers the uncured formulation or another sample state. Supplier metrics are useful screening tools, not guarantees of line performance. I would verify shortlisted materials with the actual lamp, substrate, and coating thickness. One weakness in my own screening is relying too heavily on headline numbers; real parts often reveal the mismatch.

Profile 10 Global Suppliers by Product Range, Markets, and Technical Support

An informed review of ten global acrylic-based UV resin suppliers should compare more than catalog size. Product ranges may include low-viscosity bonding grades, flexible coatings, and high-build formulations for controlled dispensing. Some suppliers focus on electronics or optical assembly, where clarity and low shrinkage matter. Others serve automotive, packaging, and industrial finishing markets, prioritizing adhesion and weather resistance. Small details count. Request wavelength-specific cure data, viscosity ranges, and samples tested on your actual substrate. A resin that cures under a bench lamp may behave differently inside a shaded joint.

Supplier profiles also differ in technical support. Larger international suppliers may offer regional distribution, application laboratories, and structured troubleshooting. More specialized producers may provide faster formulation adjustments but serve fewer markets. Ask whether support includes dispensing advice, cure testing, and help diagnosing tacky surfaces or brittle edges. Check how clearly technical sheets describe test conditions; some comparisons are difficult when lamp intensity or sample thickness is missing. This is an imperfect way to rank suppliers, but practical trials often reveal more than polished catalogs. Request comparable samples and record cure time, adhesion, and appearance under the same conditions.

Verify Performance with ASTM D3359 Adhesion and ASTM D3363 Hardness Tests

When comparing acrylic-based UV resin suppliers, request test results for the same substrate, film thickness, and curing conditions. ASTM International’s ASTM D3359 describes tape-based coating adhesion tests, with ratings from 0B to 5B; higher ratings indicate less coating removal. The result is not a universal bond-strength value. A smooth panel can hide problems that appear on a curved part or after moisture exposure. Small details matter.

ASTM D3363 measures pencil hardness, using grades from 6B through 9H. A harder reading may suit a scratch-prone surface, but it does not prove better impact resistance or adhesion. Ask suppliers to report the pencil grade, cure dose, and conditioning time, then compare like with like. Keep a retained sample. That helps. I would still treat a clean laboratory result as a starting point, not a guarantee of production performance. These ASTM methods provide a shared testing language, but the buyer’s actual substrate and process must shape the final decision.

Who Are the Top 10 Acrylic Based UV Resin Suppliers? - Verify Performance with ASTM D3359 Adhesion and ASTM D3363 Hardness Tests
Anonymous supplier slot Acrylic UV resin profile to verify ASTM D3359 adhesion ASTM D3363 pencil hardness Evidence needed before comparison
Supplier 1 Request the exact resin grade, recommended film thickness, and compatible substrate range. Not verified. Request the test method (A or B), substrate, coating thickness, and reported rating. Not verified. Request the pencil grade and test conditions. Current technical data sheet and a test report for the proposed grade.
Supplier 2 Confirm whether the product is a 100% solids, UV-curable acrylic formulation or an oligomer intended for formulation. Not verified. Results should identify substrate preparation and cure conditions. Not verified. Results should identify coating thickness and conditioning. Grade-specific documentation and reports from a defined test setup.
Supplier 3 Ask for the recommended UV wavelength range and cure-dose guidance for the specific formulation. Not verified. Compare ratings only when substrate and test method are stated. Not verified. Compare pencil grades only when cure and film conditions are stated. Technical data sheet plus documented curing parameters.
Supplier 4 Check viscosity, recommended application method, and any stated formulation limits. Not verified. No supplier-specific result is asserted here. Not verified. No supplier-specific result is asserted here. Current product specification and independently traceable test results.
Supplier 5 Confirm intended use and suitability for the target substrate and coating process. Not verified. Request the full ASTM D3359 method and rating, not a standalone number. Not verified. Request the ASTM D3363 pencil grade and test details. Test reports for the intended substrate, surface preparation, and cure process.
Supplier 6 Ask whether the grade requires photoinitiator or other components to achieve the stated cure. Not verified. Adhesion is substrate- and preparation-dependent. Not verified. Hardness is formulation- and cure-dependent. Complete formulation guidance and grade-specific test documentation.
Supplier 7 Request the recommended storage, handling, and processing conditions for the grade. Not verified. Confirm test method, substrate, and conditioning before comparing. Not verified. Confirm pencil set, coating thickness, and conditioning before comparing. Technical data sheet, safety data sheet, and relevant test reports.
Supplier 8 Clarify whether published performance relates to the supplied resin alone or a finished coating formulation. Not verified. Finished-coating results should not be attributed to a raw resin without supporting details. Not verified. Finished-coating results should not be attributed to a raw resin without supporting details. Test sample composition and report identifying the tested material.
Supplier 9 Check whether the grade is intended for a specific application, such as a coating, ink, or adhesive formulation. Not verified. Request results on a substrate relevant to the intended application. Not verified. Request results for the intended film build and cure conditions. Application-specific recommendations and traceable test reports.
Supplier 10 Confirm grade identity, specification revision, and consistency of the supplied product. Not verified. Require a report tied to the exact grade and test conditions. Not verified. Require a report tied to the exact grade and test conditions. Grade-specific certificate or specification and supporting ASTM test reports.
These are anonymous evaluation slots, not a ranked supplier list; no supplier names or supplier-specific performance results are provided. ASTM D3359 ratings depend on the selected method and test conditions; ASTM D3363 reports pencil-hardness grades. Both tests should be performed on a defined coating system and substrate, with preparation, film thickness, and curing conditions documented.

England

Special Piping Materials Ltd Broadway, Globe Industrial Estate, Dukinfield, Cheshire, SK16 4UU, United Kingdom

Scotland

Special Piping Materials (Scotland) Ltd Moss Road, Gateway Business Park, Aberdeen, AB12 3GQ

USA

Special Piping Materials INC 4615, Kennedy Commerce Drive, Houston, Texas-77032

Brazil

Special Piping Materials Do Brasil Ltda. Warehouse Stock & Office Estrada do Mato Alto, 912 Campo Grande – RJ – CEP 23036-150

Singapore

Special Piping Materials (Singapore) Pvt Ltd 43, Kian Teck Drive, Singapore-628856

Dubai

Special Piping Materials Fze P.O.Box: 120667, Sharjah Airport Free Zone, Sharjah – UAE

Oman

Special Piping Materials Authorised representative for Oman Petrovision International LLC, PB NO: 1497, Postal Code 133, Al Khuwair, Oman.

Australia

Special Piping Materials Australia Pty Ltd 11 Purser Loop Bassendean Western Australia 6054
© Copyright 2025. Special Piping Materials.
Website Design by nvisage