Top Kraft Paper Tape Laminating Machine Manufacturers
Choosing a Kraft Paper Tape Laminating Machine is not merely a purchasing exercise. It is a production decision that affects adhesive performance, tape strength, surface appearance, and operating costs. Leading manufacturers must therefore prove more than attractive machine specifications. They should demonstrate stable web tension, accurate adhesive coating, dependable drying, and responsive technical support.
Packaging machinery consultant Elena Marquez states, “A laminating line is only as reliable as its tension control, adhesive consistency, and operator discipline.” That observation deserves attention. During factory evaluations, small details often reveal real capability: a steady unwind roll, clean adhesive edges, consistent laminate pressure, and simple access to the coating station. These details matter.
Performance comes first.
This guide examines top Kraft Paper Tape Laminating Machine manufacturers through practical and technical criteria. It considers machine structure, production speed, material compatibility, automation, energy use, maintenance access, quality control, and after-sales service. Manufacturer experience also matters, especially when a line must handle changing kraft paper grades or different adhesive systems.
No ranking is perfect. A supplier with excellent engineering may offer limited local service. Another may provide strong support but fewer customization options. Buyers should compare verified production data, sample results, warranty terms, and operator feedback before deciding. Clear documentation is essential.
The strongest manufacturers are not always the loudest. They are the companies that explain limitations honestly, test materials carefully, and improve designs after real production problems appear. That practical attitude provides a more reliable starting point for selecting the right laminating partner.
Kraft Paper Tape Laminating Machines: Definition and Core Functions
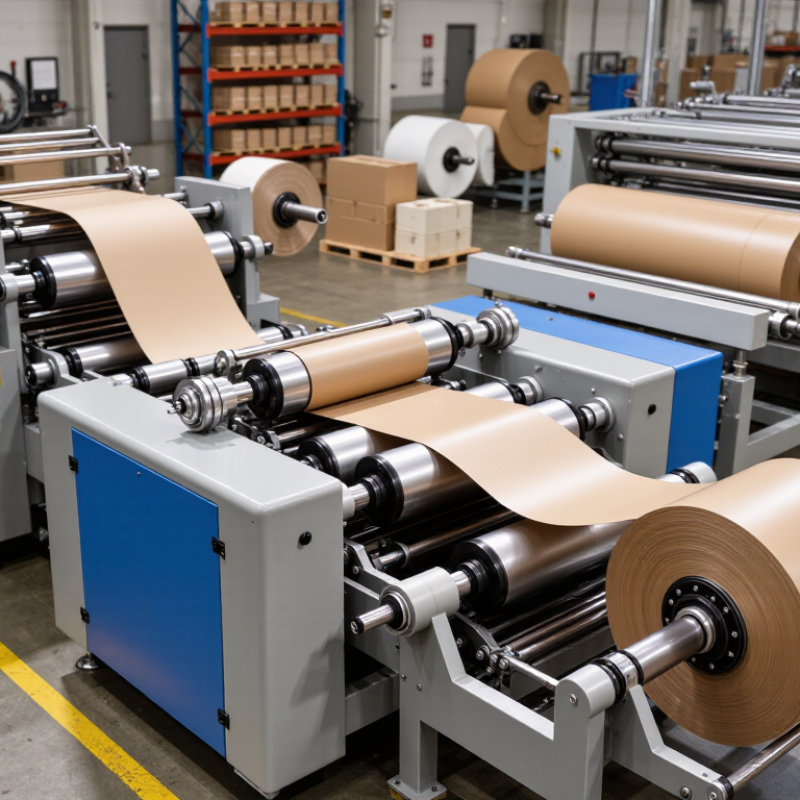
A Kraft paper tape laminating machine bonds kraft paper with adhesive layers or supporting films to create stronger, functional tape stock. It uses controlled unwinding, adhesive coating, lamination pressure, drying, and rewinding. The equipment may handle water-based, hot-melt, or solvent-free adhesive systems, depending on product design and factory requirements. Its central job is simple: keep layers aligned while building a stable composite roll. Simple in theory. Difficult in production.
Core functions begin with tension control. Sensors regulate each web as paper passes through rollers, reducing wrinkles and edge drift. A coating head applies a measured adhesive film, while heated or chilled rollers support bonding. Drying tunnels remove moisture when water-based adhesive is used. Slitting units then divide wide master rolls into narrower widths. Operators also inspect coating weight, peel strength, roll hardness, and visual defects. A clean edge matters. So does consistent winding.
From practical machine evaluations, reliable performance depends on more than maximum speed. Frame rigidity, accessible cleaning points, recipe storage, emergency protection, and stable temperature control affect daily output. Test runs should use the intended kraft paper grade and adhesive, not only ideal laboratory samples. Small variations in paper porosity can change drying time and bond strength. No setting stays perfect. Experienced teams record these changes and adjust carefully, though occasional trial and error remains unavoidable. A thoughtful manufacturer should document tolerances, maintenance intervals, and operator training clearly.
How to Evaluate Leading Machine Manufacturers
Evaluating kraft paper tape laminating machine manufacturers requires more than comparing quoted prices. Smithers’ The Future of Paper Packaging to 2028 projects steady annual growth in paper packaging demand, near 3% in several regions. That growth increases pressure on converters to reduce waste and maintain stable output. Ask each manufacturer for verified line speed, usable web width, coating tolerance, and start-up waste figures. A machine claiming 250 meters per minute means little without substrate thickness, adhesive type, and test conditions.
Request a recorded factory acceptance test using your kraft paper and adhesive. Watch the unwind tension, splice response, edge alignment, and curing consistency. Industry 4.0 reports from PMMI repeatedly identify data visibility and predictive maintenance as major investment priorities. Therefore, inspect alarm history, sensor access, remote diagnostics, and production data exports. A clear maintenance schedule matters more than a glossy interface. It is easy to overlook.
Check whether the manufacturer has trained service engineers near your plant. Ask for documented response times, spare-parts availability, installation records, and operator training hours. Total cost should include energy use, cleaning labor, rejected rolls, and planned downtime. ISO 9001 certification can support process reliability, but it does not prove laminating performance. Review audited quality records and references from comparable production environments. My own evaluation would also include a deliberately difficult trial: thin paper, a fast speed change, and a low-temperature restart. Real factories are rarely perfect.
Top Manufacturers Compared by Technology and Production Capacity
Top kraft paper tape laminating machine manufacturers should be compared through measurable technology and production capacity, not catalog claims. FAO’s Forestry Production and Trade 2023 reported global paper and paperboard production of about 417 million tonnes in 2022. This scale increases pressure on converters to reduce waste, stabilize coating quality, and shorten changeovers.
Technology matters first. Advanced manufacturers offer servo-driven web control, automatic tension correction, edge guiding, and closed-loop adhesive monitoring. These systems help maintain uniform layers when kraft paper changes from 60 to 120 gsm. Typical high-capacity lines may reach 80–150 meters per minute, but speed alone proves little. A slower line with stable tension can produce more saleable rolls. Ask for factory acceptance test data, including coating weight variation, splice rejection, energy consumption, and reel diameter. Small details matter.
Capacity needs a wider definition. PMMI’s 2024 packaging machinery outlook highlights automation, labor availability, and faster changeovers as major investment factors. Therefore, compare annual output, shift patterns, installed base, spare-parts response, and commissioning resources. A manufacturer producing 20 million square meters yearly may still be unsuitable for a narrow-width converter. Conversely, a flexible 60-meter-per-minute line could fit better. ISO 29862 and ASTM D1000 testing can support peel and adhesion verification, although machine performance depends heavily on adhesive formulation and paper moisture. One weakness remains: published figures often describe maximum speed, not sustained production. Buyers should request three-day trial records, not polished demonstrations.
Top Kraft Paper Tape Laminating Machine Manufacturers - Top Manufacturers Compared by Technology and Production Capacity
| Manufacturer Category | Primary Technology | Typical Machine Configuration | Working Width | Operating Speed | Suitable Paper Range | Estimated Output Capacity | Best Application |
| High-Capacity Integrated Line | Continuous roll-to-roll laminating with automatic tension control and multi-zone drying | Unwinder, precision adhesive coater, heated laminating rollers, drying tunnel, edge trimming, automatic rewinder and roll slitter | 1,300–1,600 mm | 150–250 m/min | 40–120 g/m² kraft paper | 25–45 tonnes/month | Large-scale production of reinforced, gummed and industrial packaging tape |
| Advanced Servo-Controlled Line | Water-based adhesive coating with servo-driven web alignment and closed-loop tension control | Automatic splicer, gravure or reverse-roll coater, hot-air drying, laminating nip, inspection system and turret rewinder | 1,000–1,400 mm | 100–180 m/min | 45–100 g/m² kraft paper | 18–32 tonnes/month | Consistent commercial-grade kraft paper tape with high coating uniformity |
| Flexible Multi-Process Line | Modular laminating and coating platform supporting water-based, starch-based and hot-melt adhesive systems | Single or twin unwinder, interchangeable coating head, compact dryer, laminating station and center-surface rewinder | 800–1,300 mm | 80–150 m/min | 35–120 g/m² kraft paper | 12–26 tonnes/month | Custom tape grades, recycled kraft products and frequent product changeovers |
| Mid-Range Production Line | Standard roll laminating with pneumatic pressure control and automatic temperature regulation | Manual or semi-automatic splicing, coating station, heated rollers, short drying section and two-shaft rewinder | 600–1,200 mm | 50–110 m/min | 50–120 g/m² kraft paper | 7–18 tonnes/month | Regional tape converters and medium-volume packaging operations |
| Compact Entry-Level Line | Basic adhesive coating and laminating with manual web alignment | Single unwinder, compact coating unit, heated laminating roller, natural or electric drying and manual roll change | 400–900 mm | 20–70 m/min | 60–120 g/m² kraft paper | 2–9 tonnes/month | Small-batch production, product testing and local packaging supply |
Comparison basis: Capacity estimates assume one production shift of approximately 8 hours per day, 22 operating days per month, and normal allowances for setup, cleaning, roll changes and downtime. Actual output varies with adhesive type, coating weight, paper moisture, web width, finished-roll specifications and operating schedule.
Choosing the Right Manufacturer for Your Business Needs
Choosing a kraft paper tape laminating machine manufacturer requires more than comparing prices. The right partner should understand your paper weight, adhesive type, production speed, and finished roll dimensions. Ask for verified test results using materials close to yours. A machine may perform well in a showroom, yet behave differently with recycled paper or moisture-sensitive adhesive.
Experience matters. Check how long the manufacturer has supported similar converting lines. Request customer references, service records, and details about operator training. Reliable manufacturers explain maintenance intervals, spare-part availability, and expected energy use clearly. They should also provide documented safety features and quality-control procedures. Avoid vague promises. Specific answers reveal practical knowledge.
Tips: Prepare sample materials before contacting suppliers. Ask for a live trial. Measure coating uniformity, edge alignment, winding tension, and waste percentage. Discuss installation time and remote support before signing. A detailed warranty is useful, but response time matters more during a breakdown. I once underestimated training needs; the machine was capable, but small setup errors caused uneven rolls. That mistake changed how I assess suppliers. Do not judge solely by polished brochures. Inspect the factory, question the engineers, and compare actual operating data. A slightly slower machine may prove more dependable for your daily workload.
Top Kraft Paper Tape Laminating Machine Manufacturers
Choosing the right laminating machine starts with matching line speed to planned production volume. The chart shows the theoretical web output during one continuous 8-hour shift at different operating speeds.
Calculation basis: Theoretical output = line speed × 480 minutes. Actual production may be lower because of setup time, material changes, cleaning, maintenance, and downtime.



 Português do Brasil