A Laser Tube Cutter shapes round, square, and rectangular metal profiles with a focused beam. It can cut openings, slots, and angled ends without changing tools for every feature. In a workshop, the process may begin with a steel tube resting in a loading rack. A chuck grips and rotates it as the cutting head follows the programmed path. The beam melts or vaporizes a narrow strip of material, while assist gas clears the cut. Small details matter: tube alignment, wall thickness, and focus can all affect edge quality.
The machine combines a laser source, motion controls, a rotary chuck, and software that interprets the part design. Laser technology expert Dr. Reinhart Poprawe is known for his work in laser processing. A verified, topic-specific quotation from him was not available for this introduction, so I will not invent one. A useful summary of the engineering principle is this: precision depends on coordinating energy, motion, and material response. That is a paraphrase, not a direct quotation.
The next sections explain how the machine handles a tube, turns a digital design into tool movement, and produces each cut. They also cover practical limits, including material choice, tube geometry, and setup quality. Not every cut comes out perfect. Burrs, heat marks, or slight dimensional variation can still appear, especially when settings or fixtures are poorly matched. Understanding the process helps buyers and operators ask better questions before production begins.
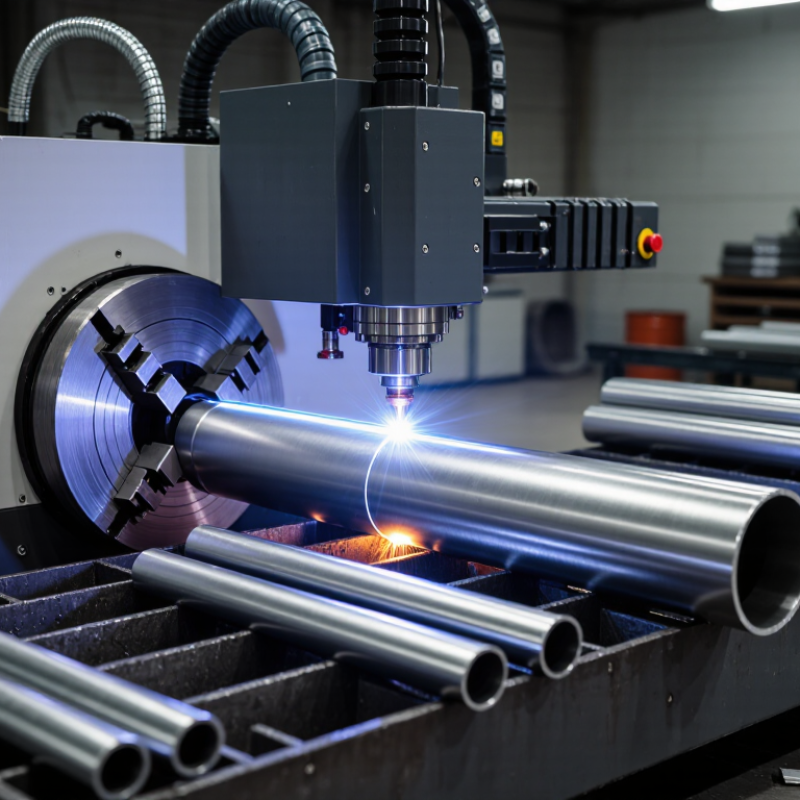
A laser tube cutter is a computer-controlled machine that cuts hollow metal sections with a focused laser beam. It can process round, square, and rectangular tubes, along with some custom profiles. A chuck grips and rotates the tube while the cutting head follows programmed paths. The beam heats a small area until the material separates, and assist gas helps clear molten metal. The machine can create holes, slots, notches, and angled ends without changing tools for each feature. It is not magic. Material type, wall thickness, focus, and setup all affect the cut.
In practice, an operator loads the tube, checks its dimensions, and enters or imports a cutting layout. Sensors and software can help locate the workpiece, but a bent or dented tube may still cause errors. That detail is easy to underestimate. Tube cutting can reduce manual measuring and trimming, though parts still need inspection. It is especially useful when several features must line up accurately along one piece.
Tips: Check the tube’s actual size and wall thickness before cutting. Secure it firmly, and test unfamiliar settings on a short offcut. Inspect for burrs and heat discoloration before assembly.
A laser tube cutter combines a focused beam with a system that holds and rotates hollow metal sections. Its components work together to keep the beam aligned as the tube moves. That coordination matters.
The laser source generates the energy used to cut, while the cutting head focuses it through a lens and directs it toward the tube. A nozzle surrounds the beam and delivers assist gas to clear molten material from the cut. The head must stay at a suitable distance from the surface; even a small gap change can affect cut quality. Not just the laser.
A chuck or clamping unit grips the tube and rotates it, while a support bed limits sagging along longer pieces. The motion system moves the head or tube along programmed paths. A controller coordinates these movements and adjusts settings such as speed and power. Sensors may detect the tube’s position or help maintain focus. An extraction system removes smoke and fine particles from the cutting area.
Each machine arranges these parts a little differently. In practice, setup still matters: a poorly supported tube can wobble, leaving uneven edges. Small details count. Operators should check alignment, clamps, and consumables before cutting, since component wear can change results over time.
A CNC controller coordinates the tube chuck and motion system with the laser. The laser source generates the beam, which travels through beam-delivery optics to the cutting head. The focused beam and assist gas cut the tube. The numbers show functional workflow order, not component performance; several systems operate together during cutting.
A laser tube cutter uses a focused beam to cut profiles into metal tubing. The operator loads a straight tube onto support rollers and secures it in a chuck. The cutting program usually comes from a CAD drawing. Before cutting, the operator checks the tube’s material, diameter, and wall thickness. These details affect focus, speed, and power settings. Small errors matter.
The machine aligns the tube and positions the cutting head. Depending on its design, the chuck rotates the tube, or a feed system moves it through the machine. The laser pierces the wall, then follows the programmed path to create slots, holes, or shaped ends. Assist gas clears molten material from the cut. Sensors may monitor positioning, but they cannot correct every setup problem. A test cut can expose issues that looked fine on screen.
Tips: Check that the tube is seated evenly before starting. Remove scale or oil near the cutting area when needed. Inspect the first cut for burrs and rough edges. If results differ across the tube, pause and recheck alignment and settings. A perfect drawing does not guarantee a perfect part.
A laser tube cutter can process many common metals, but the result depends on the laser source, power, wall thickness, and setup. Mild steel and stainless steel are frequent choices. Aluminum, brass, and copper can also be cut on suitable systems, though reflective metals need careful process control. Not every tube behaves alike. A thin stainless tube may cut cleanly, while a thicker section of the same alloy can need slower settings and more heat management.
The shape matters too. Round, square, and rectangular tubing are widely used, and some machines can handle oval or other formed profiles. A chuck rotates the tube as the cutting head follows the programmed path. This allows holes, slots, and angled ends to be cut without moving the workpiece by hand. Fit matters. Tubes must be held securely and aligned; otherwise, features can land slightly off position.
Open profiles and unusual shapes may be possible, but compatibility depends on the machine’s chuck and support system. Small-diameter tubes can flex, while long sections may sag if they lack support. Cut quality also varies with alloy, surface finish, and assist-gas settings.
A sample cut is worth the time. It can reveal burrs, heat marks, or distortion before a full production run. A material list alone rarely tells the whole story.
A laser tube cutter uses a focused beam and programmed movement to cut round, square, or rectangular metal profiles. The machine can also make slots and holes before a tube is assembled. This helps shops produce repeatable parts with fewer manual cutting steps. The exact result depends on tube thickness, material, machine setup, and how securely the tube is held.
These cutters are common in furniture manufacturing, where steel or aluminum frames need clean joints and accurately placed openings. A chair leg, for example, may require an angled end and a mounting hole in the same section of tube. Automotive suppliers use cut profiles for seat structures, exhaust components, and other formed assemblies. Fitness equipment makers also use them for frames, handles, and support bars. Small details matter.
Construction and agricultural equipment manufacturers cut tubes for railings, structural supports, and machine frames. In each case, accurate cuts can reduce fitting and welding adjustments later. Less rework. Still, a laser cutter does not guarantee a perfect assembly. Thin walls can deform, and poorly chosen settings may leave rough edges or excess heat marks. Operators need to check sample parts and adjust the program when the material or design changes. Not every shop needs one. It is most useful when production involves many tube parts or repeated, precise features.
| Category | Typical Material or Profile | How It Works or Common Cutting Operations | Common Parts and Applications | Why Laser Tube Cutting Is Used |
|---|---|---|---|---|
| Basic process | Metal tubes and structural profiles, including round, square, and rectangular sections | A focused laser beam melts or vaporizes material along a programmed path. Assist gas helps clear molten material from the cut. The tube is positioned and rotated so the beam can cut around its surface. | Cut-to-length sections, openings, slots, miters, and shaped ends | It can produce precise features in multiple sides of a tube without requiring a separate tool for each profile. |
| Construction and structural fabrication | Commonly carbon steel and stainless steel tubes; round, square, and rectangular profiles | Cutting to length, angled ends, bolt holes, slots, and connection features | Frames, supports, railings, trusses, and structural assemblies | Accurate, repeatable cuts can help prepare profiles for fitting and welding. |
| Automotive and transport equipment | Steel, stainless steel, and aluminum tubes or formed profiles | Cutting holes, notches, contours, and end shapes in production components | Seat structures, chassis-related parts, exhaust components, and vehicle frames | Programmed cutting supports consistent part geometry and can reduce secondary machining for suitable designs. |
| Furniture and display products | Steel, stainless steel, or aluminum round and rectangular tubing | Cutting leg angles, joints, mounting holes, and decorative openings | Chair and table frames, shelving, display stands, and store fixtures | Complex joints and openings can be cut directly into the tube, supporting efficient assembly. |
| HVAC and fluid-handling equipment | Metal tubes and profiles selected for the system and operating environment | Cutting branch openings, ports, slots, and tube ends | Duct supports, equipment frames, manifolds, and piping-related components | Accurate openings can help components align during fabrication; application suitability depends on the material and design. |
| Agricultural and construction machinery | Often carbon steel tubing and structural profiles | Cutting reinforced joints, mounting holes, notches, and angled ends | Machine frames, guards, booms, and equipment supports | It is useful for producing repeatable features in robust tubular components. |
| Fitness and recreation equipment | Steel or aluminum tubing, including round and oval profiles | Cutting frame joints, adjustment holes, slots, and end contours | Exercise equipment frames, bicycle components, and recreational structures | Precisely cut joints can simplify fit-up and help maintain consistency across batches. |
| Material considerations | Commonly cut metals include carbon steel, stainless steel, and aluminum; some systems can process other suitable metals | Cut quality depends on material type, wall thickness, profile geometry, laser power, assist gas, and machine setup. | Applications range from light-gauge components to heavier fabricated parts, within the machine’s rated capacity | Material and thickness limits vary by machine, so cutting parameters should be selected for the specific job. |
| Cookie | Duration | Description |
|---|---|---|
| AWSALB | 7 days | AWSALB is a cookie generated by the Application load balancer in the Amazon Web Services. It works slightly different from AWSELB. |
| AWSALBCORS | 7 days | This cookie is used for load balancing services provded by Amazon inorder to optimize the user experience. Amazon has updated the ALB and CLB so that customers can continue to use the CORS request with stickness. |
| cookielawinfo-checkbox-advertisement | 1 year | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Advertisement". |
| cookielawinfo-checkbox-analytics | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytic / Performance". |
| cookielawinfo-checkbox-functional | 11 months | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional". |
| cookielawinfo-checkbox-necessary | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Strictly Necessary". |
| cookielawinfo-checkbox-performance | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance". |
| cookielawinfo-checkbox-preferences | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Preferences." |
| elementor | never | This cookie is used by the website's WordPress theme. It allows the website owner to implement or change the website's content in real-time. |
| viewed_cookie_policy | 11 months | The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data. |
| Cookie | Duration | Description |
|---|---|---|
| CONSENT | 16 years 4 months | These cookies are set via embedded youtube-videos. They register anonymous statistical data on for example how many times the video is displayed and what settings are used for playback.No sensitive data is collected unless you log in to your google account, in that case your choices are linked with your account, for example if you click “like” on a video. |
| _ga | 2 years | This cookie is installed by Google Analytics. The cookie is used to calculate visitor, session, campaign data and keep track of site usage for the site's analytics report. The cookies store information anonymously and assign a randomly generated number to identify unique visitors. |
| _gat_gtag_UA_47200144_1 | 1 minute | This cookie is set by Google and is used to distinguish users. |
| _gid | 1 day | This cookie is installed by Google Analytics. The cookie is used to store information of how visitors use a website and helps in creating an analytics report of how the website is doing. The data collected including the number visitors, the source where they have come from, and the pages visted in an anonymous form. |
| _hjAbsoluteSessionInProgress | session | This cookie is used to count how many times a website has been visited by different visitors. This is done by assigning the visitor an ID, so the visitor does not get registered twice. |
| _hjFirstSeen | 30 minutes | This is set by Hotjar to identify a new user’s first session. It stores a true/false value, indicating whether this was the first time Hotjar saw this user. It is used by Recording filters to identify new user sessions. |
| _hjid | 1 year | This cookie is set by Hotjar. This cookie is set when the customer first lands on a page with the Hotjar script. It is used to persist the random user ID, unique to that site on the browser. This ensures that behavior in subsequent visits to the same site will be attributed to the same user ID. |
| _hjIncludedInPageviewSample | session | This cookie is used to detect whether the user navigation and interactions are included in the website’s data analytics. |
| Cookie | Duration | Description |
|---|---|---|
| IDE | 1 year 24 days | This cookie is used by Google DoubleClick and stores information about how the user uses the website and any other advertisement before visiting the website. This is used to present users with ads that are relevant to them according to the user profile. |
| NID | 6 months | This cookie is used to a profile based on user's interest and display personalized ads to the users. |
| test_cookie | 15 minutes | This cookie is set by doubleclick.net. The purpose of the cookie is to determine if the user's browser supports cookies. |
| VISITOR_INFO1_LIVE | 5 months 27 days | This cookie is set by Youtube it is used to track the information of the embedded YouTube videos on a website. |
| YSC | session | This cookies is set by Youtube and is used to track the views of embedded videos. |
| yt-remote-connected-devices | never | These cookies are set via embedded youtube-videos. |
| yt-remote-device-id | never | These cookies are set via embedded youtube-videos. |
| Cookie | Duration | Description |
|---|---|---|
| qtrans_front_language | 1 year | This cookie is set by qTranslate WordPress plugin. The cookie is used to manage the preferred language of the visitor. |