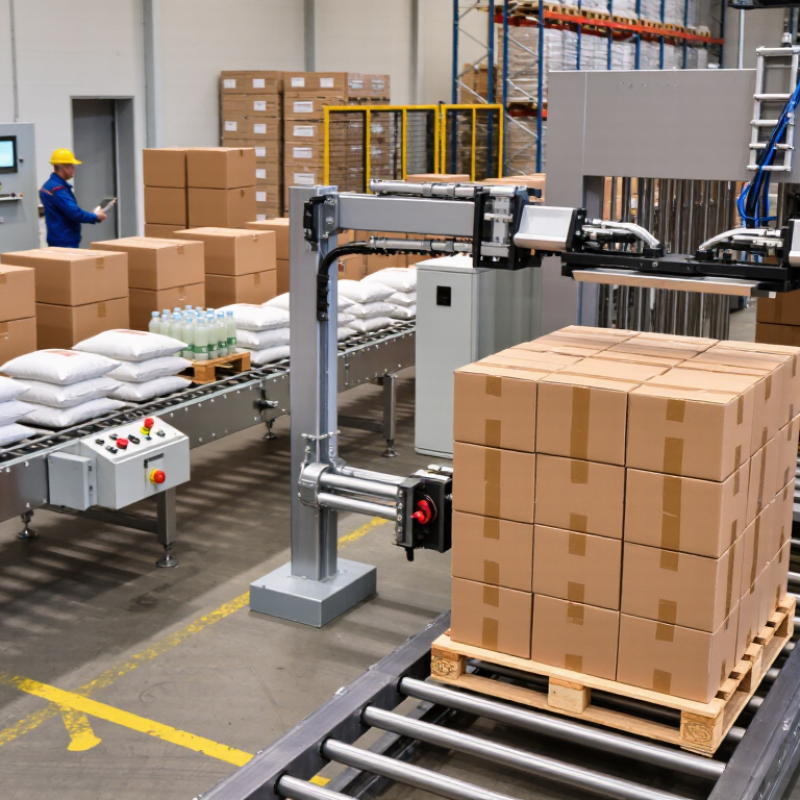
Choosing the right Palletizing Machine is not simply a matter of selecting the fastest model. The decision begins with the product, the pallet, and the people operating the line. Bags of flour behave differently from rigid cartons. Fragile bottles need softer handling and controlled acceleration. Heavy cases demand accurate gripping, stable stacking, and reliable pallet support.
Roberto Michel, an experienced materials-handling analyst, has offered a useful principle: “The best automation projects begin with a clear understanding of the process.” That advice matters when reviewing pallet patterns, case dimensions, product weight, line speed, and available floor space. A machine rated for 1,200 cases per hour may disappoint if carton sizes change frequently. Flexibility can matter more than maximum speed. Sometimes, less is better.
A practical evaluation should include gripper selection, conveyor integration, safety access, changeover time, maintenance support, and future production needs. Ask the supplier to demonstrate your actual cartons, not a similar-looking sample. Watch the machine build a complete pallet. Check corner alignment, layer stability, and film-wrapping performance. Review factory acceptance testing and service response times before signing an agreement.
No Palletizing Machine fits every factory perfectly. That is the uncomfortable part. Forecasts can be wrong, packaging may change, and operators may resist unfamiliar controls. A thoughtful choice leaves room for these weaknesses. It balances measurable output with daily usability, dependable engineering, and evidence from real production conditions.
A practical choice starts with a clear production profile, not a machine brochure. Record current output by hour, shift, and season. Include carton dimensions, product weight, pallet size, and stacking pattern. Note changes too. A line making 20 cases per minute today may need 30 next year. That gap affects gripper design, robot reach, and cycle time.
Walk the production floor with an operator and maintenance technician. Measure conveyor height, available space, pallet access, and forklift paths. Check whether cases arrive square, sealed, and consistently spaced. Small variations can create repeated jams. Define acceptable downtime, changeover time, and operator involvement. If products are fragile, dusty, cold, or irregular, document those conditions before requesting quotations. Real production rarely matches a clean specification sheet.
Set goals that can be tested. For example, target 95% line availability, a ten-minute pattern change, or reduced manual lifting per shift. Ask suppliers to demonstrate these targets using your actual cases and pallets. Request data on speed at full load, not empty-cycle performance. Review guarding, emergency stops, training, spare parts, and maintenance access against applicable local requirements. I would also challenge optimistic forecasts. Our first estimates are often too generous. Leave room for seasonal demand, product variation, and learning time. A useful specification includes what the machine must do, and what it must never compromise.
Layer palletizers build complete rows before placing them on the pallet. This method works well for uniform cartons and predictable production schedules.
Robotic arms offer more flexibility when products, pallet sizes, or stacking patterns change frequently.
Vacuum grippers handle smooth boxes effectively, while mechanical clamps may perform better with dusty or uneven surfaces. Cobot-based systems use less space, but their speed can be limited by safety requirements and payload capacity.
Operating method matters as much as machine type. A pick-and-place system may be practical for mixed cartons, while row-forming equipment can reduce handling time on stable cases. Check the infeed height, pallet exchange process, changeover steps, and access for cleaning.
Ask for tested cycle data using your actual cartons. Brochure figures can be optimistic. We have seen minor carton deformation disrupt a perfect stacking pattern. That detail is easy to miss.
Leave room for operator training, sensor adjustments, and future product changes. A machine that runs fast today may become restrictive after one packaging redesign.
Choosing a palletizing machine starts with the real load, not the advertised maximum. Payload includes the product, packaging, gripper, and dynamic forces during movement. A 20-kilogram carton may require a 30-kilogram-rated system after safety margins are applied. The first calculation is rarely perfect. Record product weights, dimensions, center of gravity, and pallet patterns from actual production samples. The International Federation of Robotics reported 541,302 industrial robots installed worldwide in 2023, showing how quickly automated handling is expanding. Yet higher automation does not remove the need for accurate site data.
Speed should be measured in completed cases per hour, including gripping, layer changes, pallet exchange, and safety pauses. A machine promising 1,000 cycles per hour may deliver less in a mixed-SKU line. Check the required rate during the busiest shift, then test a realistic buffer. Accuracy matters at every layer. Misaligned cartons can create unstable stacks, damaged corners, and manual rework. Ask suppliers to demonstrate repeatability with your actual packaging, not identical sample boxes.
Product compatibility deserves equal attention. Bags flex, cartons crush, and shrink-wrapped bundles can slide under acceleration. The gripper must match surface texture, stiffness, temperature, and allowable contact pressure. PMMI’s industry research continues to identify labor availability and flexible production as major automation drivers. That supports investment, but it is not proof of suitability. Run a documented trial, measure rejects, noise, changeover time, and operator adjustments. A tidy spreadsheet can still mislead. Production conditions are messier.
Choosing a palletizing machine starts with the floor, not the brochure. Measure conveyor height, pallet positions, aisle clearance, load dimensions, and operator access. Leave room for stretch wrapping, rejected cases, and future product changes. Real floors are rarely perfect. A layout that works in a drawing may fail when forklifts share the aisle. IFR’s World Robotics 2024 report recorded 541,302 industrial robot installations worldwide in 2023, a 10% annual increase. That growth makes practical layout planning more important, not less.
Safety features deserve an on-site risk assessment. Specify guarded zones, interlocked gates, emergency stops, light curtains, and safe restart controls. OSHA’s FY2023 data listed 1,644 machine-guarding violations, showing how basic protection still fails in workplaces. Integration also needs careful testing. Confirm signal handshakes between the palletizer, conveyors, vision devices, warehouse software, and safety circuits. Check real cycle times, not advertised speeds. Maintenance access matters too. Technicians should reach grippers, sensors, belts, and filters without climbing around the cell. Design for quick fault diagnosis, documented spare parts, and measurable mean time to repair.
Tips: Walk the proposed route with an operator and a maintenance technician. Mark every reach, stop, and blind corner. Ask what happens during a jam, product change, or power recovery. A small overlooked detail can create repeated downtime. I would also challenge optimistic assumptions about staffing and uptime; they often need revision after commissioning.
A practical comparison of common palletizing machine configurations using typical planning ranges
| Evaluation Dimension | What to Assess | Cartesian Palletizer | Articulated-Arm Palletizer | Delta Palletizer | Collaborative Palletizer |
|---|---|---|---|---|---|
| Typical Application | Match the machine to product type, packaging format, and production volume. | Stable, repetitive palletizing for cases, sacks, trays, and cartons. | Flexible handling of cases, bags, drums, and mixed product patterns. | High-speed handling of lightweight products in organized infeed streams. | Lower-volume or frequently changing lines where human-machine collaboration is useful. |
| Space Requirement | Review footprint, aisle clearance, pallet staging, guarding, and service access. | Usually requires a larger rectangular footprint and clear overhead travel space. | Generally compact around the robot base, but guarding and pallet lanes add space. | Compact footprint, but requires carefully designed overhead or gantry-mounted equipment. | Small to medium footprint; layout must include collaborative operating and replenishment zones. |
| Typical Payload | Include product, gripper, tooling, and any accumulated load. | Approximately 10–150 kg, depending on axis design and tooling. | Approximately 20–250 kg, depending on robot reach and configuration. | Usually approximately 1–20 kg per pick; best suited to lighter products. | Commonly approximately 5–25 kg, subject to collaborative speed and reach limits. |
| Throughput Planning Range | Confirm required cases per minute, product spacing, and pallet pattern changes. | Typically 8–25 cases per minute. | Typically 10–30 cases per minute, depending on reach and payload. | Typically 30–100 picks per minute for lightweight, consistently oriented items. | Typically 4–15 cases per minute, depending on collaborative operating limits. |
| Product Flexibility | Evaluate size variation, surface condition, weight distribution, and orientation. | High repeatability; changeovers may require mechanical or software adjustments. | High flexibility for different sizes, orientations, and pallet patterns. | Best with standardized, lightweight products and controlled presentation. | Good for multiple products and frequent changeovers with guided recipes. |
| Pallet Pattern Capability | Check layer count, interlocking patterns, slip sheets, and mixed-SKU requirements. | Excellent for programmed layer patterns and precise placement. | Excellent for complex patterns and orientation changes. | Suitable for simpler patterns when product flow is highly consistent. | Good for standard patterns; complex patterns can reduce cycle efficiency. |
| Safety Features | Verify risk assessment, guarding, access control, emergency stops, and safe restart logic. | Typically needs perimeter guarding, interlocked gates, light curtains, and safety-rated controls. | Typically needs perimeter guarding, restricted zones, interlocked access, and safety scanners. | Requires guarding or enclosure around high-speed motion, plus access monitoring. | May operate without full fencing only after a documented risk assessment and validated safety functions. |
| Integration Requirements | Assess conveyor interfaces, scanners, pallet dispensers, stretch wrappers, and control protocols. | Integrates well with conveyors, layer-forming equipment, pallet magazines, and warehouse systems. | Requires coordinated robot, conveyor, gripper, vision, and pallet handling controls. | Needs precise conveyor timing, product tracking, vision, and high-speed control synchronization. | Often requires simplified interfaces, operator guidance, recipe management, and safety communication. |
| Changeover Time | Measure recipe selection, gripper changes, guide adjustment, and verification time. | Often 15–45 minutes for standard product and pattern changes. | Often 10–30 minutes when recipes and automatic tooling are available. | Often less than 15 minutes for standardized products and predefined recipes. | Often 5–20 minutes with intuitive programming and quick-change tooling. |
| Maintenance Demand | Consider lubrication, belts, bearings, sensors, grippers, and access to wear parts. | Moderate; linear components and drive systems require scheduled inspection and lubrication. | Moderate; inspect joints, reducers, cables, brakes, grippers, and safety devices. | Moderate to high; high cycle rates increase wear on belts, joints, tooling, and conveyors. | Low to moderate; routine checks still include joints, tooling, sensors, cables, and safety functions. |
| Operator Skill Level | Assess programming, troubleshooting, mechanical, and electrical capabilities. | Moderate; operators need training for HMI recipes, sensors, and basic mechanical checks. | Moderate to high; robot programming and recovery procedures may require specialists. | High for optimization; timing, vision, and motion-control knowledge may be required. | Generally moderate; graphical programming can simplify routine product changes. |
| Best-Fit Production Profile | Choose when long runs, stable products, and predictable pallet patterns are priorities. | High-volume lines with a stable product range and available floor space. | Medium- to high-volume lines requiring broad product and pattern flexibility. | Very high-speed lines handling lightweight, consistent products. | Low- to medium-volume lines with variable products and limited automation space. |
| Selection Priority | Use production data and a site risk assessment before final specification. | Prioritize repeatability, payload capacity, and precise layer formation. | Prioritize flexibility, reach, tooling options, and integration capability. | Prioritize speed, product consistency, and accurate infeed control. | Prioritize safe collaboration, ease of programming, and rapid changeover. |
Choosing a palletizing machine starts with total ownership cost, not the purchase price. Include the machine, gripper, guarding, conveyors, installation, programming, training, and floor modifications. Then estimate annual electricity, preventive maintenance, spare parts, software support, labor, and unplanned downtime. A simple five-year model is useful: TCO equals initial investment plus five years of operating costs, minus residual value.
Use real production data. The International Federation of Robotics reported 541,302 industrial robot installations worldwide in 2023, showing how widely automation is entering factories. PMMI’s recent packaging industry research also identifies labor availability, flexibility, and changeover speed as important investment drivers. Therefore, compare machines by cases per minute, changeover time, uptime, and service response, not only by cycle speed. A fast machine can still lose money if it needs frequent adjustments.
Measure your current line for two weeks. Record operators per shift, rejected cases, stoppage minutes, pallet patterns, and energy use. For example, saving two operators across three shifts may justify a higher capital cost, but only if the line remains consistently loaded. My first estimate is often too optimistic. Downtime is easy to underestimate. Ask for documented uptime from comparable applications, maintenance intervals, and realistic integration costs. Include training hours and spare grippers. Small parts matter. Recalculate payback under low-volume and high-volume scenarios before selecting the machine.
| Cookie | Duration | Description |
|---|---|---|
| AWSALB | 7 days | AWSALB is a cookie generated by the Application load balancer in the Amazon Web Services. It works slightly different from AWSELB. |
| AWSALBCORS | 7 days | This cookie is used for load balancing services provded by Amazon inorder to optimize the user experience. Amazon has updated the ALB and CLB so that customers can continue to use the CORS request with stickness. |
| cookielawinfo-checkbox-advertisement | 1 year | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Advertisement". |
| cookielawinfo-checkbox-analytics | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytic / Performance". |
| cookielawinfo-checkbox-functional | 11 months | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional". |
| cookielawinfo-checkbox-necessary | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Strictly Necessary". |
| cookielawinfo-checkbox-performance | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance". |
| cookielawinfo-checkbox-preferences | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Preferences." |
| elementor | never | This cookie is used by the website's WordPress theme. It allows the website owner to implement or change the website's content in real-time. |
| viewed_cookie_policy | 11 months | The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data. |
| Cookie | Duration | Description |
|---|---|---|
| CONSENT | 16 years 4 months | These cookies are set via embedded youtube-videos. They register anonymous statistical data on for example how many times the video is displayed and what settings are used for playback.No sensitive data is collected unless you log in to your google account, in that case your choices are linked with your account, for example if you click “like” on a video. |
| _ga | 2 years | This cookie is installed by Google Analytics. The cookie is used to calculate visitor, session, campaign data and keep track of site usage for the site's analytics report. The cookies store information anonymously and assign a randomly generated number to identify unique visitors. |
| _gat_gtag_UA_47200144_1 | 1 minute | This cookie is set by Google and is used to distinguish users. |
| _gid | 1 day | This cookie is installed by Google Analytics. The cookie is used to store information of how visitors use a website and helps in creating an analytics report of how the website is doing. The data collected including the number visitors, the source where they have come from, and the pages visted in an anonymous form. |
| _hjAbsoluteSessionInProgress | session | This cookie is used to count how many times a website has been visited by different visitors. This is done by assigning the visitor an ID, so the visitor does not get registered twice. |
| _hjFirstSeen | 30 minutes | This is set by Hotjar to identify a new user’s first session. It stores a true/false value, indicating whether this was the first time Hotjar saw this user. It is used by Recording filters to identify new user sessions. |
| _hjid | 1 year | This cookie is set by Hotjar. This cookie is set when the customer first lands on a page with the Hotjar script. It is used to persist the random user ID, unique to that site on the browser. This ensures that behavior in subsequent visits to the same site will be attributed to the same user ID. |
| _hjIncludedInPageviewSample | session | This cookie is used to detect whether the user navigation and interactions are included in the website’s data analytics. |
| Cookie | Duration | Description |
|---|---|---|
| IDE | 1 year 24 days | This cookie is used by Google DoubleClick and stores information about how the user uses the website and any other advertisement before visiting the website. This is used to present users with ads that are relevant to them according to the user profile. |
| NID | 6 months | This cookie is used to a profile based on user's interest and display personalized ads to the users. |
| test_cookie | 15 minutes | This cookie is set by doubleclick.net. The purpose of the cookie is to determine if the user's browser supports cookies. |
| VISITOR_INFO1_LIVE | 5 months 27 days | This cookie is set by Youtube it is used to track the information of the embedded YouTube videos on a website. |
| YSC | session | This cookies is set by Youtube and is used to track the views of embedded videos. |
| yt-remote-connected-devices | never | These cookies are set via embedded youtube-videos. |
| yt-remote-device-id | never | These cookies are set via embedded youtube-videos. |
| Cookie | Duration | Description |
|---|---|---|
| qtrans_front_language | 1 year | This cookie is set by qTranslate WordPress plugin. The cookie is used to manage the preferred language of the visitor. |