Choosing the right Coating Agent begins with understanding what the coated surface must do. A metal part exposed to moisture has different needs from a paper package that must resist scuffing. Even two plastics can respond differently to the same formulation. The details matter: surface energy, operating temperature, exposure time, and application method can all influence the result. Small differences show up fast.
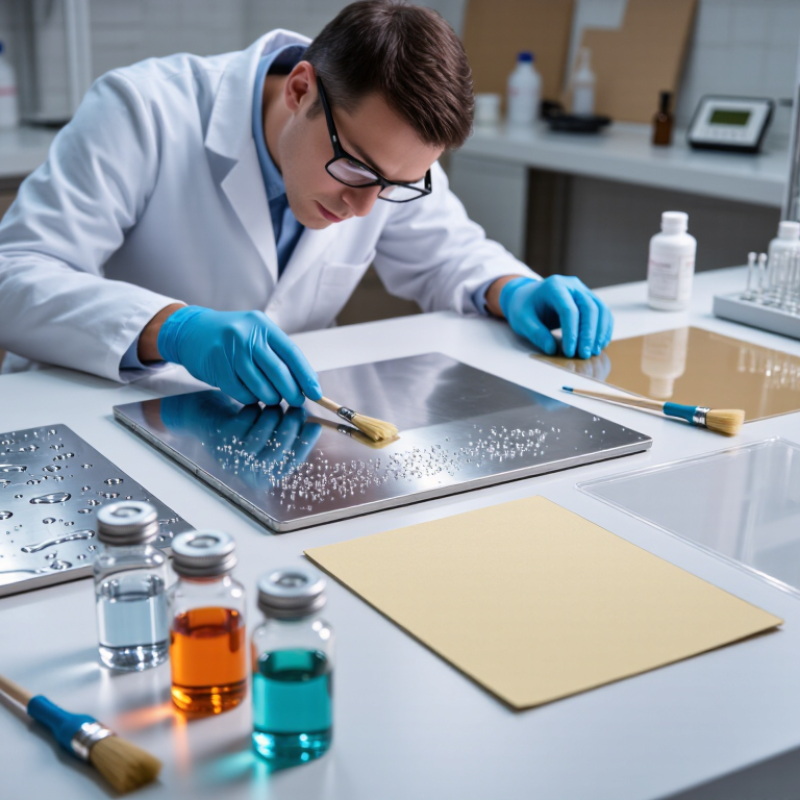
A useful selection process starts with the substrate and the required performance. Consider adhesion, flexibility, appearance, drying time, and resistance to expected wear. Then check whether the agent suits the available equipment and production conditions. A coating that performs well in a laboratory may behave differently on a fast production line. That gap is easy to overlook. Product data sheets and supplier guidance can narrow the options, but a controlled trial on the actual material is more dependable than assumptions. Record the coating thickness, curing conditions, and visible defects, such as peeling at an edge or uneven gloss. These observations make comparisons clearer and help teams discuss results with suppliers.
There is rarely one perfect choice. A harder finish may sacrifice flexibility, while faster drying may complicate application. Requirements can also change as products move from prototype to routine production. Revisit the decision when materials, equipment, or use conditions change. Careful testing takes time, but it can prevent costly rework and disappointing performance. It is not a guarantee. It is a better basis for choosing.
Why Choose the Right Coating Agent for Your Needs?
A coating agent does more than make paint spread smoothly. It helps pigments disperse, improves wetting, controls foam, and supports adhesion. The binder forms the film; additives help that film develop evenly. In water-based coatings, coalescing agents can soften polymer particles so they merge as water evaporates. In reactive systems, curing agents build a stronger network through chemical crosslinking. The choice depends on the surface, application method, drying conditions, and desired finish. A glossy panel and a porous concrete wall rarely need the same formulation.
Film formation is visible in small details: a brush mark that levels, droplets that stop beading, or a dry edge that refuses to blend. ASTM D3359 rates coating adhesion using a tape test, with classifications from 0B to 5B; 5B indicates the strongest classification. That number is useful, but it does not measure every aspect of coating performance. This is where neat theory gets messy. A well-chosen agent can still underperform if the substrate is dusty or the film dries too quickly. Test the actual surface and application conditions, then compare adhesion, appearance, and drying behavior. A small trial panel often reveals more than a datasheet alone.
| Agent or component | Typical chemistry | Core function | Role in film formation | Common applications | Selection considerations |
|---|---|---|---|---|---|
| Film-forming binder | Acrylic, polyurethane, alkyd, epoxy, or other polymer resin | Binds pigments and other ingredients; contributes adhesion, cohesion, and durability | Forms the continuous polymer phase as water or solvent leaves, or as a chemical cure proceeds | Architectural, industrial, wood, and protective coatings | Match resin type to substrate, exposure, flexibility, chemical resistance, and application conditions |
| Surfactant or dispersant | Anionic, nonionic, or polymeric surface-active materials | Helps wet pigments and stabilize particles in the liquid coating | Supports uniform particle distribution before application and reduces settling or flocculation | Waterborne paints, pigment concentrates, and formulated coatings | Check compatibility with the binder, pigment type, pH, and water sensitivity of the dried film |
| Wetting and flow additive | Often silicone-based, fluorine-free surface-active, or polymeric additives | Improves substrate wetting and helps the coating level during application | Promotes smoother spreading and can reduce surface defects such as craters or uneven flow | Spray, roll, brush, and high-gloss coatings | Assess substrate surface energy and test carefully; excessive or incompatible additive may cause recoat or adhesion problems |
| Coalescent | Low-volatility organic liquid used in some waterborne systems | Temporarily softens polymer particles and supports their deformation and fusion | Helps latex particles merge into a continuous film, especially when application temperatures are low | Waterborne latex paints and coatings | Consider minimum film-formation temperature, drying conditions, emissions requirements, and residual odor |
| Rheology modifier | Cellulose ethers, associative polymers, clays, or other thickening materials | Controls viscosity, flow, sag resistance, and suspension stability | Influences how the wet layer is deposited and maintained before the film dries or cures | Interior and exterior paints, textured coatings, and high-build systems | Choose for the application method and desired shear behavior; verify compatibility and storage stability |
| Crosslinker or curing agent | Chemistry varies; examples include isocyanate, epoxy, and amino-resin systems | Creates chemical links between polymer chains or functional groups | Builds a crosslinked network during curing, often improving hardness and resistance | Industrial, floor, automotive, and chemical-resistant coatings | Check mix ratio, pot life, cure temperature and humidity, safety requirements, and target resistance |
| Defoamer | Silicone-based, mineral-oil-based, or polymeric formulations | Controls foam created during manufacture, mixing, or application | Helps prevent bubbles and pinholes from becoming defects in the dried or cured film | Waterborne coatings, pigment dispersions, and high-speed processing | Balance foam control against surface appearance, compatibility, and the risk of cratering |
| Corrosion inhibitor | Examples include phosphate-based pigments and other passivating or barrier-forming materials | Helps protect metal by reducing corrosion reactions or limiting access of water and ions | Functions within the applied coating and, in some systems, at the metal–coating interface | Primers and protective coatings for steel and other metals | Consider metal type, surface preparation, exposure environment, regulatory limits, and the full coating system |
Film formation depends on the complete formulation and application conditions. Validate performance with substrate-specific testing and the coating supplier's technical guidance.
Why Choose the Right Coating Agent for Your Needs?
Start by identifying the exact substrate, not just calling it “metal” or “plastic.” Steel, aluminum, and galvanized surfaces can respond differently to the same coating. Note existing finishes, porosity, surface oils, and preparation limits. A coating may look sound at first, then peel where dust or moisture remained. Small details matter.
Next, map the real exposure: direct sunlight, rain, salt spray, cleaning chemicals, abrasion, or changing temperatures. Include how often exposure occurs and how long surfaces stay wet. Then define the performance you need, such as adhesion, corrosion resistance, flexibility, cleanability, or a particular finish. These goals can conflict. A hard film may resist scratches but crack when a flexible part bends. It is tempting to specify every possible benefit, but that can add cost without solving the actual problem.
Check that the coating suits the substrate and application method, and review preparation and curing requirements. A small test area can reveal poor adhesion, uneven coverage, or slow curing before work expands. Test before scaling. Record the conditions and results; otherwise, comparisons become guesswork. Even a careful plan can miss a detail, especially when site conditions differ from the workshop. Use the test to revise the specification, not merely to confirm an early choice.
Define the substrate, exposure conditions, and required performance.
For steel structures in atmospheric environments, ISO 12944 durability categories describe the expected time to first major maintenance: Low (up to 7 years), Medium (7–15), High (15–25), and Very High (more than 25). The Very High bar is capped at 35 years for display only; the category has no upper limit. These categories are not a coating warranty or a guaranteed service life. Confirm the substrate and corrosivity category, then specify the performance target before selecting a coating system.
Waterborne coatings use water as their main carrier and can suit indoor work where lower solvent odor matters. They clean up readily, but cool, damp conditions may slow drying and affect the finish. A test panel can reveal problems before a full run. Solventborne coatings often flow smoothly and dry reliably across varied shop conditions. Their stronger odor and need for careful ventilation may make application less convenient.
Powder coatings form a durable film when charged particles are heated and fused. They work well on metal parts that can withstand the oven cycle. Plastic components or heat-sensitive assemblies may not be suitable. Watch corners and recesses: electrostatic coverage can be uneven in deep, narrow areas. UV-curable coatings harden quickly under the correct light source, which can shorten handling time. But the light must reach the coated surface; shaded grooves may remain soft. Fast cure helps, but it does not fix poor coverage.
Compare more than cure speed. Consider the substrate, part shape, available equipment, production volume, and the finish you need. In a small trial, check film thickness, adhesion, appearance, and drying time—not just the first impression. A glossy panel can look convincing while hiding weak adhesion. Real shop conditions can also differ from a supplier’s ideal test setup.
A coating can look smooth and still detach under stress. Adhesion testing helps reveal what the eye misses. ASTM D3359 uses a cross-cut or X-cut procedure, depending on the coating and test setup. Its ratings run from 0B to 5B. A 5B result means the cut edges remain intact; lower ratings indicate increasing coating removal.
ISO 2409 also uses cuts and adhesive tape, but its scale runs in the opposite direction: 0 is best, while 5 indicates the greatest flaking. Small difference. Before testing, allow the coating to cure as specified, then make clean, evenly spaced cuts through the film. Grid spacing depends on coating thickness and the test method. Press the tape consistently, remove it as directed, and inspect the exposed grid under good lighting.
Record the substrate, coating thickness, cure time, temperature, and test method with each result. These details make comparisons more meaningful across batches or surfaces. A rough panel or uneven cuts can skew the rating, so repeat the test when results seem surprising. Neither scale predicts every condition in service. Moisture, abrasion, and surface preparation can still change performance. A high rating is useful evidence, not a guarantee.
Why Choose the Right Coating Agent for Your Needs?
A coating’s VOC limit depends on its product category and intended use. Comparing one number across unrelated products can lead to a poor selection. The U.S. EPA’s architectural-coatings standards, listed in 40 CFR Part 59, set different limits by category: flat coatings are limited to 250 grams per liter, while nonflat coatings are limited to 380 grams per liter. These figures apply to specified U.S. federal categories, not every coating agent or market. Small differences matter.
Before choosing, match the product label and technical data sheet to the category used by the relevant rule. Confirm whether VOC content is reported after subtracting water and exempt compounds; otherwise, two figures may not be comparable. Then check applicable state or local requirements, which may set tighter limits. A coating for a metal railing, for example, may not fit an architectural wall-coating category. Check the test method.
VOC performance is only one part of the decision. Application temperature, drying time, substrate preparation, and film thickness affect real-world results. Ask suppliers for current test documentation, and compare products under the same conditions. A lower listed VOC value may look decisive, but it does not prove suitability or durability. I would still verify the category carefully; product descriptions can be vague, and that is easy to overlook.
| Cookie | Duration | Description |
|---|---|---|
| AWSALB | 7 days | AWSALB is a cookie generated by the Application load balancer in the Amazon Web Services. It works slightly different from AWSELB. |
| AWSALBCORS | 7 days | This cookie is used for load balancing services provded by Amazon inorder to optimize the user experience. Amazon has updated the ALB and CLB so that customers can continue to use the CORS request with stickness. |
| cookielawinfo-checkbox-advertisement | 1 year | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Advertisement". |
| cookielawinfo-checkbox-analytics | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytic / Performance". |
| cookielawinfo-checkbox-functional | 11 months | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional". |
| cookielawinfo-checkbox-necessary | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Strictly Necessary". |
| cookielawinfo-checkbox-performance | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance". |
| cookielawinfo-checkbox-preferences | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Preferences." |
| elementor | never | This cookie is used by the website's WordPress theme. It allows the website owner to implement or change the website's content in real-time. |
| viewed_cookie_policy | 11 months | The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data. |
| Cookie | Duration | Description |
|---|---|---|
| CONSENT | 16 years 4 months | These cookies are set via embedded youtube-videos. They register anonymous statistical data on for example how many times the video is displayed and what settings are used for playback.No sensitive data is collected unless you log in to your google account, in that case your choices are linked with your account, for example if you click “like” on a video. |
| _ga | 2 years | This cookie is installed by Google Analytics. The cookie is used to calculate visitor, session, campaign data and keep track of site usage for the site's analytics report. The cookies store information anonymously and assign a randomly generated number to identify unique visitors. |
| _gat_gtag_UA_47200144_1 | 1 minute | This cookie is set by Google and is used to distinguish users. |
| _gid | 1 day | This cookie is installed by Google Analytics. The cookie is used to store information of how visitors use a website and helps in creating an analytics report of how the website is doing. The data collected including the number visitors, the source where they have come from, and the pages visted in an anonymous form. |
| _hjAbsoluteSessionInProgress | session | This cookie is used to count how many times a website has been visited by different visitors. This is done by assigning the visitor an ID, so the visitor does not get registered twice. |
| _hjFirstSeen | 30 minutes | This is set by Hotjar to identify a new user’s first session. It stores a true/false value, indicating whether this was the first time Hotjar saw this user. It is used by Recording filters to identify new user sessions. |
| _hjid | 1 year | This cookie is set by Hotjar. This cookie is set when the customer first lands on a page with the Hotjar script. It is used to persist the random user ID, unique to that site on the browser. This ensures that behavior in subsequent visits to the same site will be attributed to the same user ID. |
| _hjIncludedInPageviewSample | session | This cookie is used to detect whether the user navigation and interactions are included in the website’s data analytics. |
| Cookie | Duration | Description |
|---|---|---|
| IDE | 1 year 24 days | This cookie is used by Google DoubleClick and stores information about how the user uses the website and any other advertisement before visiting the website. This is used to present users with ads that are relevant to them according to the user profile. |
| NID | 6 months | This cookie is used to a profile based on user's interest and display personalized ads to the users. |
| test_cookie | 15 minutes | This cookie is set by doubleclick.net. The purpose of the cookie is to determine if the user's browser supports cookies. |
| VISITOR_INFO1_LIVE | 5 months 27 days | This cookie is set by Youtube it is used to track the information of the embedded YouTube videos on a website. |
| YSC | session | This cookies is set by Youtube and is used to track the views of embedded videos. |
| yt-remote-connected-devices | never | These cookies are set via embedded youtube-videos. |
| yt-remote-device-id | never | These cookies are set via embedded youtube-videos. |
| Cookie | Duration | Description |
|---|---|---|
| qtrans_front_language | 1 year | This cookie is set by qTranslate WordPress plugin. The cookie is used to manage the preferred language of the visitor. |