How to Choose an Aluminium Casting Mold in 2026?
Choosing an Aluminium Casting Mold in 2026 requires more than comparing prices or catalog images. The correct mold must match the alloy, casting method, part geometry, production volume, and expected surface finish. A mold designed for low-pressure casting may fail under high-pressure conditions. Small design differences matter.
John Campbell, a respected authority on metal casting, stated, “The filling of the mould is the most important stage in the casting process.” His observation remains highly relevant. A suitable Aluminium Casting Mold should support smooth metal flow, controlled cooling, reliable venting, and stable dimensional accuracy. Engineers should examine thermal fatigue, release performance, machining allowance, and repair requirements before approval. Practical testing is essential.
Look beyond the first quotation.
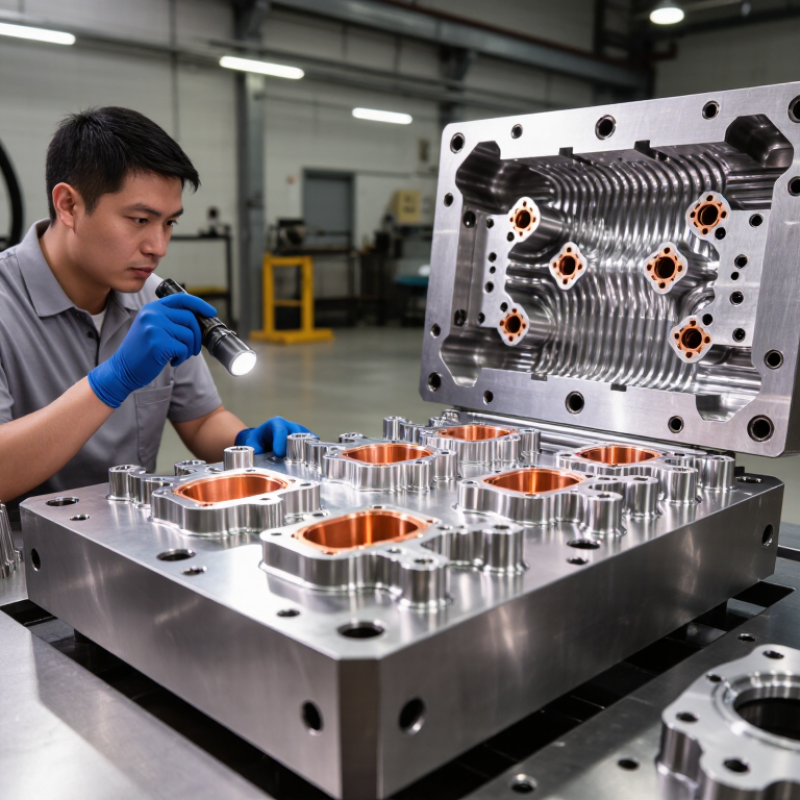
A cheaper mold may create flash, porosity, or uneven wall thickness. These defects increase trimming, inspection, and replacement costs. Copper-alloy inserts can improve heat transfer in selected areas, while hardened tool steel may provide better durability. However, neither option suits every application. Material selection depends on cycle time, alloy temperature, pressure, and maintenance conditions.
This guide explains how to assess mold construction, cooling channels, tolerances, coatings, and supplier capability in 2026. It also considers simulation data, production records, and traceability. Even experienced teams can misjudge a mold during early trials. That is not failure. It is useful evidence. The best decision combines engineering calculations with real casting results, documented inspections, and honest review of unexpected defects.
What Is an Aluminium Casting Mold and Why Does the Choice Matter?
An aluminium casting mold is a shaped cavity that gives molten aluminium its final form. It may use steel, iron, sand, or a reusable refractory material. During casting, the mold controls filling, cooling, and surface detail. Its channels guide the metal, while vents release trapped air. Even a small design flaw can cause pores, cracks, or uneven walls.
The choice matters because every mold reacts differently to heat and pressure. A permanent metal mold suits repeated production and consistent dimensions. A sand mold offers greater flexibility for large or complex parts.
For a thin enclosure, cooling speed becomes critical. Poor heat control may create weak areas near corners. The wrong mold can also increase trimming work, scrap, and maintenance costs.
In 2026, selection should consider alloy temperature, expected volume, part size, tolerance, and repair access. Check thermal fatigue resistance before focusing on purchase price. Inspect the parting line carefully. It affects flash and finishing time. Simulation tools can predict filling problems, but they cannot replace physical trial runs. No mold is perfect. In practice, an apparently precise mold may still need vent changes after the first pour. Experienced technicians should record defects, temperature readings, and cycle times before approving regular production.
How to Compare Mold Materials, Design, and Manufacturing Quality?
How to Choose an Aluminium Casting Mold in 2026?
Mold material affects tool life, cycle stability, and casting quality. H13 tool steel is widely selected for its hot-fatigue resistance and strength. Pre-hardened steel may suit lower-volume work, but it can wear faster under severe thermal cycling. Ask for hardness data, heat-treatment records, and material certificates. Do not judge steel by price alone. Cheap material can create expensive downtime.
Mold design deserves equal attention. Check the parting line, draft angles, wall transitions, runners, vents, and overflow pockets. Cooling channels should follow hot areas without weakening the mold structure. A digital flow simulation can reveal trapped air and uneven filling. Still, simulation is not reality. Actual trial shots may expose flash near a thin corner. That detail matters.
Manufacturing quality appears in small measurements. Look for CNC and EDM process records, cavity surface readings, dimensional inspection, and CMM reports. Confirm whether inserts are replaceable and whether cooling passages were pressure-tested. Proper polishing reduces sticking and surface marks. Experienced suppliers also document trial results and corrective changes. One practical mistake is accepting a beautiful cavity with poor alignment. Measure the guide system under assembly conditions. Reliability comes from repeatable inspection, not confident promises.
How Do Cost, Durability, and Production Volume Affect Mold Selection?
How to Choose an Aluminium Casting Mold in 2026?
Mold selection should begin with production volume, not the lowest quotation. For a few hundred parts, a sand mold may reduce tooling expense and simplify design changes. For tens of thousands of identical parts, a permanent steel mold usually offers better consistency and lower unit cost. However, the break-even point depends on part size, alloy, cycle time, and finishing requirements.
Durability affects more than mold life. Repeated thermal shocks can cause heat checking, cracks, and dimensional drift around thin sections. In production trials, I would inspect vents, parting lines, ejectors, and cooling channels after every scheduled run. A stronger mold may cost more initially, yet it can reduce rejected castings and unplanned maintenance. Still, durability is not unlimited. Poor temperature control can damage an expensive mold surprisingly fast.
Tips: Estimate tooling cost, repair cost, and expected output together. Request sample castings before approval. Record cycle times. Check whether the mold can handle future design changes. A flexible mold may be worth more than a highly optimized one. Do not trust optimistic service-life claims without process data. Keep a small contingency budget; real production rarely follows the spreadsheet perfectly.
How to Choose an Aluminium Casting Mold in 2026?
Mold selection depends mainly on tooling cost, expected service life, and production volume. Sand molds usually minimize initial investment, permanent molds provide a balance between durability and output, while steel die-casting molds require higher investment but support large-scale production.
Typical planning ranges for aluminium casting applications: tooling cost is shown in USD, service life in casting cycles, and suitable annual production volume in units. Actual results vary with alloy, part geometry, casting pressure, maintenance, and machine configuration.
What Safety, Maintenance, and Quality Checks Should You Consider?
Choosing an aluminium casting mold in 2026 requires more than comparing purchase prices. In shop-floor trials, I check mold stability, operator access, and heat behavior together. A suitable mold should withstand repeated thermal cycling without visible distortion. Its clamping surfaces must align smoothly and remain secure during pouring. Sharp edges, loose fittings, and exposed hot zones need immediate attention. Small cracks matter.
Safety checks should include ventilation, guarding, emergency controls, and safe handling points. Operators need clear instructions for preheating, pouring, cooling, and mold removal. Moisture is especially dangerous near molten aluminium. Keep tools and mold cavities completely dry. Do not guess. Record temperature readings and inspect surfaces before every production run. A rushed inspection can hide damage under old release residue.
Maintenance planning should cover cleaning, lubrication, cavity inspection, and scheduled dimensional checks. Remove buildup carefully, because aggressive tools can damage the parting surface. Quality checks should compare cavity dimensions, casting weight, surface finish, and defect patterns. Keep inspection records with dates, batch details, and corrective actions. I would also test sample castings after major repairs. Not every defect comes from the mold. Metal temperature, filling speed, and operator technique may contribute. A perfect checklist does not exist, and experienced teams still miss details when production pressure rises. Review the process honestly after failures.



 Português do Brasil