Choosing the right Uv Drying Solutions starts with the material, not the lamp. A glossy coating on a plastic label may need a different setup from ink on a paper carton. The best system must deliver a reliable cure at the required production speed, without overheating the substrate or wasting energy. More power alone is not a solution.
UV-curing expert Dr. Robert F. Bohn’s published work informs a process-focused approach. A useful paraphrase of that principle is: “Match the lamp, formulation, and production line before chasing maximum power.” This is a paraphrase, not a verbatim quotation. It captures an important point: wavelength, irradiance, exposure time, ink chemistry, and line speed work together. A mismatch can leave a surface tacky, weaken adhesion, or create inconsistent results across a wide web.
Small details matter. Check the substrate’s heat tolerance, measure output at the working distance, and test the actual ink or coating under production conditions. Ask suppliers for measurable performance data and clear maintenance requirements. Then confirm the cure on real samples, not just a demonstration panel.
There is no universal best system. And that is easy to overlook. A compact LED unit may suit a heat-sensitive product, while another application may require a different source or configuration. Treat early trials as evidence, not proof. Record the settings, inspect the finished surface, and revisit the choice when materials or line speeds change.
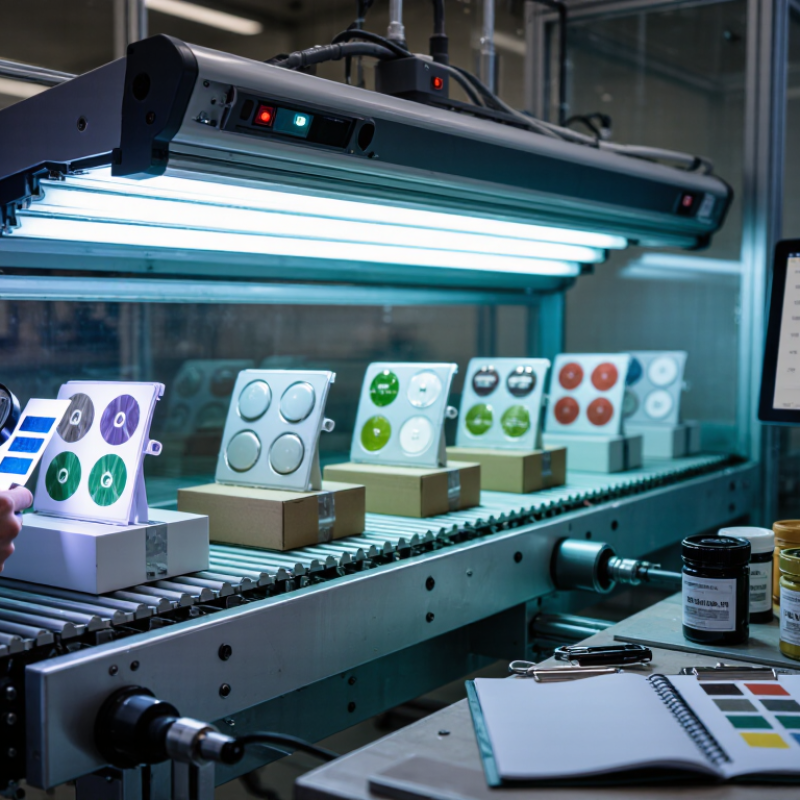
Choosing a UV dryer starts with the actual substrate, not a machine specification sheet. A clear varnish on glass behaves differently from an opaque ink on flexible film. Check whether the material absorbs or reflects the lamp’s output, and test adhesion after curing. Thin plastics can warp under heat; paper may curl when coating coverage is uneven. Small details matter.
The coating determines the wavelength and energy needed for a reliable cure. Ask its supplier for recommended wavelength, irradiance, and dose, then verify them on your production line. MarketsandMarkets’ 2023 UV Curing System Market report estimated the market at USD 3.3 billion in 2023 and projected USD 5.1 billion by 2028. That growth suggests broad adoption, but it does not prove a system suits your job. Line speed, web width, lamp distance, and shaded areas all affect results. I still consider a glossy test panel weak evidence; check adhesion and curing through the full production run.
Match the system to real operating conditions: daily hours, changeovers, cooling needs, and available maintenance time. Record test results for each substrate and coating combination. A slower line may cure well while a faster one leaves tacky edges. That is easy to miss. Start with small trials, inspect the finished surface, and adjust only one process setting at a time.
Choosing a UV system starts with the lamp’s spectrum, not its advertised power. Mercury-vapor lamps emit across a broad band, which can suit coatings containing several photoinitiators. Metal-halide lamps shift that output toward longer wavelengths, helping light reach some pigmented layers. UV LEDs emit narrow bands. RadTech’s UV LED Curing Primer identifies common peaks at 365, 385, 395, and 405 nanometers. Match the peak to the photoinitiator’s absorption range; a mismatch can leave a tacky surface or weak adhesion. Not always obvious.
The curing chemistry matters just as much. Free-radical acrylates cure quickly, but oxygen at the surface can inhibit the reaction, especially on thin films. Cationic epoxy systems are less sensitive to oxygen and may continue curing after exposure, though moisture can interfere. LEDs generally deliver less infrared heat to the workpiece than conventional arc lamps, but the substrate can still warm during repeated passes. Check irradiance and dose at the part, not only at the lamp window. A handheld radiometer helps, but readings depend on wavelength and measurement setup. That detail is easy to miss. Test the actual ink, coating, line speed, and substrate before choosing a curing technology; small trials often reveal uneven edges or shadowed areas that a datasheet cannot.
Compare representative emission wavelengths for common UV sources used in curing and related applications.
How to read this chart: The bars show representative wavelengths, not lamp power, efficiency, or cure speed. Medium-pressure mercury lamps emit multiple wavelengths across a broad spectrum; UV LEDs are available at several discrete peaks, commonly from about 365 to 405 nm. Match the source to the photoinitiator and material, and note that low-pressure mercury at 254 nm is primarily used for disinfection rather than general UV coating cure.
Choosing UV drying equipment starts with the ink, coating, or adhesive chemistry, not the lamp’s headline wattage. Check the material’s response range: a formulation may cure well at 365 nm but respond poorly at 395 nm. Dark pigments and thick films can also limit light penetration. Measure at the surface.
Judge output by both irradiance and delivered dose. Irradiance describes the power reaching the work; dose accumulates during exposure. On a conveyor, higher speed means less exposure time, so more output may be needed to maintain the required dose. But more power is not always better. Heat-sensitive films may warp, while a cured surface can hide a tacky layer underneath. Test with the actual material.
Set conveyor speed after checking lamp distance, reflector condition, and light uniformity across the belt. A reading at one point can miss weak edges. Run a small trial at production speed, then check adhesion, tack, and gloss at the center and edges. Record the wavelength, measured output, and belt speed. One assumption worth questioning: a setup that worked last month may not work today. Dust on a lamp window or sensor can quietly change exposure, so recheck readings after maintenance or when results shift.
Assess Equipment Fit, Safety, and Operating Costs
Choose equipment around the actual material and production line, not a headline wattage. Test the intended ink, coating, or adhesive on the real substrate. Check curing depth, conveyor speed, working width, and available clearance. A test coupon tells more than a brochure. It can also reveal heat damage or uneven curing before installation.
Safety features deserve a close inspection. Look for effective shielding and interlocks that stop UV output when access panels open. Use eye and skin protection specified for the equipment, and consider ventilation when materials release vapors during curing. Do not judge exposure by visible brightness. UV light may be difficult to see. Keep maintenance procedures clear, too; hurried lamp cleaning can create avoidable exposure or downtime.
Purchase price is only part of the cost. Compare energy use, cooling needs, lamp or LED replacement, ventilation, servicing, and production interruptions. Estimate cost per acceptable finished piece across a typical shift. A faster unit may still be costly if it needs frequent maintenance or rejects delicate parts. I would leave room for doubt: one successful sample does not prove stable performance across a full run. Recheck cure quality as speed, material, and equipment age change.
A lamp’s rated output cannot tell you whether a coating will cure on your production line. Test with the actual substrate, coating thickness, and conveyor speed. A thin film on clear glass behaves differently from a heavier layer on a heat-sensitive plastic. Small differences matter.
Measure UV dose with a radiometer suited to the lamp’s wavelength, and record the lamp-to-surface distance. Then check the cured sample for tack, rub resistance, adhesion, and cure through the full film depth. Run several passes at normal line speed, not just one slow test. Not always. A surface can feel dry while material underneath remains undercured.
Keep notes on temperature, lamp age, and sample position; edges may receive less exposure than the center. I would not treat one successful pass as proof, even when the finish looks clean. That shortcut is tempting under schedule pressure. Test under realistic operating conditions, and include the least favorable setup you expect to use. A test coupon is useful, but it cannot reproduce every variation in a full production run. If results shift between samples, investigate the process before selecting equipment.
| Cookie | Duration | Description |
|---|---|---|
| AWSALB | 7 days | AWSALB is a cookie generated by the Application load balancer in the Amazon Web Services. It works slightly different from AWSELB. |
| AWSALBCORS | 7 days | This cookie is used for load balancing services provded by Amazon inorder to optimize the user experience. Amazon has updated the ALB and CLB so that customers can continue to use the CORS request with stickness. |
| cookielawinfo-checkbox-advertisement | 1 year | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Advertisement". |
| cookielawinfo-checkbox-analytics | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytic / Performance". |
| cookielawinfo-checkbox-functional | 11 months | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional". |
| cookielawinfo-checkbox-necessary | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Strictly Necessary". |
| cookielawinfo-checkbox-performance | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance". |
| cookielawinfo-checkbox-preferences | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Preferences." |
| elementor | never | This cookie is used by the website's WordPress theme. It allows the website owner to implement or change the website's content in real-time. |
| viewed_cookie_policy | 11 months | The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data. |
| Cookie | Duration | Description |
|---|---|---|
| CONSENT | 16 years 4 months | These cookies are set via embedded youtube-videos. They register anonymous statistical data on for example how many times the video is displayed and what settings are used for playback.No sensitive data is collected unless you log in to your google account, in that case your choices are linked with your account, for example if you click “like” on a video. |
| _ga | 2 years | This cookie is installed by Google Analytics. The cookie is used to calculate visitor, session, campaign data and keep track of site usage for the site's analytics report. The cookies store information anonymously and assign a randomly generated number to identify unique visitors. |
| _gat_gtag_UA_47200144_1 | 1 minute | This cookie is set by Google and is used to distinguish users. |
| _gid | 1 day | This cookie is installed by Google Analytics. The cookie is used to store information of how visitors use a website and helps in creating an analytics report of how the website is doing. The data collected including the number visitors, the source where they have come from, and the pages visted in an anonymous form. |
| _hjAbsoluteSessionInProgress | session | This cookie is used to count how many times a website has been visited by different visitors. This is done by assigning the visitor an ID, so the visitor does not get registered twice. |
| _hjFirstSeen | 30 minutes | This is set by Hotjar to identify a new user’s first session. It stores a true/false value, indicating whether this was the first time Hotjar saw this user. It is used by Recording filters to identify new user sessions. |
| _hjid | 1 year | This cookie is set by Hotjar. This cookie is set when the customer first lands on a page with the Hotjar script. It is used to persist the random user ID, unique to that site on the browser. This ensures that behavior in subsequent visits to the same site will be attributed to the same user ID. |
| _hjIncludedInPageviewSample | session | This cookie is used to detect whether the user navigation and interactions are included in the website’s data analytics. |
| Cookie | Duration | Description |
|---|---|---|
| IDE | 1 year 24 days | This cookie is used by Google DoubleClick and stores information about how the user uses the website and any other advertisement before visiting the website. This is used to present users with ads that are relevant to them according to the user profile. |
| NID | 6 months | This cookie is used to a profile based on user's interest and display personalized ads to the users. |
| test_cookie | 15 minutes | This cookie is set by doubleclick.net. The purpose of the cookie is to determine if the user's browser supports cookies. |
| VISITOR_INFO1_LIVE | 5 months 27 days | This cookie is set by Youtube it is used to track the information of the embedded YouTube videos on a website. |
| YSC | session | This cookies is set by Youtube and is used to track the views of embedded videos. |
| yt-remote-connected-devices | never | These cookies are set via embedded youtube-videos. |
| yt-remote-device-id | never | These cookies are set via embedded youtube-videos. |
| Cookie | Duration | Description |
|---|---|---|
| qtrans_front_language | 1 year | This cookie is set by qTranslate WordPress plugin. The cookie is used to manage the preferred language of the visitor. |