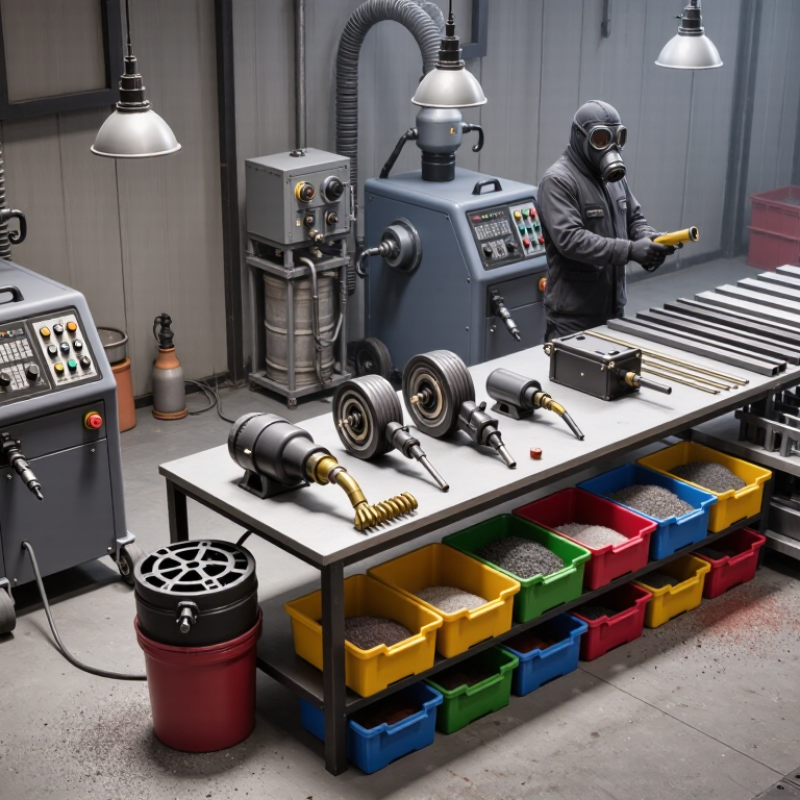
Choosing Shot Blasting Tools is not simply a matter of buying the most powerful machine. The right setup depends on the workpiece, abrasive, finish target, and available workspace. A small workshop cleaning brackets has different needs from a production line treating large steel plates. The distinction matters.
Look at the full process, not one specification. Check the blast machine’s capacity, nozzle or wheel design, abrasive compatibility, dust collection, and replacement-part availability. Then compare these details with your daily workload. A tool that performs well for short jobs may struggle during continuous operation. That can mean uneven coverage, extra cleanup, or avoidable wear.
Safety and measurement deserve equal attention. Confirm that the system supports effective dust control and that operators can follow the manufacturer’s instructions. Test the equipment on a representative sample, then inspect the surface under consistent lighting. A clean-looking part is not always a uniformly prepared part. Small differences matter.
An expert quotation needs a verifiable source. Since none was provided, this introduction does not invent one or attribute words to a named specialist. That is worth acknowledging. In the guide ahead, we will compare tool types, abrasive choices, performance factors, and maintenance needs. The goal is practical: choose Shot Blasting Tools that match the job, deliver repeatable results, and make sense for your workshop—not just the sales sheet.
Before choosing shot blasting tools, set the required cleanliness level. ISO 8501-1 defines Sa 2½ as very thorough blast-cleaning. Without magnification, the surface must be free of visible oil, grease, and dirt. Mill scale, rust, coatings, and other foreign matter must be removed almost entirely. Only slight stains may remain, often as faint spots or stripes. That distinction matters.
Sa 2½ does not prescribe one abrasive or a particular surface profile. Select the abrasive, nozzle, and air supply to suit the metal, coating specification, and work area. For example, a narrow steel corner may need a smaller nozzle and careful passes, while a broad plate calls for steady coverage. Keep dust extraction effective; poor visibility makes missed patches more likely. Corners and weld toes are easy to overlook, so inspect them closely.
Judge cleanliness under consistent lighting and viewing conditions, using ISO 8501-1’s visual descriptions as the reference. A bright surface can still retain contamination. Also, cleanliness and surface profile are different checks: Sa 2½ describes visual cleanliness, while profile needs its own suitable measurement. If the result falls short, adjust the blasting setup and reassess rather than assuming a longer pass will fix everything.
| Selection or Inspection Factor | Practical Guidance | How to Verify |
|---|---|---|
| Cleanliness target | Specify the required preparation grade before choosing equipment. ISO 8501-1 Sa 2½ is “very thorough blast-cleaning”: visible oil, grease and dirt must be removed, and mill scale, rust, paint coatings and foreign matter must be removed to the extent that only slight traces remain as spots or stripes. | Compare the prepared surface with the applicable ISO 8501-1 visual reference photographs under suitable lighting. |
| Existing surface condition | Assess the steel’s initial rust and coating condition, the type and thickness of existing coatings, and whether the surface has pits or difficult-to-reach areas. These factors influence the preparation effort and tool setup. | Record the initial condition and inspect representative areas before production blasting. |
| Abrasive shape | Round steel shot is commonly used where a more peening action is desired. Angular steel grit cuts more aggressively and can help remove tightly adherent scale or coatings. The result depends on the abrasive, equipment, operating conditions and substrate. | Run a trial on representative steel and check cleanliness, surface profile and abrasive condition. |
| Abrasive size and hardness | Choose size and hardness to suit the contaminant, required profile, substrate and blasting equipment. Larger or harder particles can increase impact energy, but the correct choice must be established for the application rather than assumed from cleanliness grade alone. | Check the supplier’s abrasive specification and confirm results with a production trial. |
| Surface profile | Sa 2½ describes visual cleanliness; it does not specify a surface-profile value. Set a separate profile requirement based on the coating system and project specification. | Measure profile using an appropriate method, such as a replica tape or a suitable surface-profile instrument, in accordance with the project procedure. |
| Soluble salts and other invisible contaminants | A visual cleanliness grade does not establish that soluble salts or other invisible contaminants are absent. Include separate limits and testing when required by the coating specification or project requirements. | Use the specified field test method and acceptance limit; do not treat visual inspection as a salt test. |
| Equipment capacity and coverage | Match the blasting system’s capacity and working pattern to the component size, geometry and required production rate. Confirm that edges, welds, recesses and other difficult areas can be reached consistently. | Inspect both accessible and difficult-to-reach areas during the trial and after blasting. |
| Operating controls | Follow the equipment and abrasive supplier’s operating guidance. Keep the abrasive clean and in suitable condition, and maintain consistent settings and technique to help achieve repeatable results. | Check operating records, abrasive condition and prepared surfaces at defined intervals. |
| Final acceptance | Accept the work against the specified cleanliness grade and any separate requirements for profile, salts, dust or coating readiness. Protect prepared steel from contamination and flash rust before coating. | Document visual inspection and all required supplementary measurements before coating begins. |
Note: ISO 8501-1 visual preparation grades and surface-profile requirements are separate checks. Always follow the project specification and the coating manufacturer’s requirements.
Choose the abrasive by the surface profile, substrate, and cleanup plan—not by price alone. ISO 11124 covers metallic abrasives, including cast-steel shot and grit; ISO 11126 covers non-metallic types, including garnet and furnace slag. These standards classify abrasive properties and help buyers compare technical specifications. Small details matter. Shot’s rounded particles suit repeated impact, while angular grit cuts rust and scale more aggressively.
For a steel beam needing a deep profile, compare metallic grit size and hardness with the coating specification. For a thin panel, excessive impact can distort the surface. Non-metallic media may suit jobs where steel contamination is undesirable, but mineral composition and dust still require attention. Request the product’s ISO classification, particle-size distribution, and batch test certificate. Then test a small area. A certificate alone cannot predict every result.
Review the safety data sheet, especially when mineral abrasives may contain crystalline silica. The NIOSH Pocket Guide to Chemical Hazards lists a recommended exposure limit of 0.05 mg/m³ for respirable crystalline silica, averaged over a work shift. That figure is a useful control benchmark, not proof that a particular abrasive is safe. Check ventilation, dust collection, and spent-media handling at the actual site. A technically correct choice can still disappoint when the profile target or recovery method was guessed.
For a controlled surface profile, choose abrasive by particle shape and SAE J444 size—not by size alone. Round steel shot mainly cleans and peens; angular steel grit cuts the surface and creates a sharper anchor pattern. SAE J444 classifies cast steel shot and grit through sieve-based size designations. For example, S330 shot is nominally about 0.033 inch (0.84 mm). Check the current standard and the supplier’s sieve analysis before ordering.
A size table is a starting point, not a promise. The final profile also depends on blast pressure, nozzle distance, angle, exposure time, and the steel itself. A finer abrasive may suit a shallow profile, while larger or angular media can produce a more pronounced texture. Too aggressive? You may remove more substrate than intended. Test a small area first.
Measure the result. ASTM D4417 describes field methods for measuring the profile of blast-cleaned steel, including replica tape and depth micrometers. Use the method specified for the project, then compare readings with the required profile range. A clean test panel helps reveal whether the media choice is working. I would still verify the result on the actual workpiece; settings that perform well on a sample can shift on a larger, uneven surface.
For air-blast equipment, 100 psi (6.9 bar) at the nozzle is a common benchmark—not a universal setting. Measure pressure while blasting, with the trigger open. A static gauge can look healthy while air flows poorly through a long hose, small couplings, or a clogged filter. The nozzle may then receive less pressure than the compressor gauge suggests. That difference matters: the abrasive stream can lose speed, leaving patches of coating on a steel plate.
Check the whole air path. The U.S. Department of Energy’s Improving Compressed Air System Performance guide recommends keeping distribution-system pressure drop below 10% of compressor discharge pressure. Treat this as a system diagnostic, not a blast-nozzle specification. At 100 psi discharge, a 10 psi drop would already leave only 90 psi before other losses. Record nozzle pressure under load, hose length, and abrasive flow. Retest after changing any of them.
Tips: Use a pressure-rated gauge close to the nozzle, inspect couplings for leaks, and compare readings during steady blasting. A worn nozzle can increase air demand; pressure alone will not reveal the whole problem. I would not chase 100 psi blindly. The right setup depends on the surface, abrasive, and finish required.
Choosing blasting equipment is also a dust-control decision. OSHA’s respirable crystalline silica PEL is 50 μg/m³ as an eight-hour time-weighted average. Staying below it cannot be assumed from a tool’s specifications. Abrasive choice, the workpiece, ventilation, and operator position all matter.
Wheel blasting propels abrasive inside an enclosed machine, which can make dust capture more manageable when seals and extraction systems work properly. Air blasting is more flexible for large structures and hard-to-reach surfaces, but compressed air can spread dust beyond the immediate work area. Enclosures, effective local exhaust, and suitable respiratory protection may be needed. Avoid silica sand as blasting abrasive; dust can also come from the material being cleaned.
Check the actual setup. Look for damaged seals, clogged filters, and dust escaping when the enclosure opens. Keep workers out of the plume, and use exposure monitoring to verify control measures under real operating conditions. A clean-looking floor proves little. I would not treat a “low-dust” label as evidence of compliance; that assumption is easy to make, and hard to defend. Review results with a qualified safety professional, especially when surfaces or abrasives change.
| Cookie | Duration | Description |
|---|---|---|
| AWSALB | 7 days | AWSALB is a cookie generated by the Application load balancer in the Amazon Web Services. It works slightly different from AWSELB. |
| AWSALBCORS | 7 days | This cookie is used for load balancing services provded by Amazon inorder to optimize the user experience. Amazon has updated the ALB and CLB so that customers can continue to use the CORS request with stickness. |
| cookielawinfo-checkbox-advertisement | 1 year | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Advertisement". |
| cookielawinfo-checkbox-analytics | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytic / Performance". |
| cookielawinfo-checkbox-functional | 11 months | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional". |
| cookielawinfo-checkbox-necessary | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Strictly Necessary". |
| cookielawinfo-checkbox-performance | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance". |
| cookielawinfo-checkbox-preferences | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Preferences." |
| elementor | never | This cookie is used by the website's WordPress theme. It allows the website owner to implement or change the website's content in real-time. |
| viewed_cookie_policy | 11 months | The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data. |
| Cookie | Duration | Description |
|---|---|---|
| CONSENT | 16 years 4 months | These cookies are set via embedded youtube-videos. They register anonymous statistical data on for example how many times the video is displayed and what settings are used for playback.No sensitive data is collected unless you log in to your google account, in that case your choices are linked with your account, for example if you click “like” on a video. |
| _ga | 2 years | This cookie is installed by Google Analytics. The cookie is used to calculate visitor, session, campaign data and keep track of site usage for the site's analytics report. The cookies store information anonymously and assign a randomly generated number to identify unique visitors. |
| _gat_gtag_UA_47200144_1 | 1 minute | This cookie is set by Google and is used to distinguish users. |
| _gid | 1 day | This cookie is installed by Google Analytics. The cookie is used to store information of how visitors use a website and helps in creating an analytics report of how the website is doing. The data collected including the number visitors, the source where they have come from, and the pages visted in an anonymous form. |
| _hjAbsoluteSessionInProgress | session | This cookie is used to count how many times a website has been visited by different visitors. This is done by assigning the visitor an ID, so the visitor does not get registered twice. |
| _hjFirstSeen | 30 minutes | This is set by Hotjar to identify a new user’s first session. It stores a true/false value, indicating whether this was the first time Hotjar saw this user. It is used by Recording filters to identify new user sessions. |
| _hjid | 1 year | This cookie is set by Hotjar. This cookie is set when the customer first lands on a page with the Hotjar script. It is used to persist the random user ID, unique to that site on the browser. This ensures that behavior in subsequent visits to the same site will be attributed to the same user ID. |
| _hjIncludedInPageviewSample | session | This cookie is used to detect whether the user navigation and interactions are included in the website’s data analytics. |
| Cookie | Duration | Description |
|---|---|---|
| IDE | 1 year 24 days | This cookie is used by Google DoubleClick and stores information about how the user uses the website and any other advertisement before visiting the website. This is used to present users with ads that are relevant to them according to the user profile. |
| NID | 6 months | This cookie is used to a profile based on user's interest and display personalized ads to the users. |
| test_cookie | 15 minutes | This cookie is set by doubleclick.net. The purpose of the cookie is to determine if the user's browser supports cookies. |
| VISITOR_INFO1_LIVE | 5 months 27 days | This cookie is set by Youtube it is used to track the information of the embedded YouTube videos on a website. |
| YSC | session | This cookies is set by Youtube and is used to track the views of embedded videos. |
| yt-remote-connected-devices | never | These cookies are set via embedded youtube-videos. |
| yt-remote-device-id | never | These cookies are set via embedded youtube-videos. |
| Cookie | Duration | Description |
|---|---|---|
| qtrans_front_language | 1 year | This cookie is set by qTranslate WordPress plugin. The cookie is used to manage the preferred language of the visitor. |