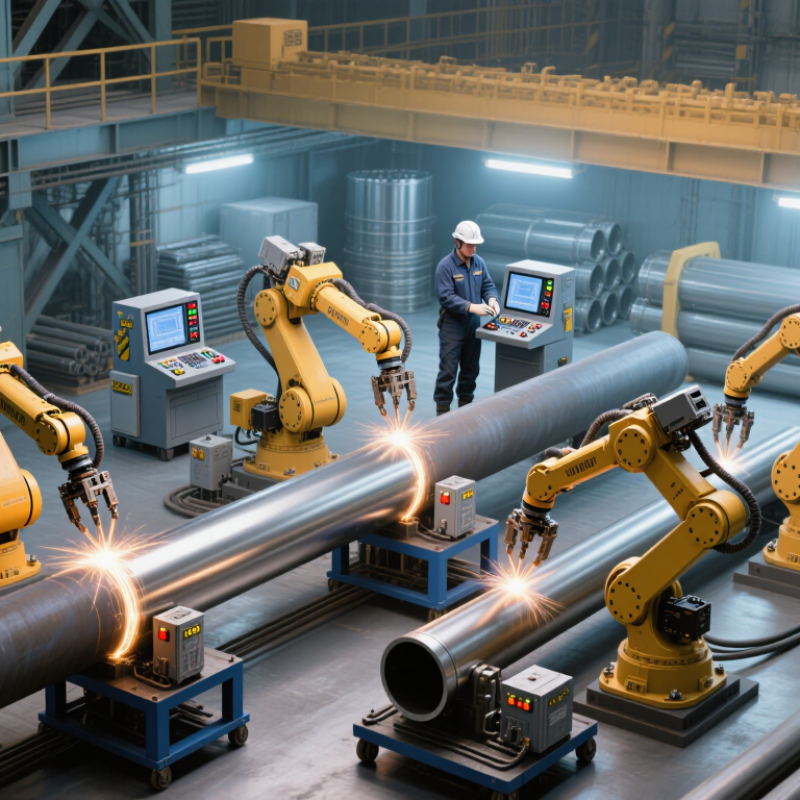
Choosing an Auto Pipe Welding Machine in 2026 requires more than comparing amperage, price, and advertised travel speed. The machine must fit pipe diameter, wall thickness, alloy, joint design, production volume, and site conditions. A workshop welding stainless steel spools needs different control precision than a field crew joining carbon-steel lines. Small details matter, including torch clearance, wire-feeder stability, heat-input control, and how quickly operators can correct arc deviations.
Industry data shows why this decision deserves careful review. The International Federation of Robotics reported 541,302 industrial robots installed worldwide in 2023, confirming broader manufacturing investment in automation. MarketsandMarkets also projects continued growth in the global welding equipment market through 2028. However, these reports cover wider equipment categories, not Auto Pipe Welding machines alone. That distinction matters. Buyers should avoid treating broad market growth as proof that every automated system will improve their operation.
Welding metallurgist John C. Lippold has emphasized a practical principle: “Successful welding depends on controlling the process variables, not simply selecting advanced equipment.” His point remains relevant when comparing orbital systems, robotic manipulators, and integrated pipe stations. A reliable evaluation should examine weld repeatability, documented procedure support, operator training, maintenance access, data logging, and compatibility with qualified welding procedures. Ask for real production samples. Inspect the root profile. Review defect records. The choice is practical.
Some specifications can look impressive on paper but disappoint beside a hot pipe, limited access, or inconsistent fit-up. This guide explains how to compare machines realistically, identify hidden costs, and select equipment that supports safe, repeatable, and auditable welding performance.
How to Choose an Auto Pipe Welding Machine in 2026?
Pipe size determines machine capacity, clamping range, and torch travel. Record outside diameter, inside diameter, and joint access before comparing equipment. Measure twice. A machine designed for 2-inch pipe may struggle with 24-inch sections. Large-diameter work also needs stronger alignment control and steadier rotation. The International Energy Agency’s World Energy Investment 2024 report expects global energy investment to exceed 3 trillion dollars in 2024. That growth will increase demand for consistent pipeline welding, but project specifications still control the purchase.
Wall thickness affects heat input, pass planning, and welding speed. Thin-wall stainless pipe can burn through under excessive current. Thick carbon-steel walls may require preheating, multiple passes, and slower travel. Select a system that records current, voltage, travel speed, and interpass temperature. ASME Boiler and Pressure Vessel Code Section IX and ISO 15614-1 provide useful qualification frameworks. They do not replace a project-specific welding procedure. That assumption fails.
Material selection matters just as much. The World Steel Association reported about 1.89 billion tonnes of crude steel production in 2023, showing the scale and variety of steel applications. Carbon steel, stainless steel, duplex steel, and nickel alloys require different shielding gases, filler metals, and thermal limits. In field reviews, teams often specify diameter but overlook wall variation. Check the complete thickness range, material certificates, joint design, and allowable heat input. A short trial weld can expose poor fit-up, awkward torch access, or unstable arc behavior before production begins.
Use the following planning matrix to match pipe dimensions, materials, welding processes, and automation requirements. Actual machine capacity should be verified against the selected welding procedure specification (WPS), applicable code, joint design, and production conditions.
| Application Category | Typical Outside Diameter | Typical Wall Thickness | Common Pipe Materials | Recommended Automated Process | Preferred Machine Configuration | Important Selection Factors |
|---|---|---|---|---|---|---|
| Small-diameter process tubing | 6–60 mm (0.24–2.36 in) | 1–4 mm (0.04–0.16 in) | Austenitic stainless steel, nickel alloys, titanium | Orbital GTAW/TIG with inert-gas shielding | Compact orbital power source with automatic torch rotation, programmable current, and closed-loop travel control | Low-current stability, precise arc control, purge-gas monitoring, and repeatable heat input |
| General utility and fabrication pipe | 60–168 mm (2.36–6.63 in) | 3–12 mm (0.12–0.47 in) | Carbon steel, low-alloy steel, stainless steel | Orbital GTAW for root passes; GMAW or FCAW for fill and cap passes | Modular positioner or rotating-chuck system with multi-process power capability | Workholding range, torch access, wire-feed synchronization, and easy parameter recipe changes |
| Medium-diameter pipeline joints | 168–406 mm (6.63–16 in) | 6–20 mm (0.24–0.79 in) | Carbon steel and low-alloy pipeline steel | Mechanized GMAW, pulsed GMAW, or narrow-gap GTAW/GMAW | Track-mounted or band-mounted welding carriage with automatic seam tracking | Carriage stability, root-gap tolerance, arc-voltage control, interpass-temperature control, and weather protection |
| Large-diameter transmission pipe | 406–1,219 mm (16–48 in) | 8–25 mm (0.31–0.98 in) | High-strength carbon and low-alloy steel | Mechanized pulsed GMAW, tandem GMAW, or hybrid multi-process welding | Multi-head internal and external welding system with synchronized controls | Deposition rate, synchronized travel speed, joint tracking, preheat management, and data logging |
| Heavy-wall pressure pipe | 114–610 mm (4.5–24 in) | 20–60 mm (0.79–2.36 in) | Carbon steel, low-alloy steel, creep-resistant alloy steel | Narrow-gap GTAW for root; GMAW, FCAW, or SAW for subsequent passes | Multi-pass CNC welding system with oscillation, layer control, and pass sequencing | High duty cycle, thermal management, narrow-gap torch geometry, layer alignment, and full weld traceability |
| Stainless and corrosion-resistant pipe | 25–406 mm (1–16 in) | 2–16 mm (0.08–0.63 in) | Austenitic stainless steel, duplex stainless steel, nickel-based alloys | Orbital GTAW, pulsed GTAW, or controlled-pulse GMAW | Precision orbital system with programmable pulse waveform and internal purge control | Heat-input limits, purge quality, interpass temperature, shielding coverage, and corrosion-resistance requirements |
| Aluminum and lightweight alloy pipe | 50–406 mm (2–16 in) | 3–12 mm (0.12–0.47 in) | Wrought aluminum alloys and selected aluminum-magnesium alloys | AC GTAW/TIG or pulsed GMAW with suitable aluminum wire | Rotary positioner with AC-capable power source, high-frequency arc start, and wire-feed control | Oxide cleaning action, thermal distortion control, wire feeding, torch cooling, and cleanliness procedures |
| High-production shop fabrication | 168–914 mm (6.63–36 in) | 6–30 mm (0.24–1.18 in) | Carbon steel, stainless steel, and low-alloy steel | Mechanized GMAW, FCAW, SAW, or combined multi-process welding | Automated welding cell with powered rotator, seam tracking, fume extraction, and production monitoring | Cycle time, duty cycle, loading method, operator safety, fixture repeatability, and compatibility with existing WPS procedures |
Note: The dimensions and process combinations shown are typical engineering planning ranges rather than universal machine limits. Final selection should be validated through procedure qualification, sample welds, inspection requirements, and the exact pipe grade and joint design.
Choosing an automatic pipe welding machine in 2026 starts with weld data, not catalog speed. The AWS Welding Handbook identifies current, voltage, electrode size, shielding gas, and travel speed as linked variables. For a 6 mm carbon-steel pipe wall, a qualified GTAW root may begin near 90–130 A, while mechanized GMAW fill passes may use 160–230 A. These are starting ranges, not universal settings. Pipe position, joint gap, and heat loss can change them quickly.
Measure the actual arc values during trials. Heat input can be estimated as Q = 60VI ÷ 1,000S, where V is voltage, I is amperage, and S is travel speed in millimeters per minute. At 12 V, 100 A, and 120 mm/min, the calculated input is 0.60 kJ/mm before efficiency correction. Compare this result with the qualified WPS and PQR requirements under ASME BPVC Section IX or API 1104. Keep the machine’s working range above the target, but avoid buying excessive capacity.
Travel speed matters most.
A machine running 300 mm/min may look efficient, yet it can produce poor sidewall fusion if amperage is too low. The opposite problem is also common: excessive heat causes distortion, wider beads, or unacceptable hardness. I have seen clean-looking test coupons fail after radiographic inspection. That is why production logs should record current, voltage, speed, interpass temperature, and defect findings. Published data helps, but shop trials remain necessary. Surface condition and operator setup can quietly invalidate a perfect spreadsheet.
Match the machine’s current capacity and wire or electrode delivery system to the welding process. The chart shows representative setpoints for carbon-steel pipe welding: GTAW is commonly used for controlled root passes, while SMAW, GMAW, and FCAW support higher deposition rates for fill and cap passes.
Values are typical engineering reference points for procedure development on medium-wall pipe and must be qualified against pipe diameter, wall thickness, welding position, joint design, shielding gas, consumable classification, and applicable welding codes.
When selecting an automatic pipe welding machine, verify procedure qualification before comparing speed or price. The equipment must support welding variables listed in your qualified WPS and PQR. Check current, voltage, travel speed, wire feed, arc length, and shielding gas control. These settings must remain stable during long circumferential welds. Small deviations can affect penetration and heat input.
Ask for documented evidence that your proposed process aligns with ASME Section IX and ISO 15614-1. The machine itself is not automatically qualified because it has precise controls. Your welding procedure requires suitable test records, material groups, thickness ranges, joint designs, and position limits. Confirm whether the software records actual values, not only programmed values. Review calibration certificates for power sources, sensors, and monitoring devices. Request sample data from a pipe weld, including purge pressure and interpass temperature.
Test it with your own pipe material.
A practical trial should reproduce the intended diameter, wall thickness, joint preparation, and consumables. Then compare the results with the qualified procedure. I would not rely on a supplier’s general compliance statement. It may omit important variables. One overlooked detail can force a new qualification test.
Also examine data export, alarm history, and operator access controls. These features support traceability during audits and help identify unstable welds.
The best choice is not always the fastest machine; it is the one that consistently produces qualified, documented results.
Choosing an automatic pipe welding machine requires more than checking its maximum speed. In 2026, evaluate how accurately it maintains travel speed, torch alignment, and arc distance. A range of 0.5–2.0 m/min supports different pipe diameters and wall thicknesses. Lower speeds help control heat on thin sections. Higher speeds can improve productivity on stable, repeatable joints. Ask for test welds using your actual pipe material and joint design.
Tips: Check accuracy at both speed extremes. Measure the completed weld, not only the machine display. Confirm whether speed changes under load. Duty cycle also matters during long production runs. Review the rated duty cycle at your expected current, ambient temperature, and welding duration. A machine rated for continuous work may still require cooling pauses at demanding settings.
In practical shop trials, fit-up variation often affects results more than advertised precision. Small gaps can change penetration and bead shape. I would not choose a machine from a polished demonstration alone. Inspect its control response, clamp stability, and recovery after stopping. Perfect repeatability is unlikely when operators prepare joints differently. That weakness should be tested honestly. A reliable system records welding parameters and supports simple adjustments without hiding important settings.
Choosing an automatic pipe welding machine in 2026 requires more than comparing welding speed. Safety must be verified at the workcell. Check guarding, interlocked doors, emergency stops, fume extraction, and purge-gas monitoring. These controls should support documented risk assessments and relevant machinery standards. A practical trial should include cramped access, hot surfaces, and imperfect pipe fit-up. Real workshops are rarely perfect.
Digital controls should create repeatable weld recipes, record current, voltage, travel speed, and gas flow, and protect approved settings from casual changes. The IFR World Robotics 2024 report recorded 541,302 industrial robots installed globally in 2023, a 10% annual increase. Automation is expanding, but a touchscreen alone is not intelligence. Ask whether operators can export usable data, trace each weld, and diagnose alarms without calling an engineer. Deloitte’s 2024 Smart Manufacturing and Operations Survey found that 86% of manufacturers consider smart manufacturing important to future competitiveness.
Service support can decide uptime. Confirm spare-part availability, remote diagnostics, calibration procedures, training, and a written response-time commitment. Calculate total cost across five years. Include fixtures, consumables, shielding gas, programming, energy, inspections, software, downtime, scrap, and technician travel. A low purchase price can still become expensive. I would not trust optimistic payback figures without production records. Measure cycle time on your own pipe sizes. Review rejected welds. Then challenge the assumptions again.
| Cookie | Duration | Description |
|---|---|---|
| AWSALB | 7 days | AWSALB is a cookie generated by the Application load balancer in the Amazon Web Services. It works slightly different from AWSELB. |
| AWSALBCORS | 7 days | This cookie is used for load balancing services provded by Amazon inorder to optimize the user experience. Amazon has updated the ALB and CLB so that customers can continue to use the CORS request with stickness. |
| cookielawinfo-checkbox-advertisement | 1 year | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Advertisement". |
| cookielawinfo-checkbox-analytics | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytic / Performance". |
| cookielawinfo-checkbox-functional | 11 months | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional". |
| cookielawinfo-checkbox-necessary | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Strictly Necessary". |
| cookielawinfo-checkbox-performance | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance". |
| cookielawinfo-checkbox-preferences | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Preferences." |
| elementor | never | This cookie is used by the website's WordPress theme. It allows the website owner to implement or change the website's content in real-time. |
| viewed_cookie_policy | 11 months | The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data. |
| Cookie | Duration | Description |
|---|---|---|
| CONSENT | 16 years 4 months | These cookies are set via embedded youtube-videos. They register anonymous statistical data on for example how many times the video is displayed and what settings are used for playback.No sensitive data is collected unless you log in to your google account, in that case your choices are linked with your account, for example if you click “like” on a video. |
| _ga | 2 years | This cookie is installed by Google Analytics. The cookie is used to calculate visitor, session, campaign data and keep track of site usage for the site's analytics report. The cookies store information anonymously and assign a randomly generated number to identify unique visitors. |
| _gat_gtag_UA_47200144_1 | 1 minute | This cookie is set by Google and is used to distinguish users. |
| _gid | 1 day | This cookie is installed by Google Analytics. The cookie is used to store information of how visitors use a website and helps in creating an analytics report of how the website is doing. The data collected including the number visitors, the source where they have come from, and the pages visted in an anonymous form. |
| _hjAbsoluteSessionInProgress | session | This cookie is used to count how many times a website has been visited by different visitors. This is done by assigning the visitor an ID, so the visitor does not get registered twice. |
| _hjFirstSeen | 30 minutes | This is set by Hotjar to identify a new user’s first session. It stores a true/false value, indicating whether this was the first time Hotjar saw this user. It is used by Recording filters to identify new user sessions. |
| _hjid | 1 year | This cookie is set by Hotjar. This cookie is set when the customer first lands on a page with the Hotjar script. It is used to persist the random user ID, unique to that site on the browser. This ensures that behavior in subsequent visits to the same site will be attributed to the same user ID. |
| _hjIncludedInPageviewSample | session | This cookie is used to detect whether the user navigation and interactions are included in the website’s data analytics. |
| Cookie | Duration | Description |
|---|---|---|
| IDE | 1 year 24 days | This cookie is used by Google DoubleClick and stores information about how the user uses the website and any other advertisement before visiting the website. This is used to present users with ads that are relevant to them according to the user profile. |
| NID | 6 months | This cookie is used to a profile based on user's interest and display personalized ads to the users. |
| test_cookie | 15 minutes | This cookie is set by doubleclick.net. The purpose of the cookie is to determine if the user's browser supports cookies. |
| VISITOR_INFO1_LIVE | 5 months 27 days | This cookie is set by Youtube it is used to track the information of the embedded YouTube videos on a website. |
| YSC | session | This cookies is set by Youtube and is used to track the views of embedded videos. |
| yt-remote-connected-devices | never | These cookies are set via embedded youtube-videos. |
| yt-remote-device-id | never | These cookies are set via embedded youtube-videos. |
| Cookie | Duration | Description |
|---|---|---|
| qtrans_front_language | 1 year | This cookie is set by qTranslate WordPress plugin. The cookie is used to manage the preferred language of the visitor. |