Choosing a Rubber Automatic Cutting machine in 2026 is less about chasing the fastest cycle time and more about matching the machine to your actual production work. Rubber sheets, rolls, and molded components behave differently under a blade. A setup that cuts thin gasket stock cleanly may struggle with thick, elastic material. That difference matters on the factory floor.
Look closely at material thickness, cutting accuracy, usable table area, blade options, and software workflow. Ask suppliers to run samples using your own rubber, not just a standard demonstration sheet. Watch the cut edge. Check for stretching, burrs, and material movement. Small defects can become costly when repeated across a full shift. The published speed is only part of the story.
A reliable guide should also include a verifiable expert voice. No sourced expert quotation was provided for this topic, so attributing a made-up statement to a named specialist would weaken trust. Instead, use this practical principle: “Test the machine with your material, your files, and your production targets.” Treat it as editorial guidance, not a quotation from a named expert. There is no perfect specification sheet. Operator skill, maintenance access, and daily workload can change real-world results. A little uncertainty is useful. It prompts better questions before a purchase, and helps buyers choose Rubber Automatic Cutting equipment that fits the work they actually need to do.
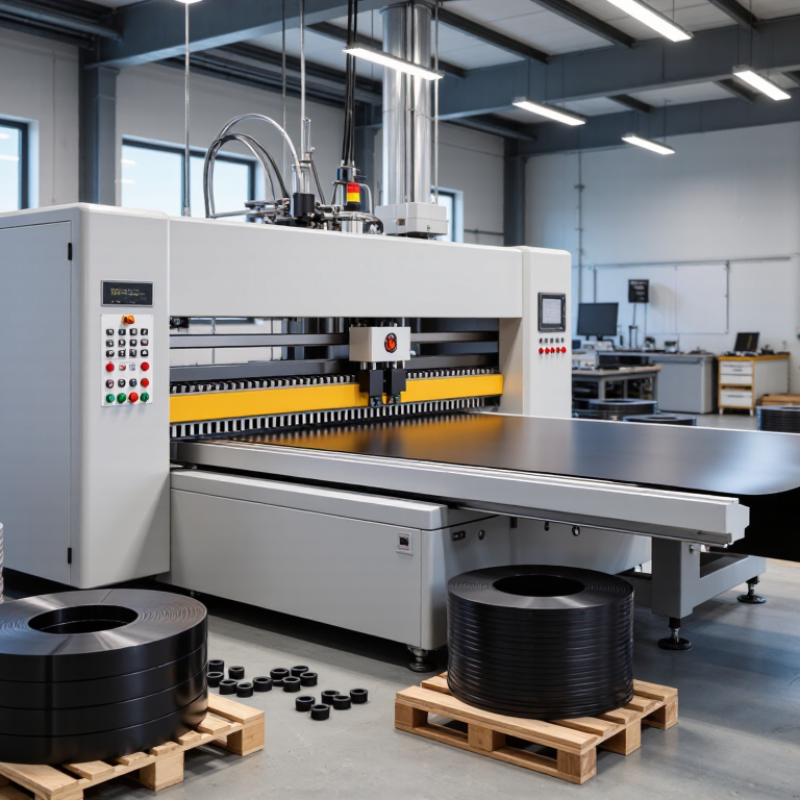
How to Choose a Rubber Automatic Cutting Machine in 2026? Start with measured hardness, not a guess. ASTM D2240 defines durometer testing for rubber and elastomers, including the Shore A scale. Record several readings from a flat, clean sample, then note the test temperature and reading time. A single value can mislead. For example, a batch reading of 55 Shore A may cut differently from another compound with the same reading but different elasticity or thickness.
Use hardness as a screening guide, not a cutting-force formula. Softer rubber can stretch or deform under a blade; harder stock may need greater feed stability and a sharper tool. ASTM D2240-15(2021) and ISO 48-4:2018 provide recognized methods for measuring rubber hardness. Compare their test data with actual cutting trials on your material, recording edge quality, distortion, and cycle time. I would not treat any Shore A boundary as universal; compound composition matters.
Tips: Keep a small test coupon from each batch. Confirm its Shore A reading, thickness, and temperature before setting blade speed or pressure. If results vary, repeat the test and inspect the sample surface. Small details matter. A hardness number helps narrow machine settings, but a short production trial should confirm them.
Choose a cutting method only after measuring the rubber you will actually run. Sheet thickness can vary across a roll or batch. Measure both. A CNC oscillating knife often suits flexible, thin-to-medium sheets and changing part shapes, because it avoids dedicated tooling. Thick, dense rubber may deflect the blade or compress under the hold-down, leaving tapered edges. For repeated parts in large runs, a steel-rule die can be faster, but it adds tooling cost and is less adaptable to design changes.
Set the required tolerance from the part’s function, not just the machine specification. A gasket with narrow sealing lands needs more control than a floor mat with broad edges. Sheet movement, hardness, blade wear, and hold-down pressure all affect the result. Ask for sample cuts using your own compound and maximum sheet thickness. Check dimensions at several points, including internal corners and small holes. A quoted accuracy figure is only a starting point. I would not assume one test sheet proves consistency; repeat the cut after changing material batches or blade condition. That extra check can feel fussy, but missed fits are worse.
Knife, die, and laser systems solve different production problems. A drag or oscillating knife creates a narrow kerf and avoids heat, making it useful for gaskets, foam rubber, and short runs with frequent design changes. Throughput depends on material thickness, blade condition, and how tightly parts can be nested. Die cutting can produce many identical pieces quickly once the tooling is ready, but each new shape may require a die. Laser cutting handles detailed profiles without physical tooling, though its kerf, edge finish, and heat-affected area vary with rubber type and settings. Heat can discolor edges or leave residue. Test samples matter.
Tips: Ask suppliers to cut your actual compound and thickness. Measure kerf, inspect both sides of the edge, and record cycle time across a realistic batch. Include setup, loading, and tool changes in throughput estimates—not just cutting speed. A clean edge on one sample is encouraging, but it is not proof of consistent production.
For routine purchasing, compare usable output, scrap, and maintenance alongside machine speed. Check whether the intended rubber produces fumes or edge changes under laser processing, and confirm suitable extraction is available. Knife cutting may seem slower on paper, yet flexibility can pay off for mixed orders. That trade-off is easy to underestimate.
When choosing a rubber automatic cutting machine, start with the parts required per hour, then check whether the table can hold a useful cutting layout. Measure the largest part, sheet width, and clearance needed for clamps or material tracking. A large table is not automatically productive; awkward nesting can leave valuable space unused. Feed rate matters too, but the machine’s advertised speed may not reflect intricate cuts, thick rubber, or frequent repositioning. Test your actual material.
ISO 22400-2:2014 defines manufacturing performance measures that include production rate, availability, and quality ratio. Use those ideas to estimate good parts, not just theoretical cycles. For example, a layout of six parts and a 30-second cycle gives 720 parts per hour before losses. At 75% availability and 95% acceptable output, that becomes about 513 good parts per hour. That is close to a 500-part target. Very close. I would verify it with a timed trial across several sheets; one clean run can flatter a machine. Record feed speed, loading pauses, scrap, and completed parts, then compare the results with your required hourly rate.
Evaluate a rubber automatic cutting machine against the finished part’s drawing, not a brochure’s best-case accuracy. ISO 3302-1 specifies dimensional tolerance classes for rubber products, but the appropriate class depends on the product and its requirements. It does not certify a cutter or set one tolerance for every cut shape. Check the drawing for the specified class and critical dimensions. Then test samples using the actual rubber compound and thickness. Measure length, width, and key features with calibrated tools under controlled conditions. Small details matter. A cold sheet may behave differently.
Tips: Request a repeatability trial using a representative batch, not just one sample. Record the minimum, maximum, and average dimensions, and compare each result with the drawing limits. Check for blade wear and material movement during cutting. A first-pass test can look clean, yet drift may appear during a longer run. That deserves attention. If results vary, investigate setup and material handling before deciding the machine meets your needs.
| Cookie | Duration | Description |
|---|---|---|
| AWSALB | 7 days | AWSALB is a cookie generated by the Application load balancer in the Amazon Web Services. It works slightly different from AWSELB. |
| AWSALBCORS | 7 days | This cookie is used for load balancing services provded by Amazon inorder to optimize the user experience. Amazon has updated the ALB and CLB so that customers can continue to use the CORS request with stickness. |
| cookielawinfo-checkbox-advertisement | 1 year | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Advertisement". |
| cookielawinfo-checkbox-analytics | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytic / Performance". |
| cookielawinfo-checkbox-functional | 11 months | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional". |
| cookielawinfo-checkbox-necessary | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Strictly Necessary". |
| cookielawinfo-checkbox-performance | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance". |
| cookielawinfo-checkbox-preferences | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Preferences." |
| elementor | never | This cookie is used by the website's WordPress theme. It allows the website owner to implement or change the website's content in real-time. |
| viewed_cookie_policy | 11 months | The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data. |
| Cookie | Duration | Description |
|---|---|---|
| CONSENT | 16 years 4 months | These cookies are set via embedded youtube-videos. They register anonymous statistical data on for example how many times the video is displayed and what settings are used for playback.No sensitive data is collected unless you log in to your google account, in that case your choices are linked with your account, for example if you click “like” on a video. |
| _ga | 2 years | This cookie is installed by Google Analytics. The cookie is used to calculate visitor, session, campaign data and keep track of site usage for the site's analytics report. The cookies store information anonymously and assign a randomly generated number to identify unique visitors. |
| _gat_gtag_UA_47200144_1 | 1 minute | This cookie is set by Google and is used to distinguish users. |
| _gid | 1 day | This cookie is installed by Google Analytics. The cookie is used to store information of how visitors use a website and helps in creating an analytics report of how the website is doing. The data collected including the number visitors, the source where they have come from, and the pages visted in an anonymous form. |
| _hjAbsoluteSessionInProgress | session | This cookie is used to count how many times a website has been visited by different visitors. This is done by assigning the visitor an ID, so the visitor does not get registered twice. |
| _hjFirstSeen | 30 minutes | This is set by Hotjar to identify a new user’s first session. It stores a true/false value, indicating whether this was the first time Hotjar saw this user. It is used by Recording filters to identify new user sessions. |
| _hjid | 1 year | This cookie is set by Hotjar. This cookie is set when the customer first lands on a page with the Hotjar script. It is used to persist the random user ID, unique to that site on the browser. This ensures that behavior in subsequent visits to the same site will be attributed to the same user ID. |
| _hjIncludedInPageviewSample | session | This cookie is used to detect whether the user navigation and interactions are included in the website’s data analytics. |
| Cookie | Duration | Description |
|---|---|---|
| IDE | 1 year 24 days | This cookie is used by Google DoubleClick and stores information about how the user uses the website and any other advertisement before visiting the website. This is used to present users with ads that are relevant to them according to the user profile. |
| NID | 6 months | This cookie is used to a profile based on user's interest and display personalized ads to the users. |
| test_cookie | 15 minutes | This cookie is set by doubleclick.net. The purpose of the cookie is to determine if the user's browser supports cookies. |
| VISITOR_INFO1_LIVE | 5 months 27 days | This cookie is set by Youtube it is used to track the information of the embedded YouTube videos on a website. |
| YSC | session | This cookies is set by Youtube and is used to track the views of embedded videos. |
| yt-remote-connected-devices | never | These cookies are set via embedded youtube-videos. |
| yt-remote-device-id | never | These cookies are set via embedded youtube-videos. |
| Cookie | Duration | Description |
|---|---|---|
| qtrans_front_language | 1 year | This cookie is set by qTranslate WordPress plugin. The cookie is used to manage the preferred language of the visitor. |