Choosing a Cold Foil Printing Machine in 2026 means matching equipment to real production needs, not simply chasing peak speed. The right choice depends on the materials you run, the effects customers expect, and how the machine fits your existing press. A coating that looks bright on a supplier’s sample may behave differently on your own stock. That difference matters.
Start with practical details: compatible substrates, usable web width, running speed, registration accuracy, and foil-transfer consistency. Ask how quickly operators can change jobs and clean the coating system. Small delays add up. Consider whether the machine supports your typical carton, label, or flexible-packaging work, and whether it can connect smoothly with your current workflow. A specification sheet helps, but it cannot answer everything.
Request a production trial using your actual material and artwork. Check fine lines, solid areas, edge definition, and results across a full run—not just one attractive sheet. I would not treat an impressive demonstration sample as proof; that is an easy mistake. Compare service response, spare-part availability, training, and the total cost of ownership alongside the purchase price. A checklist helps, though it can still miss the small frustrations operators notice after installation. This guide looks at the questions worth asking before you choose, so your decision rests on measurable performance rather than polished promises.
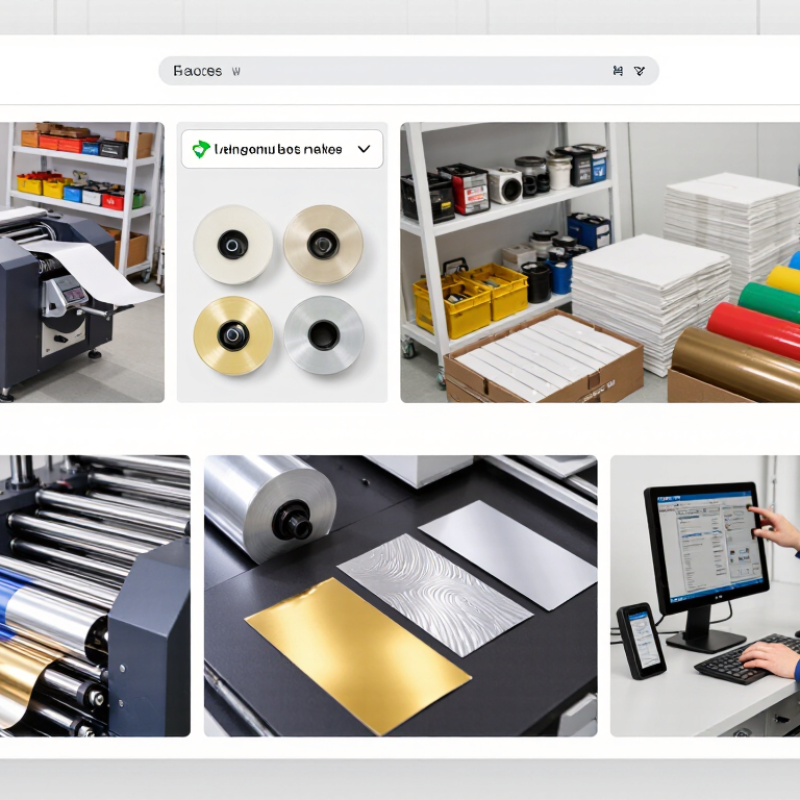
Cold foil printing transfers a metallic finish onto selected areas of paper, board, or film. A press applies adhesive where the shine is needed, then brings a foil web into contact under controlled pressure. The foil releases onto the adhesive pattern, leaving other areas uncoated. Many systems use UV-curable adhesive, so curing capability and compatibility matter. That detail matters.
Cold foil suits labels, folding cartons, and promotional print where bright accents need to align with text or graphics. When assessing a machine, check its registration accuracy, usable web width, speed range, and ability to handle your actual substrates. Ask how operators control foil tension and adhesive laydown; small variations can cause wrinkles, gaps, or uneven shine. A fast rated speed is not enough. Run a sample job with your stock and artwork, then inspect fine lines and solid areas under consistent light. I would not rely on a brochure figure alone.
Tips: Confirm that the press supports the adhesive and curing method your workflow requires. Test setup time, waste, and repeatability—not just the finished sample. A little uncertainty is normal; record the test conditions so results can be compared.
How to Choose a Cold Foil Printing Machine in 2026? Identify the Materials, Formats, and Production Needs
Start with the stock you actually print, not a machine’s headline speed. Paperboard, coated paper, films, and labels can behave differently under adhesive, pressure, and heat. Cold foil systems generally transfer foil through an adhesive and a nip, so confirm that the machine suits your adhesive and curing method. Bring representative samples, including the thinnest film and heaviest board you use. Check adhesion, fine-line detail, and foil coverage after finishing. A small test can reveal curl or scuffing that a brochure will not.
Match the machine to your format and workflow. Sheet-fed production needs suitable sheet dimensions and reliable feeding; roll-fed work depends on web width, tension control, and changeover time. Ask for demonstrated registration accuracy at your normal speed, not only under ideal conditions. If foil appears beside printed colors, confirm how the unit integrates with your press and drying or curing equipment. I would not assume every substrate runs cleanly. Even familiar stock can surprise you.
Tips: Bring a real job file and substrate samples to a production trial. Record speed, setup waste, foil consumption, and reject rate—not just the best-looking sheet. Check whether operators can adjust pressure and registration without lengthy stops. Leave room for future formats, but avoid paying for capacity your current workflow cannot use.
A cold foil machine should match your production route, not just your target speed. Standalone units suit separate finishing lines; inline modules reduce handling between printing and foiling. Retrofit systems can be practical, but confirm press access, web direction, and available space before ordering. Smithers’ The Future of Global Packaging to 2028 forecasts a global packaging market of about $1.2 trillion by 2028. That growth makes finishing capacity relevant, but it does not prove any one machine will fit your jobs.
Check substrate compatibility with the actual stocks you run: coated paper, label paper, or film. Ask suppliers to test foil release, adhesive bonding, and registration on your material. Test first. A specification sheet cannot show every curl or surface variation. This is where selection gets less tidy.
Compare usable width, minimum and maximum stock thickness, running speed, registration tolerance, and changeover time. Ask how speed changes with finer detail or larger foil areas. Confirm adhesive and curing requirements, plus waste during setup. The FTA’s FIRST quality guidelines emphasize process control and repeatability in flexographic printing; use that same discipline when reviewing sample runs and acceptance criteria. Request measured results, not only demonstrations. A small trial may still miss a difficult job, so leave room for a second test.
Choosing a cold foil printing machine in 2026 means looking beyond its purchase price. Compare the full cost: installation, dies, foil consumption, maintenance, training, and expected waste during setup. Ask for a live demonstration using your own stock and artwork. Check registration accuracy across a production run, not just on one impressive sample. Small differences matter.
Automation can reduce repetitive adjustments, but it cannot fix every process problem. Match the machine’s controls and feed system to your job mix, operator skills, and planned output. Request clear figures for setup time and changeovers. Then confirm which functions are automated and which still require manual checks. Keep it practical.
Safety deserves a close inspection. Look for accessible emergency stops, guarding around moving parts, and clear operating instructions. Ask how operators are trained and how routine maintenance is performed safely.
Supplier support matters just as much. Confirm spare-parts availability, response times, installation help, and access to troubleshooting. Get these commitments in writing.
A spreadsheet won’t capture every shift or every awkward job, and I’d treat polished sample results with some caution. The right choice is the machine your team can run consistently, maintain confidently, and support without guesswork.
A cold foil press should prove repeatability on your actual stock, not just achieve a headline speed. Run a trial with your substrate, adhesive, foil, ink, and finishing sequence. Record registration drift, foil release, adhesion, waste, and stoppages at both start-up and steady speed. Keep samples. A clean first pass can still mislead if the run is short or the material is unusually forgiving. Smithers’ The Future of Global Packaging to 2028 valued the global packaging market at about $1.17 trillion in 2023. That scale signals a demanding production environment, but it does not predict any single machine’s output.
Ask the supplier to repeat the trial after a changeover, then compare results against agreed acceptance limits. Track actual setup time and usable output, not theoretical maximum speed. Small details matter. Check whether operators can access rollers safely, clean adhesive buildup, and identify wear before defects spread. Request a maintenance schedule covering inspection intervals, consumables, spare-part availability, and service response times. Price these costs across several years; purchase price alone can hide downtime expenses. One point deserves reflection: the trial itself creates waste, yet skipping it can make a costly problem harder to diagnose later. Keep the test conditions and results with the machine’s service records.
| Evaluation Area | How to Verify During a Trial | Suggested Acceptance Check | Long-Term Maintenance Planning |
|---|---|---|---|
| Foil adhesion and transfer | Run the intended foil, adhesive, ink, coating, and substrate combination. Inspect solid areas, fine details, and edges under consistent lighting. | Agree on a visual defect limit and a repeatable tape-pull or rub test for the specific job. Check for pinholes, voids, edge lift, and unwanted foil pickup. | Define cleaning intervals for adhesive and foil residue. Keep approved foil and adhesive specifications, test samples, and setup records available. |
| Registration and repeatability | Measure foil-to-print alignment at the start, middle, and end of a sustained run using the same artwork and inspection method. | Set the allowable registration tolerance from the product design and customer specification; confirm that results remain within it after the press reaches stable running conditions. | Schedule checks of sensors, web guides, bearings, and drive components. Record calibration results and investigate drift rather than correcting it only at the operator control. |
| Web tension and foil handling | Test the planned foil widths and roll sizes. Observe unwinding, guiding, splicing, and rewinding during acceleration, steady running, and deceleration. | Look for stable tracking without wrinkles, telescoping, breaks, or avoidable foil waste. Confirm that tension settings can be repeated for each job. | Inspect tension-control components, rollers, brakes, and guide mechanisms at intervals specified by the equipment supplier. Keep wear parts and adjustment procedures documented. |
| Speed and usable output | Run representative jobs at the intended production speed, including setup, ramp-up, steady production, and changeover where practical. | Compare saleable output—not just the machine’s rated speed—and record stable running speed, setup time, rejects, and foil consumption for the agreed trial conditions. | Plan preventive maintenance around production hours and operating conditions. Review downtime, scrap, and recurring faults so maintenance intervals reflect actual use. |
| Substrate and job range | Trial the actual stock types, thicknesses, widths, and surface finishes expected in production, including the most demanding planned job. | Confirm that feeding, transport, foil transfer, and delivery are stable for each required material. Record any job-specific limits or setup changes. | Maintain a controlled list of validated substrates and recipes. Requalify settings when foil, adhesive, ink, coating, or stock specifications change. |
| Inspection and operator controls | Ask operators to set up a job, adjust foil tracking, respond to a simulated fault, and restore saved settings. Check alarms and inspection functions if included. | Verify that controls and instructions are understandable, faults are identifiable, and agreed quality checks can be performed consistently across shifts. | Provide operator and maintenance training, keep current manuals and backup settings, and establish a clear process for logging faults and corrective actions. |
| Serviceability and parts support | Review access to routine service points and request a documented list of consumables, recommended spares, and maintenance tasks. | Confirm responsibility for installation, training, technical support, parts availability, and response arrangements in writing before purchase. | Build a planned maintenance calendar, budget for wear parts, and keep records of inspections, replacements, service visits, and machine downtime. |
| Trial documentation | Use agreed artwork, materials, run length, speed range, inspection method, and acceptance criteria. Retain samples from the trial. | Record settings, measured results, defects, waste, and any deviations. Treat numerical targets as project-specific rather than universal machine standards. | Use the trial record as the baseline for production audits, troubleshooting, staff training, and future comparisons of performance. |
Note: Acceptance limits should be agreed in advance and validated with the intended materials, artwork, and production conditions. Actual maintenance intervals should follow the equipment documentation and operating environment.
| Cookie | Duration | Description |
|---|---|---|
| AWSALB | 7 days | AWSALB is a cookie generated by the Application load balancer in the Amazon Web Services. It works slightly different from AWSELB. |
| AWSALBCORS | 7 days | This cookie is used for load balancing services provded by Amazon inorder to optimize the user experience. Amazon has updated the ALB and CLB so that customers can continue to use the CORS request with stickness. |
| cookielawinfo-checkbox-advertisement | 1 year | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Advertisement". |
| cookielawinfo-checkbox-analytics | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytic / Performance". |
| cookielawinfo-checkbox-functional | 11 months | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional". |
| cookielawinfo-checkbox-necessary | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Strictly Necessary". |
| cookielawinfo-checkbox-performance | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance". |
| cookielawinfo-checkbox-preferences | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Preferences." |
| elementor | never | This cookie is used by the website's WordPress theme. It allows the website owner to implement or change the website's content in real-time. |
| viewed_cookie_policy | 11 months | The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data. |
| Cookie | Duration | Description |
|---|---|---|
| CONSENT | 16 years 4 months | These cookies are set via embedded youtube-videos. They register anonymous statistical data on for example how many times the video is displayed and what settings are used for playback.No sensitive data is collected unless you log in to your google account, in that case your choices are linked with your account, for example if you click “like” on a video. |
| _ga | 2 years | This cookie is installed by Google Analytics. The cookie is used to calculate visitor, session, campaign data and keep track of site usage for the site's analytics report. The cookies store information anonymously and assign a randomly generated number to identify unique visitors. |
| _gat_gtag_UA_47200144_1 | 1 minute | This cookie is set by Google and is used to distinguish users. |
| _gid | 1 day | This cookie is installed by Google Analytics. The cookie is used to store information of how visitors use a website and helps in creating an analytics report of how the website is doing. The data collected including the number visitors, the source where they have come from, and the pages visted in an anonymous form. |
| _hjAbsoluteSessionInProgress | session | This cookie is used to count how many times a website has been visited by different visitors. This is done by assigning the visitor an ID, so the visitor does not get registered twice. |
| _hjFirstSeen | 30 minutes | This is set by Hotjar to identify a new user’s first session. It stores a true/false value, indicating whether this was the first time Hotjar saw this user. It is used by Recording filters to identify new user sessions. |
| _hjid | 1 year | This cookie is set by Hotjar. This cookie is set when the customer first lands on a page with the Hotjar script. It is used to persist the random user ID, unique to that site on the browser. This ensures that behavior in subsequent visits to the same site will be attributed to the same user ID. |
| _hjIncludedInPageviewSample | session | This cookie is used to detect whether the user navigation and interactions are included in the website’s data analytics. |
| Cookie | Duration | Description |
|---|---|---|
| IDE | 1 year 24 days | This cookie is used by Google DoubleClick and stores information about how the user uses the website and any other advertisement before visiting the website. This is used to present users with ads that are relevant to them according to the user profile. |
| NID | 6 months | This cookie is used to a profile based on user's interest and display personalized ads to the users. |
| test_cookie | 15 minutes | This cookie is set by doubleclick.net. The purpose of the cookie is to determine if the user's browser supports cookies. |
| VISITOR_INFO1_LIVE | 5 months 27 days | This cookie is set by Youtube it is used to track the information of the embedded YouTube videos on a website. |
| YSC | session | This cookies is set by Youtube and is used to track the views of embedded videos. |
| yt-remote-connected-devices | never | These cookies are set via embedded youtube-videos. |
| yt-remote-device-id | never | These cookies are set via embedded youtube-videos. |
| Cookie | Duration | Description |
|---|---|---|
| qtrans_front_language | 1 year | This cookie is set by qTranslate WordPress plugin. The cookie is used to manage the preferred language of the visitor. |