Choosing the best T beam welding line in China starts with the beam, not the brochure. A line suited to one factory may struggle with another’s web height, flange width, steel thickness, or production mix. Buyers should compare the complete process: positioning, tack welding, main welding, conveying, and any required straightening. Details matter. A misplaced web can create uneven welds, extra correction work, and delays downstream.
For a clearly illustrative expert perspective, fictional welding engineer Lin Wei puts it this way: “Repeatability matters more than headline speed.” That principle points to practical questions: Can the line hold alignment across the specified beam range? Are welding parameters adjustable and documented? Can operators access consumables and service points without awkward workarounds? Ask suppliers for a sample production run using your drawings and material, then inspect fit-up, weld consistency, and measured output. See the results yourself.
A strong T beam welding line should match real workloads, not just impressive maximum figures. Review installation support, operator training, spare-parts access, and references from comparable applications. A factory visit can reveal small but important clues, such as cable routing, fixture condition, and how quickly settings change between sizes. No line is perfect. I would also question any offer that promises high speed without explaining its operating conditions. Compare evidence, clarify assumptions, and choose equipment your team can run reliably on an ordinary production day.
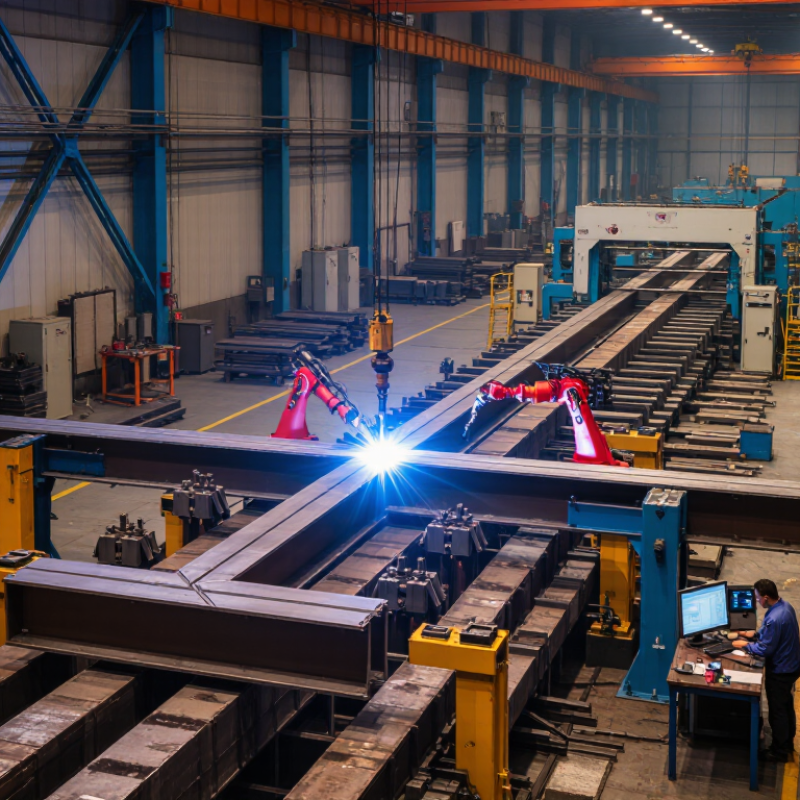
A T-beam welding line joins a vertical steel web to a horizontal flange, forming a T-shaped structural member. The line may include plate positioning, tack welding, continuous welding, straightening, and cutting. Its output is ready-to-use beams for building frames, equipment supports, and other fabricated structures. Details vary by design.
Worldsteel’s World Steel in Figures 2024 reports 1,892.2 million tonnes of crude steel production worldwide in 2023. That figure shows the scale of steel supply, not T-beam demand or line productivity. A typical line uses clamps to hold the web and flange square while welding equipment makes consistent seams. Operators still check alignment, weld appearance, and dimensions. Real shops are less tidy. Heat distortion or uneven plate edges can affect fit-up, even when automation is running. I would not treat fast travel speed as proof of quality; stable joints and accurate dimensions matter more.
A practical T beam welding line links plate feeding, positioning, tack welding, main welding, straightening, and discharge. The web plate stands between two flange plates, held by adjustable clamps. Accurate alignment matters: a small gap or tilt can create uneven welds and extra correction work. Small errors travel.
A tack-welding station fixes the assembly before continuous welding. Many lines use submerged arc welding for long, steady seams, with a gantry or welding carriage guiding the torch. Sensors and controls help maintain travel speed and torch position. Hydraulic or servo straighteners then correct distortion caused by heat. Operators should still inspect the beam; automation does not catch every setup mistake.
Automation is increasingly common across manufacturing, though not every process needs a robot. The International Federation of Robotics’ World Robotics 2023 report recorded 553,052 industrial robot installations worldwide in 2022, a 5% rise from 2021. This broad figure is not specific to T beam production, but it shows the scale of industrial automation. When comparing lines, check usable beam dimensions, welding speed, straightening capacity, and changeover time. Ask for a trial using your actual plate thickness. A smooth demonstration is useful, but real production can be less tidy.
A T-beam welding line works best when fit-up, welding, straightening, and transfer are treated as one connected process. The web is positioned against the flange, then clamps hold both parts steady before welding. Operators check the web’s centerline and the flange’s edge; a small gap can affect the finished joint. Keep it square.
Welding may use a gantry or submerged arc process, depending on beam size and production needs. A balanced weld sequence helps limit heat distortion. Still, heat can pull the web out of alignment, especially on long sections. Watch the seam closely. Recording current, travel speed, and visible defects helps teams repeat sound settings, though one recipe will not suit every thickness.
After welding, the beam is checked for sweep and flange tilt. A straightening machine applies measured pressure to correct distortion, rather than forcing the steel into place in one pass. Too much pressure can create a new problem. Once dimensions are verified, a roller bed or crane moves the beam to the next station. Clear lift points and stable supports protect the beam and nearby workers. The awkward part is that handling marks are easy to overlook until inspection.
Comparing T beam welding lines in China starts with the actual beam range, not the advertised maximum. Record web height, flange width, plate thickness, and daily output. Ask suppliers to run a representative workpiece, including the thickest plate and a short beam. Watch alignment before welding. Small gaps matter. Poor fit-up can increase correction work and distortion, even when the weld itself looks sound.
Check how the line handles tack welding, submerged arc welding, straightening, and material transfer. Compare usable speed under your production conditions, rather than relying on a peak figure. Inspect weld continuity, leg size, and deformation against your drawings and acceptance criteria. Request measured trial records. Then test again. A clean demonstration beam may not reveal setup delays, changeover time, or operator dependence.
Also compare controls, guarding, extraction, spare-part access, and maintenance instructions. Ask how quickly common wear parts can be replaced and what training is included. Confirm the line can accommodate future product changes without major rebuilding. Price matters, but so do floor space, power demand, and commissioning support. A spreadsheet can miss these costs. I would avoid naming one line “best” before seeing repeatable results on your own material; that judgment can be uncomfortable, but it is more useful.
Compare T beam welding lines using the factors that matter most to your production needs. The percentages below are a suggested evaluation weighting—not supplier rankings or market survey results.
Assess weld consistency, achievable cycle time, and supported beam dimensions against your drawings and production targets. Also verify automation and changeover requirements, operating costs, safety provisions, and the availability of service and spare parts.
What Is the Best T Beam Welding Line in China?
How Production Needs Shape the Choice of Line Configuration
The best T-beam welding line is the one that fits your actual production mix, not the one with the most automation. Start with beam height, flange width, plate thickness, and daily output. A shop making a few large, changing designs may need flexible positioning and quick fixture adjustments. A plant running the same beam sizes all week may gain more from automatic feeding and continuous welding. Measure changeover time, too. It is often underestimated.
Line configuration also depends on floor space, operator skills, and downstream straightening. Check whether the line can maintain stable alignment before welding; small fit-up errors can become visible distortion later. The International Federation of Robotics reported 541,302 industrial robot installations worldwide in 2023, with Asia accounting for about 70% of installations (World Robotics 2024). That shows broad automation adoption, but it does not mean every beam shop needs a fully robotic line. Match automation to repeatability and labor constraints.
Tips: Before requesting quotations, record beam dimensions, material thicknesses, weekly volume, and changeover frequency. Ask suppliers to demonstrate a representative beam—not just a fast cycle on an ideal sample. Check access for maintenance and verify that the proposed line handles your smallest and largest sections. Leave room for revision; production plans rarely stay perfect.
| Production Need | Suitable Line Configuration | Typical Process Arrangement | Key Advantages | Main Trade-Offs | Best Fit |
|---|---|---|---|---|---|
| Small batches with frequent changes in beam dimensions | Flexible, semi-automatic line | Separate fit-up, tack welding, main welding, and straightening stations; operators adjust fixtures and settings between jobs. | Lower commitment to dedicated tooling; easier to accommodate varied section sizes and short production runs. | More operator involvement and setup time; output depends strongly on preparation, handling, and operator experience. | Job shops and manufacturers producing varied T-beam specifications in relatively small quantities. |
| Repeated orders with a stable range of beam sizes | Mechanized production line with adjustable fixtures | Controlled feeding and alignment, mechanized welding, and dedicated downstream straightening or handling equipment. | More consistent positioning and welding travel than a largely manual arrangement; changeovers remain possible within the designed range. | Adjustment limits depend on the fixture and machine design; changeovers still require time and process verification. | Plants with recurring product families and moderate-to-high production volumes. |
| High-volume production of a narrow product range | Dedicated, highly automated line | Integrated material handling, repeatable fit-up, automated welding travel, and coordinated inspection and discharge steps. | Supports repeatable cycle sequences and reduces routine manual handling when the line is properly balanced. | Higher equipment and integration commitment; less adaptable to frequent design changes, and an unbalanced station can constrain the whole line. | Producers with stable specifications, predictable demand, and sufficient space for an integrated layout. |
| Long welds where distortion control is a priority | Line configured around controlled welding sequence and straightening | Stable clamping and alignment, a qualified welding sequence, suitable heat-input control, and a planned straightening stage where required. | Addresses the effects of weld shrinkage through process control and downstream correction rather than relying on welding speed alone. | Results depend on material, thickness, joint design, restraint, welding procedure, and straightening method; trials may be needed. | Fabricators handling long members or applications with defined straightness and dimensional requirements. |
| Limited workshop space or restricted material flow | Compact or modular line layout | Stations arranged to suit available floor space, with material loading, transfer, access, and finished-product removal planned together. | Can fit an existing workshop and may allow staged equipment investment. | Compact layouts can create handling bottlenecks; maintenance access and safe movement of long beams must not be compromised. | Existing facilities where building footprint or crane coverage limits a conventional straight-line arrangement. |
| Uncertain demand or plans to expand later | Modular line with provision for future automation | Core fit-up and welding equipment installed first, with interfaces and material-flow space reserved for additional handling or process stations. | Allows investment to be phased and can reduce the need to replace the entire line when requirements grow. | Future expansion is practical only if utilities, layout, controls, and station interfaces are planned from the start. | New production operations or businesses forecasting gradual growth in volume or automation needs. |
Selection note: There is no single best configuration for every T-beam producer. Compare lines using the actual beam-size range, plate thickness, weld length, required dimensional tolerances, production mix, shift pattern, available floor space, material-handling method, and the applicable welding procedure. Request a production trial or a documented cycle-time estimate based on representative workpieces before making a final decision.
| Cookie | Duration | Description |
|---|---|---|
| AWSALB | 7 days | AWSALB is a cookie generated by the Application load balancer in the Amazon Web Services. It works slightly different from AWSELB. |
| AWSALBCORS | 7 days | This cookie is used for load balancing services provded by Amazon inorder to optimize the user experience. Amazon has updated the ALB and CLB so that customers can continue to use the CORS request with stickness. |
| cookielawinfo-checkbox-advertisement | 1 year | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Advertisement". |
| cookielawinfo-checkbox-analytics | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytic / Performance". |
| cookielawinfo-checkbox-functional | 11 months | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional". |
| cookielawinfo-checkbox-necessary | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Strictly Necessary". |
| cookielawinfo-checkbox-performance | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance". |
| cookielawinfo-checkbox-preferences | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Preferences." |
| elementor | never | This cookie is used by the website's WordPress theme. It allows the website owner to implement or change the website's content in real-time. |
| viewed_cookie_policy | 11 months | The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data. |
| Cookie | Duration | Description |
|---|---|---|
| CONSENT | 16 years 4 months | These cookies are set via embedded youtube-videos. They register anonymous statistical data on for example how many times the video is displayed and what settings are used for playback.No sensitive data is collected unless you log in to your google account, in that case your choices are linked with your account, for example if you click “like” on a video. |
| _ga | 2 years | This cookie is installed by Google Analytics. The cookie is used to calculate visitor, session, campaign data and keep track of site usage for the site's analytics report. The cookies store information anonymously and assign a randomly generated number to identify unique visitors. |
| _gat_gtag_UA_47200144_1 | 1 minute | This cookie is set by Google and is used to distinguish users. |
| _gid | 1 day | This cookie is installed by Google Analytics. The cookie is used to store information of how visitors use a website and helps in creating an analytics report of how the website is doing. The data collected including the number visitors, the source where they have come from, and the pages visted in an anonymous form. |
| _hjAbsoluteSessionInProgress | session | This cookie is used to count how many times a website has been visited by different visitors. This is done by assigning the visitor an ID, so the visitor does not get registered twice. |
| _hjFirstSeen | 30 minutes | This is set by Hotjar to identify a new user’s first session. It stores a true/false value, indicating whether this was the first time Hotjar saw this user. It is used by Recording filters to identify new user sessions. |
| _hjid | 1 year | This cookie is set by Hotjar. This cookie is set when the customer first lands on a page with the Hotjar script. It is used to persist the random user ID, unique to that site on the browser. This ensures that behavior in subsequent visits to the same site will be attributed to the same user ID. |
| _hjIncludedInPageviewSample | session | This cookie is used to detect whether the user navigation and interactions are included in the website’s data analytics. |
| Cookie | Duration | Description |
|---|---|---|
| IDE | 1 year 24 days | This cookie is used by Google DoubleClick and stores information about how the user uses the website and any other advertisement before visiting the website. This is used to present users with ads that are relevant to them according to the user profile. |
| NID | 6 months | This cookie is used to a profile based on user's interest and display personalized ads to the users. |
| test_cookie | 15 minutes | This cookie is set by doubleclick.net. The purpose of the cookie is to determine if the user's browser supports cookies. |
| VISITOR_INFO1_LIVE | 5 months 27 days | This cookie is set by Youtube it is used to track the information of the embedded YouTube videos on a website. |
| YSC | session | This cookies is set by Youtube and is used to track the views of embedded videos. |
| yt-remote-connected-devices | never | These cookies are set via embedded youtube-videos. |
| yt-remote-device-id | never | These cookies are set via embedded youtube-videos. |
| Cookie | Duration | Description |
|---|---|---|
| qtrans_front_language | 1 year | This cookie is set by qTranslate WordPress plugin. The cookie is used to manage the preferred language of the visitor. |