Choosing the best Hydrocarbon Cleaning System from China requires more than comparing prices or viewing polished factory photographs. The right system must match the contaminant, component material, cleaning volume, and required surface condition. Dr. Rajiv Kohli, a respected surface-cleaning researcher, emphasizes: “Effective cleaning begins with understanding contamination, surface material, and process conditions.”
That principle guides this introduction. A reliable Chinese system may combine heated cleaning chambers, controlled hydrocarbon solvents, filtration, vacuum drying, and solvent recovery. Picture a metal part leaving the chamber clean, dry, and free from oily residue. The result should be measurable, not merely attractive.
Look for documented cleaning performance, stable temperature control, sealed operation, and clear maintenance procedures. Ask whether the supplier provides test cleaning, process validation, spare parts, operator training, and technical support after installation. These details often reveal more than a low quotation.
Safety also deserves close attention. The equipment should support appropriate ventilation, fire prevention, electrical protection, and local compliance requirements. Certification must be verified for the destination market. Do not rely only on a brochure.
The “best” choice is rarely the cheapest machine. It is the system that delivers repeatable results without creating hidden operating problems. A cheaper offer may conceal higher solvent consumption or difficult maintenance. That risk is easy to underestimate.
This review will compare Chinese manufacturers through practical criteria, including cleaning quality, automation, energy use, safety design, customization, and after-sales reliability. No supplier is perfect. Real factory conditions can expose weaknesses that demonstrations do not show. Careful testing remains essential before making a final decision.
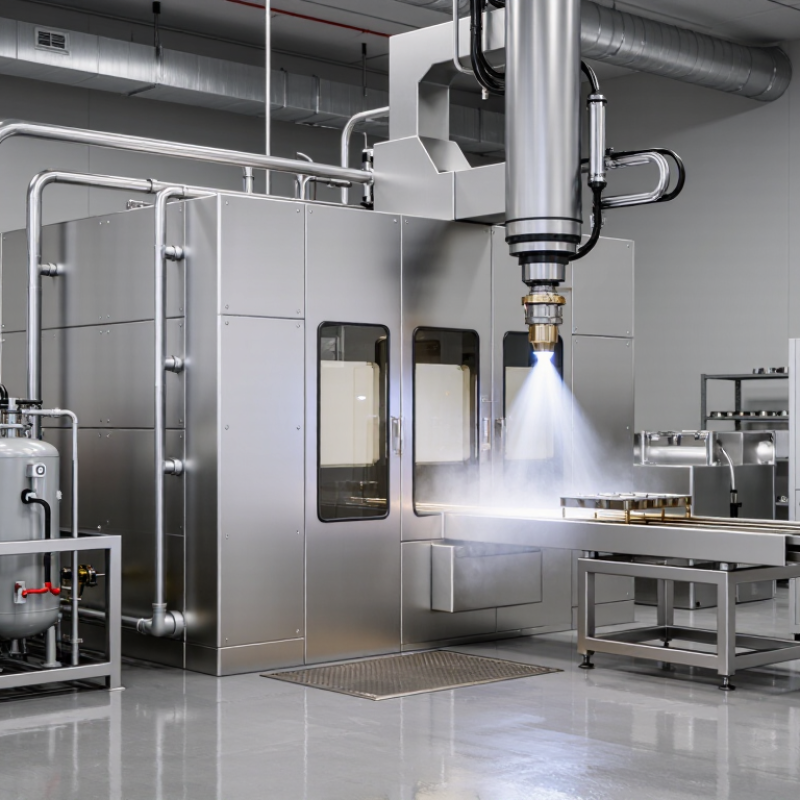
Hydrocarbon cleaning uses refined, non-water-based solvents to remove oil, grease, wax, and machining residue. These solvents dissolve contamination without swelling many metal components. The process often uses sealed chambers, vacuum drying, filtration, and controlled vapor recovery.
In precision manufacturing, cleanliness affects fit, friction, coating adhesion, and electrical reliability. A bearing race may look bright but still hold a thin oil film. That film can change measured torque or attract abrasive dust.
Technicians therefore check particle levels, surface residues, and drying performance, not appearance alone. Small details matter.
The best hydrocarbon cleaning system from China should match the part, solvent, production volume, and compliance requirements. A reliable system needs stable temperature control, effective filtration, leak protection, and repeatable solvent separation. It should also provide clear operating records and accessible maintenance points.
Poor ventilation or weak sealing can create avoidable risks. In real production, cycle speed is not everything. Excessive speed may leave residue inside blind holes.
My own view is that equipment selection often underestimates loading patterns and part geometry. That weakness deserves a practical trial. Test parts should include difficult surfaces, narrow gaps, and the heaviest expected contamination. Engineers can then compare cleanliness, drying time, solvent consumption, and process stability before approval.
What Is the Best Hydrocarbon Cleaning System from China?
The best hydrocarbon cleaning system is not judged by appearance alone. It must produce repeatable results under ISO 16232 and VDA 19.1 cleanliness tests. An experienced evaluation examines washing, rinsing, drying, filtration, and particle recovery. The system should remove oil residues without damaging aluminum parts, seals, or precision surfaces. Test coupons can reveal hidden contamination. A bright component may still fail microscopic inspection.
ISO 16232 and VDA 19.1 support structured cleanliness verification. Inspectors typically extract particles, filter the fluid, and measure particle numbers, sizes, and mass. Some applications also require microscopic images of metallic or fibrous debris. Ask the supplier for raw test data, extraction details, filter information, and repeatability results. A single successful rinse is not enough. It may hide unstable pressure, poor bath control, or operator variation. This is where many evaluations become too optimistic.
Tips: Define the cleanliness limit before comparing systems. Use the same parts, fluid volume, extraction time, and laboratory method. Check results after repeated production cycles, not only after installation. Request independent validation when possible. Also inspect difficult areas, such as blind holes and narrow channels. A small weakness there can affect the entire result. Standards guide the method, but your component geometry decides the real challenge.
What Is the Best Hydrocarbon Cleaning System from China?
For throughput, spray systems usually lead. They wash parts continuously, with short exposure times and easy conveyor integration. Immersion systems suit mixed batches, heavy oil, and complex geometries. Ultrasonic systems reach blind holes and fine channels, but basket loading and acoustic recovery can reduce hourly output. In practice, a spray line may process more parts per hour, while immersion can deliver better soil tolerance. Ultrasonic cleaning is often the strongest choice for precision parts, though not always the fastest. ISO 16232:2018 recommends measuring cleanliness through controlled extraction and particle analysis, rather than judging parts by appearance alone. That distinction matters.
Bath life depends more on soil loading than tank size. Filtration, skimming, solvent distillation, and controlled drag-out can extend usable hydrocarbon solvent. The U.S. Department of Energy reports that compressed-air leaks may waste 20–30% of compressor output, so poorly adjusted spray pressure can raise operating costs. A 2023 industrial cleaning survey by Products Finishing also highlights energy, contamination control, and maintenance as major selection factors. These are practical concerns, not brochure promises. I would still test the actual oil, alloy, and cycle time before choosing equipment. Small parts can behave badly.
Tips: Request a factory trial using your dirtiest production batch. Record parts per hour, solvent loss, filter loading, and cleanliness results. Compare bath life after repeated soil additions. A cheaper machine may become expensive when its solvent turns cloudy every afternoon.
| Evaluation Dimension | Spray Hydrocarbon System | Immersion Hydrocarbon System | Ultrasonic Hydrocarbon System |
|---|---|---|---|
| Cleaning Principle | Pressurized solvent jets mechanically remove oils, chips, and loose particles from exposed surfaces. | Parts are submerged in a solvent bath; agitation, circulation, and optional rotation improve soil removal. | Ultrasonic cavitation creates microscopic bubbles that reach recesses, blind holes, and complex internal features. |
| Typical Throughput | High Approximately 50–500 kg of parts per hour, depending on part geometry, conveyor speed, basket loading, and number of spray stages. | Medium Approximately 20–150 kg of parts per hour in batch or continuous systems, depending on tank volume and dwell time. | Medium to low Approximately 10–100 kg of parts per hour because effective cavitation normally requires controlled loading and longer exposure. |
| Typical Cycle Time | 30 seconds–5 minutes for common external surfaces and moderate oil contamination. | 2–15 minutes, including immersion, agitation, draining, and transfer between stages. | 3–20 minutes, depending on contamination level, ultrasonic frequency, basket density, and part complexity. |
| Indicative Bath or Solvent Service Life | Approximately 1–4 weeks between major solvent replacement events when filtration, vapor recovery, and scheduled maintenance are used. | Approximately 2–8 weeks because the solvent is commonly recirculated and can be continuously filtered or periodically distilled. | Approximately 1–6 weeks; heavy contamination can shorten life because cavitation performance decreases as dissolved oil and particulate levels rise. |
| Bath-Life Extension Methods | Replaceable filters, settling tanks, oil skimmers, solvent condensation, and controlled drag-out reduction. | Coarse and fine filtration, settling, coalescing separation, distillation, and separate rinse stages. | Filtration, settling, distillation, bath-temperature control, and regular removal of sludge from the ultrasonic tank. |
| Solvent Consumption | Low to medium in a closed-loop cabinet; higher if spray pressure, carry-out, or ventilation losses are not controlled. | Low in a sealed system because the same solvent can be reused for many cycles; drag-out control is important. | Low to medium; solvent losses mainly result from carry-out, tank opening, vapor handling, and rinse transfer. |
| Best Soil Removal Capability | Loose chips, cutting oils, stamping oils, and accessible surface contamination. | Heavy oils, grease, particulate contamination, and parts that can be fully wetted and agitated. | Fine particles, dried residues, narrow passages, blind holes, threads, and complex three-dimensional surfaces. |
| Part Geometry Suitability | Best for open, externally accessible parts with consistent orientation and limited shadow areas. | Suitable for irregular parts, bulk components, and parts that tolerate basket handling and immersion. | Best for intricate parts, precision components, small passages, cavities, and assemblies requiring high cleaning uniformity. |
| Typical Operating Temperature | Approximately 40–65°C, subject to the solvent's flash point, equipment design, and safety controls. | Approximately 35–60°C, commonly selected to balance cleaning performance, evaporation control, and solvent safety. | Approximately 35–55°C because excessive temperature can reduce cavitation intensity and increase vapor management requirements. |
| Cleaning Uniformity | High on exposed surfaces; may be lower in shadowed areas or where spray coverage is obstructed. | Medium to high when parts are properly agitated, rotated, and loaded without excessive nesting. | Very high for immersed complex parts when ultrasonic energy distribution and basket loading are correctly designed. |
| Drying Performance | Very good when combined with hot-air blow-off, vacuum drying, or solvent vapor drying. | Good, but drainage and part orientation are important to prevent solvent retention in pockets and cavities. | Good when followed by draining, heated air, vacuum drying, or vapor drying; complex cavities may require additional drying time. |
| Automation Potential | Very high; well suited to conveyorized production lines and robotic loading or unloading. | High; suitable for hoists, rotary baskets, indexing systems, and batch automation. | High; commonly integrated with automatic transfer, multiple tanks, rinsing, drying, and recipe control. |
| Space Requirement | Medium; footprint increases with additional spray, rinse, drying, filtration, and vapor-recovery sections. | Medium to high because tanks, lifting systems, solvent storage, and drying zones require additional space. | Medium to high due to ultrasonic tanks, generators, filtration, rinsing, drying, and acoustic enclosure requirements. |
| Maintenance Load | Medium; spray nozzles, pumps, filters, seals, and mist or vapor-control components require scheduled inspection. | Medium; filters, pumps, tank sludge, seals, solvent quality, and distillation equipment require regular servicing. | Medium to high; ultrasonic transducers, generators, filters, tank condition, and bath cleanliness must be monitored carefully. |
| Main Limitation | Limited access to hidden surfaces, cavities, and areas blocked by part nesting or poor spray orientation. | Longer cycle times and greater solvent inventory than a simple spray stage; parts must be drained effectively. | Higher equipment cost and lower bulk throughput; excessive loading can create uneven ultrasonic energy distribution. |
| Recommended Production Profile | High-volume production with repeatable part geometry and a strong requirement for short cycle time. | Mixed batches, heavy contamination, larger workpieces, and applications requiring long solvent contact time. | Precision or complex components where internal cleanliness and removal of fine particles are more important than maximum throughput. |
| Overall Throughput Score | 5 / 5 | 3 / 5 | 2–3 / 5 |
| Overall Bath-Life Score | 3 / 5 | 4 / 5 | 3–4 / 5 |
| Data note: The figures are representative engineering ranges for closed-loop hydrocarbon cleaning equipment, not guaranteed machine specifications. Actual throughput and bath life depend on solvent type, flash point, oil loading, part mass and geometry, basket fill level, filtration or distillation capacity, operating temperature, cycle design, and cleanliness requirements. Hydrocarbon systems should be designed with appropriate ventilation, vapor recovery, fire protection, grounding, interlocks, and solvent compatibility controls. | |||
Choosing the best hydrocarbon cleaning system from China starts with verified safety data, not catalog claims. Flash point is a practical screening value. Ask for the test method, sample temperature, and laboratory accreditation. ASTM D93 or EN ISO 2719 results are more useful than a rounded number.
Check the actual formulation against GB 38508-2020. This standard sets category-specific VOC limits for cleaning agents, so the product category must appear on the report. A vague “low VOC” statement is insufficient. The report should show VOC content, batch number, testing date, and method. ECHA guidance also treats flash point as an important input for flammability classification. Small differences can change storage requirements.
ATEX needs separate attention. Under Directive 2014/34/EU, equipment suitability depends on the explosive atmosphere and ignition risks. A solvent’s flash point alone does not prove ATEX compliance. Request zone assumptions, electrical ratings, grounding details, and ventilation calculations. The UN Globally Harmonized System, Rev. 10, provides useful classification context, but it is not a substitute for site assessment. I have seen technically impressive files with missing test conditions. That should slow the purchase. Check the liquid, machine, and workplace together. The strongest supplier can provide traceable reports, Chinese standard evidence, and practical operating limits.
What Is the Best Hydrocarbon Cleaning System from China?
The best hydrocarbon cleaning system is not simply the cheapest machine. It should meet your required cleanliness level, measured through particle counting, residue checks, and repeatable test procedures. For precision parts, ask suppliers for documented results on similar materials and geometries. A clean-looking surface can still hide oil inside small channels. That detail matters.
Recovery performance directly affects operating cost. Review solvent recovery rates, filtration life, energy use, and waste volume. A system recovering 90% of its cleaning fluid may reduce purchasing costs, but actual results depend on loading, temperature, and maintenance. Request production data, not only laboratory figures. Cost comparisons should include installation, training, spare parts, and safe fluid handling. The first calculation is rarely complete.
Tips
Measure cleanliness before and after cleaning. Record cycle time, fluid consumption, downtime, and rejected parts for at least four weeks. Ask about remote support and local service response. A system with excellent recovery may still fail your production plan if one pump stops for several days. I would also test difficult parts, not ideal samples. Real production is less forgiving. Availability claims need verification through references, service records, and a written uptime plan.
| Cookie | Duration | Description |
|---|---|---|
| AWSALB | 7 days | AWSALB is a cookie generated by the Application load balancer in the Amazon Web Services. It works slightly different from AWSELB. |
| AWSALBCORS | 7 days | This cookie is used for load balancing services provded by Amazon inorder to optimize the user experience. Amazon has updated the ALB and CLB so that customers can continue to use the CORS request with stickness. |
| cookielawinfo-checkbox-advertisement | 1 year | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Advertisement". |
| cookielawinfo-checkbox-analytics | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytic / Performance". |
| cookielawinfo-checkbox-functional | 11 months | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional". |
| cookielawinfo-checkbox-necessary | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Strictly Necessary". |
| cookielawinfo-checkbox-performance | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance". |
| cookielawinfo-checkbox-preferences | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Preferences." |
| elementor | never | This cookie is used by the website's WordPress theme. It allows the website owner to implement or change the website's content in real-time. |
| viewed_cookie_policy | 11 months | The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data. |
| Cookie | Duration | Description |
|---|---|---|
| CONSENT | 16 years 4 months | These cookies are set via embedded youtube-videos. They register anonymous statistical data on for example how many times the video is displayed and what settings are used for playback.No sensitive data is collected unless you log in to your google account, in that case your choices are linked with your account, for example if you click “like” on a video. |
| _ga | 2 years | This cookie is installed by Google Analytics. The cookie is used to calculate visitor, session, campaign data and keep track of site usage for the site's analytics report. The cookies store information anonymously and assign a randomly generated number to identify unique visitors. |
| _gat_gtag_UA_47200144_1 | 1 minute | This cookie is set by Google and is used to distinguish users. |
| _gid | 1 day | This cookie is installed by Google Analytics. The cookie is used to store information of how visitors use a website and helps in creating an analytics report of how the website is doing. The data collected including the number visitors, the source where they have come from, and the pages visted in an anonymous form. |
| _hjAbsoluteSessionInProgress | session | This cookie is used to count how many times a website has been visited by different visitors. This is done by assigning the visitor an ID, so the visitor does not get registered twice. |
| _hjFirstSeen | 30 minutes | This is set by Hotjar to identify a new user’s first session. It stores a true/false value, indicating whether this was the first time Hotjar saw this user. It is used by Recording filters to identify new user sessions. |
| _hjid | 1 year | This cookie is set by Hotjar. This cookie is set when the customer first lands on a page with the Hotjar script. It is used to persist the random user ID, unique to that site on the browser. This ensures that behavior in subsequent visits to the same site will be attributed to the same user ID. |
| _hjIncludedInPageviewSample | session | This cookie is used to detect whether the user navigation and interactions are included in the website’s data analytics. |
| Cookie | Duration | Description |
|---|---|---|
| IDE | 1 year 24 days | This cookie is used by Google DoubleClick and stores information about how the user uses the website and any other advertisement before visiting the website. This is used to present users with ads that are relevant to them according to the user profile. |
| NID | 6 months | This cookie is used to a profile based on user's interest and display personalized ads to the users. |
| test_cookie | 15 minutes | This cookie is set by doubleclick.net. The purpose of the cookie is to determine if the user's browser supports cookies. |
| VISITOR_INFO1_LIVE | 5 months 27 days | This cookie is set by Youtube it is used to track the information of the embedded YouTube videos on a website. |
| YSC | session | This cookies is set by Youtube and is used to track the views of embedded videos. |
| yt-remote-connected-devices | never | These cookies are set via embedded youtube-videos. |
| yt-remote-device-id | never | These cookies are set via embedded youtube-videos. |
| Cookie | Duration | Description |
|---|---|---|
| qtrans_front_language | 1 year | This cookie is set by qTranslate WordPress plugin. The cookie is used to manage the preferred language of the visitor. |