Choosing the right Glass Manufacturing Machine is not just a matter of output speed. Buyers must match the equipment to their product, factory space, energy supply, and quality targets. A bottle line, for example, needs different forming and inspection systems from a flat-glass operation. The details matter: furnace capacity, mold changes, control systems, spare-part access, and the time required to train operators.
“[Insert a verified, directly sourced quotation about equipment selection or process control],” says [verified expert’s full name], a glass-manufacturing specialist. This guide uses that practical perspective to compare seven machine types for global buyers. It looks at what each machine does, where it fits, and which specifications deserve closer review. No single option suits every plant.
Some trade-offs are easy to miss. A faster line may need more floor space or more skilled maintenance. A lower purchase price may not include installation, commissioning, or long-term service support. Buyers should check these points with suppliers and request clear, comparable specifications. This shortlist is a starting point, not a substitute for a site assessment. Small details can change the decision.
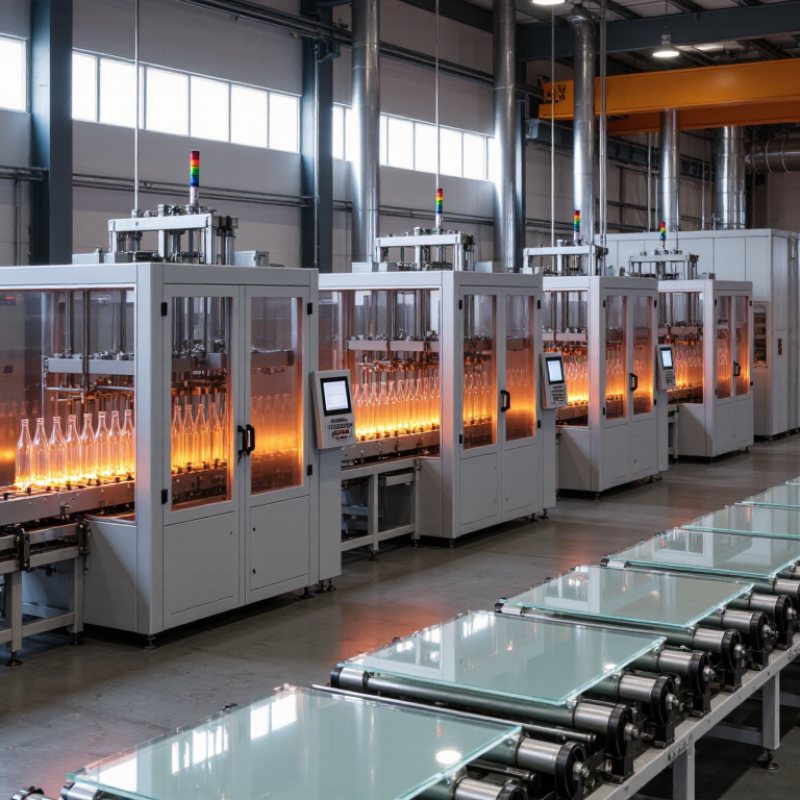
Glass manufacturing begins with carefully measured silica sand, soda ash, limestone, and recycled glass. Batch-mixing equipment blends these materials before they enter a furnace. Inside, high heat melts the mixture into a uniform liquid. Temperature stability matters: uneven heating can leave bubbles or stones that weaken finished products. Small changes matter.
The molten glass moves to forming equipment, where it becomes bottles, sheets, or other shapes. Methods differ, so buyers should match forming machines to product dimensions and expected output. The formed glass then passes through an annealing lehr. Controlled cooling reduces internal stress and helps prevent cracking later. Cutting, polishing, and inspection follow when the product requires them. It is easy to overfocus on furnace capacity; that can be a mistake if downstream equipment cannot keep pace. Heat is unforgiving.
Tips: Ask suppliers for operating ranges, energy-use data, and maintenance requirements. Check how inspection systems detect defects, such as bubbles or uneven edges. If possible, review sample products made at the proposed production speed. Specifications can look convincing on paper, but actual line balance deserves careful review.
Glass production lines rely on several machine categories, each controlling a different source of variation. Batch houses weigh and blend silica sand, soda ash, limestone, and recycled cullet before feeding the furnace. Consistent particle size and moisture help prevent unmelted grains and composition streaks. The European Commission’s 2013 Best Available Techniques Reference Document for the Manufacture of Glass identifies melting as the main energy-consuming stage, often accounting for about 60–80% of process energy. Furnace selection therefore affects fuel demand, glass quality, and operating flexibility.
Forming equipment shapes the melt: float lines make flat glass, while gob feeders supply container-forming machines. Annealing lehrs cool products gradually, reducing residual stress before inspection or cutting. Downstream options include cutting tables, edge processors, tempering furnaces, laminating lines, and optical inspection systems. Small details matter. Conveyor spacing and changeover time can decide whether nominal capacity works on a real shift. For buyers, throughput alone can mislead; a fast former adds little when the lehr becomes a bottleneck. Plant layouts differ, and generic line diagrams rarely show every constraint.
A glass plant depends on seven machines working as one process. The batch mixer blends silica sand, soda ash, limestone, and carefully prepared recycled glass, called cullet. The European Commission’s 2013 Glass Manufacturing BREF identifies melting as a major energy-consuming stage, so stable temperatures and furnace condition matter. Small errors travel. A forehearth then controls the glass temperature before it reaches forming.
A forming machine shapes the hot material into bottles, jars, or other products using molds or forming tools. The annealing lehr cools each item gradually, reducing internal stress that could cause cracks later. Cooling too quickly is costly. Operators should check temperature profiles, not just conveyor speed; the right settings depend on product thickness and glass composition.
At the cold end, inspection equipment checks for cracks, bubbles, and dimensional defects. Cutting and edge-finishing machines trim flat glass to size and smooth exposed edges. Eurostat reported that the EU recycled 75.9% of its glass packaging waste in 2022, making clean cullet preparation an important part of many production lines. Recycling rates do not tell every plant what to do. Contamination, color, and product specifications still shape the recipe, and those details are easy to underestimate.
Machine capacity should be compared as saleable output, not only the rated tonnes per day. Glass Alliance Europe’s 2023 industry figures report 39.1 million tonnes of EU glass production in 2022, across varied product types and production lines. That scale does not predict one factory’s needs. Ask suppliers for sustained output under your actual batch mix, changeover frequency, and planned maintenance hours. A fast forming machine can still be constrained by the furnace, feeder, or inspection station. Check the bottleneck.
Quality figures need context. Request defect rates by type, sampling method, and production period, rather than one headline percentage. For container lines, inspect how the system detects checks, inclusions, and dimensional variation. For flat glass, ask about thickness consistency, optical distortion, and edge quality. The European Commission’s 2013 Best Available Techniques Reference Document for the Manufacture of Glass treats emissions and energy use as important operating measures. Compare energy per tonne of saleable product, not just per tonne melted. Small differences add up.
Automation can improve repeatability, but it cannot fix every process weakness. Compare automatic inspection, recipe control, alarms, and production-data access. Ask for a live demonstration using representative glass and realistic line speeds. Watch how operators handle a false reject or a sudden temperature deviation. Also confirm whether staff can adjust settings safely without waiting for specialist support. More automation is not always better. I would weigh reliable recovery and clear records above impressive interface screens; that judgment may need revisiting after a site trial.
| Machine type | Typical capacity indicator | Quality factors to compare | Common automation level | Best suited for |
|---|---|---|---|---|
| Float glass production line | About 300–1,200 tonnes of glass per day, depending on line design and product mix. | Thickness and width consistency, optical distortion, surface defects, and furnace stability. | Very high; continuous process control, inspection, and material handling are commonly integrated. | Large-scale production of architectural, automotive, and other flat glass. |
| Container glass IS forming machine | Often specified by sections, cavities, and cycles per minute; output can range from hundreds of containers per minute across configured lines. | Weight variation, dimensional accuracy, wall distribution, finish quality, and defect rate. | High; electronic timing, automatic lubrication, and downstream inspection are common options. | Bottles and jars produced in repeatable, high-volume runs. |
| Glass tableware press-and-blow machine | Compare pieces per minute by product, mold count, and forming cycle; there is no single capacity figure across shapes and sizes. | Rim and base uniformity, shape repeatability, surface finish, and annealing compatibility. | Medium to high; automated forming and transfer can be paired with inspection and packing systems. | Tumblers, bowls, plates, and other pressed or pressed-and-blown glassware. |
| Flat glass tempering furnace | Typically compared in square metres per hour; throughput changes substantially with glass thickness, dimensions, and loading pattern. | Flatness, roller wave, optical distortion, edge quality, and compliance with the applicable safety-glazing standard. | Medium to high; recipes, temperature zones, and quench settings may be digitally controlled. | Safety glass for buildings, furniture, appliances, and selected vehicle applications. |
| Laminated glass production line | Compare square metres per hour by sheet size, interlayer, and cycle time; pre-press and autoclave stages affect total line output. | Bond strength, optical clarity, bubble control, edge quality, and interlayer placement. | Medium to high; automated loading, washing, film handling, and process recipes are available. | Safety, security, acoustic, and architectural laminated glass. |
| Insulating glass (IGU) production line | Compare completed units per shift and maximum panel dimensions; output depends on line layout, glass size, and unit complexity. | Spacer alignment, seal continuity, gas fill where specified, cleanliness, and unit thickness accuracy. | Medium to high; washing, positioning, pressing, and sealing can be integrated into one line. | Double- and triple-glazed units for windows, doors, and curtain walls. |
| CNC glass cutting table | Compare cutting speed, sheet size, loading time, and usable output per shift; nominal tool speed alone does not determine production capacity. | Cut accuracy, edge-break consistency, repeatability, cutting yield, and software nesting performance. | Medium to high; CNC patterns, automatic optimization, and optional loading or breakout systems reduce manual handling. | Flat glass processors needing accurate, repeatable cutting and efficient sheet use. |
Capacity figures are indicative comparison guides, not guaranteed machine specifications. Actual output depends on product dimensions, glass thickness, process settings, shift pattern, material handling, and the complete production-line configuration. Ask suppliers to quote capacity against the same product mix and acceptance criteria.
For global buyers, comparing glass manufacturing machines starts with the product, not the catalogue photo. A container-glass line, a tempering furnace, and a cutting table need very different floor space and utilities. Ask suppliers for confirmed output rates, acceptable glass thicknesses, energy use, and reference installations handling similar products. Check voltage, frequency, control-language options, and spare-parts lead times before signing. Small details matter. A control cabinet that fits the machine may not fit through your factory door.
Installation planning should include the building, not just the equipment. Confirm floor loading, foundation drawings, ceiling clearance, forklift access, and the route from unloading bay to production area. Arrange power, cooling water, compressed air, and extraction connections to the supplier’s specifications. Have a local electrician and mechanical engineer review those plans before shipment. Remote guidance can help, but it cannot fix a poorly prepared foundation. Allow time for commissioning and operator training; production targets may take weeks to reach.
Maintenance costs are easier to manage when routine checks are clear. Ask for lubrication schedules, wear-part lists, fault codes, and service procedures in a language your technicians can use. Keep critical consumables on site if replacement shipments take weeks. Record temperature, vibration, and downtime trends after startup. Real conditions can differ from a factory trial. A neat spreadsheet may still miss dust, shift changes, or inconsistent operator habits, so revisit the maintenance plan after the first production month.
Installation and maintenance planning considerations
Scores are qualitative planning estimates on a 1–5 scale, where 5 indicates greater installation complexity or maintenance intensity. Actual requirements vary with capacity, automation, site conditions, and operating schedule; confirm specifications with suppliers before procurement.
| Cookie | Duration | Description |
|---|---|---|
| AWSALB | 7 days | AWSALB is a cookie generated by the Application load balancer in the Amazon Web Services. It works slightly different from AWSELB. |
| AWSALBCORS | 7 days | This cookie is used for load balancing services provded by Amazon inorder to optimize the user experience. Amazon has updated the ALB and CLB so that customers can continue to use the CORS request with stickness. |
| cookielawinfo-checkbox-advertisement | 1 year | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Advertisement". |
| cookielawinfo-checkbox-analytics | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytic / Performance". |
| cookielawinfo-checkbox-functional | 11 months | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional". |
| cookielawinfo-checkbox-necessary | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Strictly Necessary". |
| cookielawinfo-checkbox-performance | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance". |
| cookielawinfo-checkbox-preferences | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Preferences." |
| elementor | never | This cookie is used by the website's WordPress theme. It allows the website owner to implement or change the website's content in real-time. |
| viewed_cookie_policy | 11 months | The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data. |
| Cookie | Duration | Description |
|---|---|---|
| CONSENT | 16 years 4 months | These cookies are set via embedded youtube-videos. They register anonymous statistical data on for example how many times the video is displayed and what settings are used for playback.No sensitive data is collected unless you log in to your google account, in that case your choices are linked with your account, for example if you click “like” on a video. |
| _ga | 2 years | This cookie is installed by Google Analytics. The cookie is used to calculate visitor, session, campaign data and keep track of site usage for the site's analytics report. The cookies store information anonymously and assign a randomly generated number to identify unique visitors. |
| _gat_gtag_UA_47200144_1 | 1 minute | This cookie is set by Google and is used to distinguish users. |
| _gid | 1 day | This cookie is installed by Google Analytics. The cookie is used to store information of how visitors use a website and helps in creating an analytics report of how the website is doing. The data collected including the number visitors, the source where they have come from, and the pages visted in an anonymous form. |
| _hjAbsoluteSessionInProgress | session | This cookie is used to count how many times a website has been visited by different visitors. This is done by assigning the visitor an ID, so the visitor does not get registered twice. |
| _hjFirstSeen | 30 minutes | This is set by Hotjar to identify a new user’s first session. It stores a true/false value, indicating whether this was the first time Hotjar saw this user. It is used by Recording filters to identify new user sessions. |
| _hjid | 1 year | This cookie is set by Hotjar. This cookie is set when the customer first lands on a page with the Hotjar script. It is used to persist the random user ID, unique to that site on the browser. This ensures that behavior in subsequent visits to the same site will be attributed to the same user ID. |
| _hjIncludedInPageviewSample | session | This cookie is used to detect whether the user navigation and interactions are included in the website’s data analytics. |
| Cookie | Duration | Description |
|---|---|---|
| IDE | 1 year 24 days | This cookie is used by Google DoubleClick and stores information about how the user uses the website and any other advertisement before visiting the website. This is used to present users with ads that are relevant to them according to the user profile. |
| NID | 6 months | This cookie is used to a profile based on user's interest and display personalized ads to the users. |
| test_cookie | 15 minutes | This cookie is set by doubleclick.net. The purpose of the cookie is to determine if the user's browser supports cookies. |
| VISITOR_INFO1_LIVE | 5 months 27 days | This cookie is set by Youtube it is used to track the information of the embedded YouTube videos on a website. |
| YSC | session | This cookies is set by Youtube and is used to track the views of embedded videos. |
| yt-remote-connected-devices | never | These cookies are set via embedded youtube-videos. |
| yt-remote-device-id | never | These cookies are set via embedded youtube-videos. |
| Cookie | Duration | Description |
|---|---|---|
| qtrans_front_language | 1 year | This cookie is set by qTranslate WordPress plugin. The cookie is used to manage the preferred language of the visitor. |