What Is the Best Aluminium Die Casting Machine in 2026?
Choosing the best Aluminium Die Casting Machine in 2026 is not a matter of picking the largest clamp force. The right choice depends on the alloy, component geometry, production volume, and acceptable scrap rate. A machine built for thin-walled automotive housings may be oversized or inefficient for smaller, lower-volume parts. There is no universal winner.
Demand gives this decision wider context. The IEA’s Global EV Outlook 2024 reports nearly 14 million electric car sales in 2023, about 35% more than in 2022. Many vehicle platforms use aluminium components to manage weight, although this trend alone does not determine which casting machine a factory needs. The International Aluminium Institute reported global primary aluminium production of about 70.6 million tonnes in 2023. That is a measure of industry scale, not a forecast of machine sales. The distinction matters.
A practical comparison should look beyond the machine’s headline tonnage. Shot capacity, injection control, repeatability, cycle time, energy use, die compatibility, and local service support all affect real production. Ask suppliers for trial results using a representative part, not only catalogue specifications. Check how they measure scrap and cycle time, too. Figures can be framed differently. One limitation remains: published market reports rarely compare machine performance under identical factory conditions. This guide therefore weighs specifications against operational evidence, while noting where buyer-specific testing is still essential. The “best” machine is the one that reliably meets your part and production requirements.
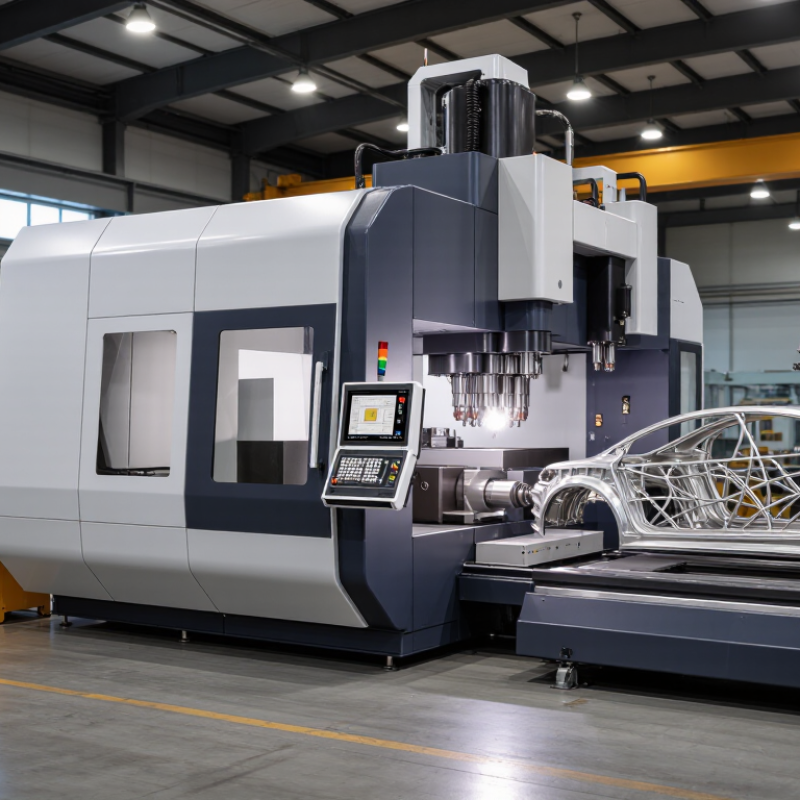
How Aluminium Die Casting Machines Work
An aluminium die casting machine turns molten metal into a shaped component by forcing it into a reusable steel die. The process starts with aluminium heated until it flows evenly. A measured shot enters the machine’s injection chamber, where a plunger drives it toward the closed die. Timing matters. Too much delay can cool the metal before it fills narrow ribs or thin sections.
Inside the die, pressure pushes the aluminium into small details, such as mounting holes and sharp corners. Cooling channels carry heat away while the metal solidifies. Then the die opens, and ejector pins release the casting. It sounds simple. It isn’t. A small change in metal temperature, injection speed, or die temperature can affect surface finish and filling quality.
Operators monitor these settings and inspect castings for issues such as incomplete filling, flash, or internal porosity. A bright surface does not prove that a part is sound; appearance alone can be misleading. After ejection, excess metal is trimmed, and critical dimensions may be checked with gauges. The machine controls much of the cycle, but setup and consistent maintenance still matter. Even a well-tuned process needs review when the part design or production conditions change.
Main Machine Types and Their Industrial Applications
What Is the Best Aluminium Die Casting Machine in 2026?
Main Machine Types and Their Industrial Applications
Machine choice starts with the part, not a headline tonnage figure. Cold-chamber high-pressure die casting is widely used for aluminium because the metal is melted separately and injected into a steel die. A fast shot fills thin ribs and detailed housings, making this process useful for automotive brackets, appliance frames, and electronic enclosures. It can produce high volumes. But die wear, porosity, and process control need attention.
Low-pressure die casting fills a die more gently, often through a riser tube. It suits wheels and other components where controlled filling and sound structure matter. Gravity die casting uses a simpler, slower pour and works well for medium-volume parts with thicker sections. Squeeze casting applies pressure as the metal solidifies, which can help reduce shrinkage in demanding components. Vacuum assistance may also improve filling in complex, thin-walled parts. Each option has trade-offs.
A practical evaluation should compare part geometry, annual volume, alloy, cycle time, and inspection needs. Even a capable machine can disappoint if the die design or temperature control is poor. The best fit is specific. Start with real part data.
Key Criteria for Evaluating Machines in 2026
What Is the Best Aluminium Die Casting Machine in 2026?
Key Criteria for Evaluating Machines in 2026
The best machine is the one that holds process conditions steady on your actual parts. Compare shot-to-shot repeatability, clamping-force margin, injection control, and die temperature stability. Ask suppliers to run your alloy and tooling, then review pressure curves, cycle times, scrap rates, and dimensional results. Peak speeds on a brochure prove little. Cycle time matters.
Energy use deserves close measurement. The International Aluminium Institute estimates that recycled aluminium requires about 5% of the energy used to produce primary aluminium. That figure describes metal production, not casting-machine consumption, so measure the machine separately: record energy per acceptable casting across a full production shift. Also assess uptime, maintenance access, spare-part availability, and the time needed for die changes. Check that safety systems and controls fit the operators’ real workflow. A machine can look efficient in a short trial and perform differently after warm-up or during a long run. I would treat supplier estimates as starting points, not guarantees; a documented trial using your own part mix is more convincing.
Leading Machine Options and Their Capabilities
In 2026, the best aluminium die-casting machine depends on part geometry, production volume, and available utilities. Cold-chamber machines are a common choice because molten aluminium enters the shot sleeve between cycles. They can produce structural housings and larger components, but performance depends on injection speed, clamping force, and die design. More tonnage is not always better. Oversizing can raise energy use and tooling costs.
For thin walls and detailed ribs, compare machines with responsive injection control and stable pressure profiles. Vacuum assist can help reduce trapped gas in suitable dies, while real-time monitoring can flag changes in cycle time or metal temperature. Servo-hydraulic systems offer controlled motion; electric configurations may provide precise repeatability, depending on machine size and service support. Robotic ladling and extraction can improve consistency in busy cells. But automation needs careful setup. That is easy to underestimate.
Tips: Request a trial with your actual alloy and part geometry. Review cycle time, scrap rate, shot-to-shot variation, and maintenance access, not just clamp force. Check local technical support, too. Keep reasonable capacity in reserve, but avoid buying for a hypothetical order.
How to Match a Machine to Production Requirements
Choosing the best aluminium die casting machine starts with the parts, not the largest tonnage on a sales sheet. Record each casting’s projected area, alloy, weight, wall thickness, and target cycle time. In cold-chamber production, clamping force must resist cavity pressure without encouraging unnecessary flash. Too much capacity can raise purchase and operating costs. A close estimate helps.
Next, check shot capacity, platen size, tie-bar spacing, and mold thickness against the actual tooling. Leave room for runners and overflows; a mold that fits on paper may be awkward to install. Match the injection system to the required fill speed and pressure, then confirm that controls can repeat those settings across shifts. Ask for trial data using a comparable part and alloy. A short demonstration can expose slow recovery or inconsistent fill that a specification sheet misses.
Plan around the whole cell, too. Consider ladling or dosing, extraction, trimming, cooling, and operator access. These details affect cycle time and safety more than many buyers expect. Check local service capability, spare-part lead times, energy use, and maintenance access. A spreadsheet can narrow the field, but it cannot reproduce a production run. Even experienced teams sometimes misjudge future volume, so compare today’s needs with realistic growth and available floor space.
What Is the Best Aluminium Die Casting Machine in 2026?
Match Clamping Force to Projected Area
This preliminary estimate assumes a cavity pressure of 40 MPa and a 20% sizing margin. It uses clamping force (kN) = projected area (cm²) × 4.8; projected area should include the casting and the projected runner and overflow areas. Actual machine selection depends on the alloy, die design, process conditions, and machine specifications, so confirm sizing with a qualified engineer.



 Português do Brasil
