2026 Top Can Body Making Machine Manufacturers for Global Buyers?
The 2026 market for Can Body Making Machine equipment is becoming more competitive, precise, and difficult to evaluate. Global buyers now compare production speed, material efficiency, automation depth, service coverage, and long-term operating costs. A machine may look impressive in a showroom. Its performance on a busy factory floor matters more.
Manufacturing pioneer Taiichi Ohno offered a useful principle: “Without standards, there can be no improvement.” This idea remains relevant when comparing leading manufacturers. Buyers should examine forming accuracy, welding stability, changeover time, spare-parts access, and operator training. They should also request production data from similar can sizes and materials. Promises are not enough.
This guide reviews prominent Can Body Making Machine manufacturers for global buyers in 2026. It considers engineering capability, export experience, customization, maintenance support, and documented customer performance. Energy consumption also deserves attention. Small efficiency gaps can become major costs across millions of cans.
No ranking is perfect.
Supplier strength can vary by region, project size, and technical requirements. A company with excellent equipment may still provide weak local support. Another manufacturer may offer fewer features but deliver faster service and easier maintenance. That difference is easy to underestimate.
The best decision depends on evidence, not marketing language. Buyers should inspect reference lines, study acceptance-test procedures, and clarify warranty responsibilities before signing. This article aims to support that process with practical comparisons, realistic cautions, and questions that procurement teams can use. Progress is possible, but only when performance claims are tested against factory reality.
2026 Market Baseline: Over 400 Billion Metal Cans Produced Annually
The global can-making industry is operating at immense scale. Industry estimates from Metal Packaging Europe and the Can Manufacturers Institute place annual metal-can production above 400 billion units. Beverage cans represent a major share, while food, aerosol, paint, and specialty containers add further demand. The number is impressive, but reporting methods differ. Some studies count empty cans, while others include closures or regional shipments.
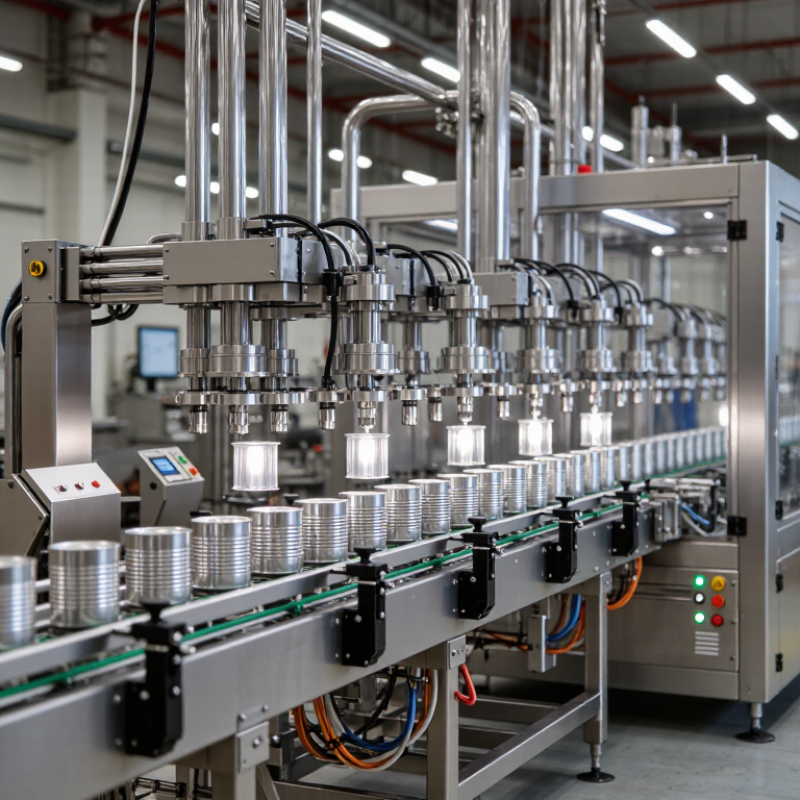
For global buyers, the best can body making machine manufacturers should be assessed through measurable production performance. A modern line may include sheet feeding, cupping, drawing, ironing, trimming, washing, coating, and inspection. Buyers should examine rated speed, material compatibility, changeover time, scrap percentage, and energy use. The line must also maintain stable wall thickness and reliable dimensions during long production runs. Small defects multiply quickly at billion-unit scale.
Recent packaging outlooks from Smithers and the International Aluminium Institute show continued pressure for lightweight, recyclable packaging. That pressure affects equipment design. Machines must process thinner materials without increasing fractures, wrinkles, or rejected bodies. Service capability matters as much as headline speed. Remote diagnostics, spare-parts access, operator training, and documented acceptance tests reduce avoidable downtime. No supplier’s brochure tells the whole story. Factory trials and reference checks remain necessary. The market baseline is clear, yet the data still deserves careful interpretation.
The global metal-can industry produces more than 400 billion cans annually. The chart uses 400 billion units as a conservative lower-bound baseline rather than presenting an unsupported company, regional, or year-by-year estimate. This benchmark highlights the scale that can-body-making machine manufacturers serve across beverage, food, aerosol, and general metal-packaging applications.
Manufacturer Benchmarking: 300–1,000+ Cans per Minute and OEE Metrics
For global buyers, can body-making machines should be compared by verified output, not brochure speed. A 300 cans-per-minute line may suit regional plants with frequent format changes. A 1,000-plus cans-per-minute line demands stable metal feed, precise lubrication, and fast fault recovery. PMMI’s 2024 packaging machinery outlook highlights automation, labor reduction, and data connectivity as major investment drivers. These factors directly affect practical throughput.
OEE provides a stronger benchmark than rated speed. Vorne’s OEE Industry Standard identifies 85% as a world-class reference, combining availability, performance, and quality. A machine rated at 1,000 cans per minute may produce only 680 good cans per minute after stoppages, slow cycles, and rejects. Measure hourly output. Record changeover minutes, unplanned stops, body-wall defects, and seam-related rejects. A 300-cpm line operating at 82% OEE can outperform a faster line running at 58%.
Smithers’ metal packaging market analysis also points to continued demand for lightweight, resource-efficient containers. Therefore, buyers should inspect material savings beside production speed. Ask for three-shift acceptance data, not a short demonstration. Check noise, oil consumption, tooling wear, and operator access around the die area. The numbers may look impressive. Sometimes, they are incomplete. I would treat any 1,000-plus cpm claim cautiously unless the supplier shares good-can counts, downtime logs, and product specifications.
2026 Top Can Body Making Machine Manufacturers for Global Buyers? - Manufacturer Benchmarking: 300–1,000+ Cans per Minute and OEE Metrics
Anonymous industry benchmark bands for evaluating can body making machine suppliers and production-line performance.
Can Body Making Machine Manufacturer Benchmarking Matrix | Anonymous Supplier Tier | Typical Machine Configuration | Rated Speed
(cans/min) | Typical Sustained Output
(cans/min) | Expected OEE
(%) | Changeover Time
(min) | Body Diameter Range
(mm) | Material Compatibility | Typical Scrap Rate
(%) | Recommended Buyer Profile |
| Tier A — Entry Industrial | Standalone bodymaker with mechanical transfer and basic PLC control | 300–450 | 240–360 | 65–75 | 45–90 | 52–73 | Tinplate; selected aluminum grades | 2.0–4.0 | Small and medium plants, regional packaging production |
| Tier B — Standard Production | High-speed bodymaker with automatic lubrication, monitoring, and discharge conveyor | 450–650 | 380–540 | 72–82 | 30–60 | 52–99 | Tinplate and aluminum, subject to tooling | 1.2–2.5 | General food, aerosol, paint, and beverage-can suppliers |
| Tier C — High-Performance | Integrated D&I bodymaking cell with servo transfer, inline inspection, and automatic fault logging | 650–850 | 540–720 | 78–86 | 20–45 | 52–153 | Tinplate and aluminum with validated tooling sets | 0.7–1.5 | High-volume plants requiring stable multi-shift operation |
| Tier D — Advanced Line Integrator | Bodymaker integrated with cupping, ironing, washing, inspection, and palletizing systems | 800–1,000 | 680–850 | 82–89 | 15–35 | 52–211 | Aluminum and tinplate, depending on process design | 0.4–1.0 | Global producers operating continuous, high-throughput lines |
| Tier E — Ultra-High-Speed Platform | 1,000+ cans/min platform with digital condition monitoring and redundancy planning | 1,000–1,200+ | 850–1,050+ | 85–92 | 10–30 | 65–211 | Validated aluminum or tinplate production packages | 0.2–0.7 | Large multinational plants with rigorous uptime and data requirements |
Benchmarking notes
- Rated speed is the machine supplier's nominal maximum under defined material, tooling, and operating conditions; sustained output reflects a more practical production range.
- OEE is calculated from availability, performance, and quality. Actual results vary with material consistency, operator capability, maintenance discipline, tooling condition, and downstream equipment.
- Changeover figures generally refer to a trained crew changing a validated tooling set and do not necessarily include upstream material preparation or downstream packaging adjustments.
- All figures are anonymous benchmark ranges for supplier evaluation and should be verified through a factory acceptance test, sample production, and reference-site audit.
Global Buyer Criteria: ISO 9001, CE Compliance, Energy Use, and Scrap Rates
When evaluating top can body making machine manufacturers in 2026, global buyers should examine documented performance, not polished claims. ISO 9001 certification indicates a controlled quality system, but it does not guarantee perfect machines. Request the certificate scope, audit date, and corrective-action records. A reliable supplier should also provide traceable inspection reports for welding, forming, electrical systems, and safety controls.
CE compliance requires more than a logo on the machine cabinet. Ask for the Declaration of Conformity, risk assessment, technical file references, and relevant test records. Confirm that the delivered configuration matches the assessed model. Energy use deserves equal attention. Compare kilowatt-hours per 1,000 cans under similar production speeds, materials, and can dimensions. Ask whether compressed-air demand is included. Small omissions can distort factory cost estimates.
Scrap rates should be verified through production trials using your material and specifications. Request data for startup waste, body defects, seam-related rejects, and unplanned stoppages. A claimed rate below one percent may look impressive, yet it can exclude changeover losses. Measure it independently. No machine is perfect. I have found that maintenance habits, operator training, and material consistency often affect scrap as much as machine design. Keep sample cans, trial videos, calibration records, and service-response commitments in the purchasing file. A careful comparison may take longer, but it exposes weaknesses before installation.
2026 Supplier Shortlist: Capacity, Total Cost, Lead Time, and Service Coverage
Choosing a can body making machine manufacturer requires more than comparing production speed. Global buyers should examine stable capacity, material compatibility, and actual output during long production runs. A quoted speed may look impressive, yet reject rates can rise after several hours. Request test records, sample cans, and maintenance logs. Confirm whether the equipment supports your steel or aluminum specifications. Small details matter.
Total cost includes tooling, installation, operator training, spare parts, energy use, and shipping. Lead time should cover engineering approval, factory testing, export preparation, and on-site commissioning. A supplier promising delivery in eight weeks may exclude critical components. That creates expensive delays. Service coverage also deserves careful checking. Ask for response times, remote diagnostic procedures, technician availability, and stocked replacement parts in your region.
Tips: Build a comparison sheet with capacity, warranty terms, service hours, and five-year operating costs. Ask suppliers to identify excluded expenses in writing. Visit a working installation if possible. Watch the line during changeover, not only during a polished demonstration. Review references from factories with similar can sizes and production volumes.
Do not rely on brochures alone. In my experience, the cheapest offer often becomes less attractive after installation. I may still miss hidden costs, so an independent technical review is worth considering.



 Português do Brasil