In 2026, global buyers need more than a low quotation when selecting Bms Wire Harness suppliers. Battery management systems depend on accurate sensing, stable connections, and consistent protection. A small crimping defect can create voltage-reading errors, production delays, or difficult field investigations. Quality begins with controlled materials, trained operators, and clear inspection records.
This guide examines leading Bms Wire Harness suppliers through practical purchasing criteria. These criteria include copper quality, insulation performance, connector compatibility, dimensional control, and testing capability. Supplier experience also matters. Teams that understand battery packs can identify routing risks before mass production begins. Look for documented traceability, sample validation, and responsive engineering support. Certifications may support confidence, but they should never replace direct evidence.
Details matter. A reliable supplier should explain terminal plating, wire specifications, pull-force results, and continuity testing. Ask how changes are approved. Ask how rejected parts are isolated. Ask whether production samples match approved drawings. Real factories sometimes have strong equipment but weak communication. Others communicate well but lack stable process control. That distinction is easy to miss.
No supplier is perfect. Buyer assumptions can also create risk. A harness designed for one battery enclosure may fail after a small layout change. Therefore, this overview encourages careful comparison rather than blind ranking. It focuses on evidence, repeatability, delivery discipline, and long-term cooperation. The strongest partner is not always the largest company. It is the supplier that can prove performance, admit limitations, and improve when problems appear. Expect practical insights for evaluating global suppliers with greater confidence in 2026.
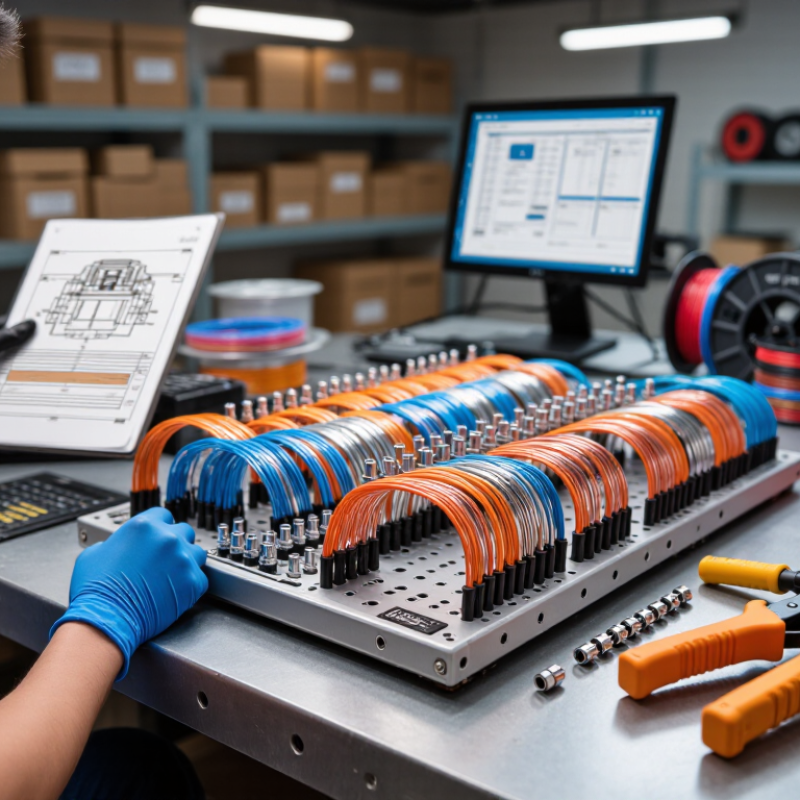
A BMS wire harness is a grouped set of wires, terminals, connectors, and protective sleeves. It links battery cells with the battery management system. The harness carries voltage, temperature, current, and balancing signals. It also supports controlled power distribution inside the battery pack.
In practical assembly work, routing quality affects reliability as much as conductor size. Wires must keep their bend radius near cell modules and avoid sharp metal edges. Abrasion sleeves, locking connectors, and strain reliefs reduce failures caused by vibration. Clear color coding and labeled branches help technicians trace faults faster. Small details matter.
These harnesses serve electric vehicles, energy storage cabinets, industrial equipment, medical backup systems, and low-voltage mobility products. High-temperature areas may require heat-resistant insulation and secured clips. Moist environments demand suitable sealing and corrosion-resistant terminals. A harness for a compact battery pack differs greatly from one used in a large storage enclosure.
It is easy to over-specify a harness. That can increase weight, cost, and assembly time without improving performance. The opposite mistake is riskier. A thin conductor, weak crimp, or loose connector can create unstable measurements. Supplier evaluation should include crimp testing, continuity testing, insulation checks, dimensional inspection, and traceable production records. Samples should also face realistic vibration, thermal cycling, and installation tests. Laboratory results help, but field feedback can reveal design weaknesses.
Choosing a BMS wire harness supplier in 2026 requires more than comparing unit prices. Examine crimp quality, insulation consistency, connector fit, and labeling accuracy. A reliable supplier should provide traceable material records and clear production controls. Ask for recent inspection reports, sample measurements, and process photographs. The harness must match your battery design, including current, temperature, vibration, and installation limits.
Request samples from the same production line used for mass orders. Check terminal retention with a pull test. Bend the cable near the connector repeatedly. Look for loose seals, exposed copper, or uneven overmolding. Review testing for continuity, insulation resistance, and high-potential safety. Supplier engineers should explain tolerances without vague promises. Communication speed matters when a drawing changes overnight.
Tips: Visit the factory if possible. Compare sample results with documented limits. Confirm packaging protects terminals from dust and moisture. Ask how rejected harnesses are isolated. No checklist is perfect. A polished sample can still hide weak process discipline, so repeat inspections during pilot production. Also, do not judge capacity only by equipment count. Staffing, maintenance records, and corrective-action history reveal more. A supplier that admits one recurring defect may be more trustworthy than one claiming flawless output. Evaluate evidence, not confidence.
| Evaluation Dimension | What Global Buyers Should Verify | Practical 2026 Benchmark | Recommended Evidence | Warning Sign | Suggested Weight |
|---|---|---|---|---|---|
| Electrical Design Capability | Ability to design low-voltage BMS harnesses for cell monitoring, temperature sensing, balancing circuits, current sensing and communication interfaces. | Documented design review process with controlled schematics, pin maps, wire lists and revision history. | Approved drawings, electrical test specifications, engineering change records and sample design packages. | Supplier relies only on customer drawings and cannot identify connector, polarity or creepage-related risks. | 15% |
| Connector and Terminal Quality | Compatibility of connectors and terminals with the battery pack environment, mating cycles, vibration, temperature and chemical exposure. | Connector and terminal selection supported by manufacturer datasheets, crimp specifications and applicable automotive qualification data. | Part datasheets, terminal pull-force results, crimp-height records and mating-cycle requirements. | Untraceable connector substitutions or mixed terminals from different component families. | 15% |
| Wire and Insulation Selection | Conductor size, insulation material, temperature rating, flexibility, abrasion resistance and compatibility with the battery enclosure. | Wire gauge, insulation rating and temperature range are selected from the electrical load, installation route and environmental profile. | Wire certificates, material declarations, conductor resistance data and thermal derating calculations. | Wire size is chosen only by nominal current without considering bundling, ambient temperature or voltage drop. | 12% |
| Crimping and Termination Control | Consistency of crimp height, crimp force, conductor brush, insulation support and terminal retention. | Crimp tooling is identified and maintained; first-article and in-process checks are recorded for each applicable terminal family. | Crimp-force monitoring records, cross-section analysis, pull-test results and tooling maintenance logs. | Manual crimping is used without validated tooling, standard work instructions or periodic pull testing. | 15% |
| Electrical Testing | Verification of continuity, short circuits, incorrect wiring, insulation resistance and dielectric withstand where required by the design. | 100% automated continuity and miswire testing for production harnesses, with traceable test results. | Tester program revision, test limits, calibration certificates and serialized or batch-level test records. | Only visual inspection is performed, or test results cannot be linked to a production lot. | 15% |
| Mechanical and Environmental Validation | Resistance to vibration, thermal cycling, humidity, abrasion, bending, connector retention and installation-related strain. | Validation plan reflects the battery pack’s actual temperature, vibration, humidity and routing conditions. | Validation reports, fixture descriptions, test conditions, acceptance criteria and failure-analysis records. | Generic laboratory reports are provided without confirming that the tested construction matches the production harness. | 12% |
| Quality Management | Effectiveness of production controls, nonconformance handling, corrective action and process auditing. | ISO 9001 certification is expected; IATF 16949 capability is advantageous for automotive or high-volume vehicle programs. | Valid certificates, process audit results, control plans, FMEA documents and corrective-action examples. | Expired certificates, missing process ownership or repeated defects without documented root-cause actions. | 10% |
| Compliance and Material Traceability | Control of restricted substances, material composition, product labeling and component traceability for international shipments. | Support for RoHS and REACH declarations; UL or other applicable wire and component approvals are verified by part number. | Declarations of conformity, material certificates, approval files, lot codes and supplier-change notifications. | Compliance statements are generic and do not identify the exact wire, terminal, connector or production site. | 8% |
| Production Capacity and Lead Time | Ability to support prototypes, pilot builds, ramp-up and recurring production without compromising process control. | Separate capacity plans for prototype and mass production, with documented standard lead times and capacity assumptions. | Capacity plan, equipment list, staffing plan, production schedule and historical on-time delivery data. | Capacity claims are based only on equipment count and do not account for labor, testing or bottleneck operations. | 8% |
| Supply Chain Resilience | Availability of terminals, connectors, wire, seals and protective materials, including contingency planning for shortages. | Approved alternatives are pre-qualified; critical components have documented lead-time monitoring and change-control procedures. | Approved vendor list, component risk matrix, buffer policy and business-continuity plan. | A single unapproved source is used for a critical connector or terminal with no substitution plan. | 5% |
| Documentation and Engineering Support | Speed and accuracy of drawing review, sample feedback, failure analysis and engineering change communication. | Controlled English-language documentation with clear revision status, response ownership and agreed engineering change timelines. | Sample submission package, change-notice template, response-time records and nonconformance reports. | Uncontrolled drawings, undocumented substitutions or design changes made without written approval. | 5% |
Global buyers need BMS wire harness suppliers that understand both battery systems and international production demands. A reliable supplier should provide clear drawings, stable connector sourcing, and documented crimping standards. Practical experience matters when harnesses face vibration, heat, moisture, and repeated assembly cycles.
Leading BMS wire harness suppliers usually support customized lengths, terminal layouts, insulation materials, and labeling. They should explain wire gauge choices instead of offering a generic product. Sample testing can reveal loose terminals, uneven stripping, or poor bend control. These small defects can become serious service problems. Ask for continuity testing, pull-force records, and inspection reports for each production batch.
Traceability builds confidence. Batch numbers, operator records, and material certificates help buyers investigate quality issues quickly. Suppliers serving multiple regions should understand packaging rules, electrical safety expectations, and documentation requirements. However, no supplier is perfect. A factory may have strong automation but weak engineering communication. Another may offer skilled assembly but limited capacity during peak demand. Buyers should review these gaps honestly before signing a long-term agreement. Factory audits, pilot orders, and direct technical discussions often reveal more than polished sales materials. Controls must work in real production, not only in presentations.
For global buyers, comparing BMS wire harness suppliers requires more than checking unit prices.
Quality should be visible in test records, not only sales presentations. Ask for crimp pull-force results, conductor resistance data, insulation checks, and thermal cycling reports. A reliable supplier can trace each harness to its materials, operator, tooling, and inspection date.
Small details matter. A loose terminal may create unstable battery readings.
Customization shows whether a supplier understands real battery-pack constraints.
Review cell spacing, wire gauges, connector locking force, thermistor placement, bend radius, and labeling requirements. Request production samples before approving large orders. The sample should match the final process, not a hand-built prototype.
Some suppliers promise flexibility but lack suitable tooling. That gap can appear after purchase.
Capacity and compliance need equal attention.
Check monthly output, available crimping machines, backup production lines, copper supply, and realistic lead times. Ask how the supplier handles urgent engineering changes. Compliance documents should cover applicable safety, environmental, and quality requirements for each destination market.
Confirm document validity independently. A certificate alone is not enough. I would also review corrective-action records and conduct a remote or on-site audit when possible.
No supplier is flawless. Even strong factories may show delayed traceability, inconsistent labeling, or weak change control. Those findings deserve honest discussion before commercial approval.
Global sourcing for a BMS wire harness should begin with application facts, not supplier rankings. The IEA Global EV Outlook 2024 projected more than 17 million electric car sales worldwide in 2024. That growth increases demand for stable, traceable battery connections. Define voltage, continuous current, temperature range, bend radius, connector sealing, and expected service life before requesting quotations. A two-page technical brief prevents vague comparisons.
Request samples from at least three qualified suppliers. Check conductor size, insulation material, terminal plating, locking force, and branch dimensions. Require crimp cross-sections, pull-force results, continuity tests, insulation resistance, and high-voltage testing where applicable. IPC/WHMA-A-620 provides recognized workmanship guidance for cable and wire harness assemblies. Ask for process control plans, lot traceability, change-notification rules, and corrective-action records. Factory audits should review crimp machines, calibration labels, operator training, and incoming inspection.
Cost deserves attention, but it should not dominate the scorecard. The IEA reported that battery demand for electric vehicles approached 750 GWh in 2023, showing how small harness defects can affect large production volumes. Compare tooling ownership, minimum order quantities, lead times, packaging, and logistics risk. A pilot order should include vibration, thermal cycling, moisture, and repeated mating tests. No scorecard is perfect. A first sample may pass electrically and still fail during assembly because its branches bend poorly. Keep that lesson visible. Review supplier performance monthly, and retain a qualified second source before production pressure arrives.
| Cookie | Duration | Description |
|---|---|---|
| AWSALB | 7 days | AWSALB is a cookie generated by the Application load balancer in the Amazon Web Services. It works slightly different from AWSELB. |
| AWSALBCORS | 7 days | This cookie is used for load balancing services provded by Amazon inorder to optimize the user experience. Amazon has updated the ALB and CLB so that customers can continue to use the CORS request with stickness. |
| cookielawinfo-checkbox-advertisement | 1 year | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Advertisement". |
| cookielawinfo-checkbox-analytics | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytic / Performance". |
| cookielawinfo-checkbox-functional | 11 months | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional". |
| cookielawinfo-checkbox-necessary | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Strictly Necessary". |
| cookielawinfo-checkbox-performance | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance". |
| cookielawinfo-checkbox-preferences | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Preferences." |
| elementor | never | This cookie is used by the website's WordPress theme. It allows the website owner to implement or change the website's content in real-time. |
| viewed_cookie_policy | 11 months | The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data. |
| Cookie | Duration | Description |
|---|---|---|
| CONSENT | 16 years 4 months | These cookies are set via embedded youtube-videos. They register anonymous statistical data on for example how many times the video is displayed and what settings are used for playback.No sensitive data is collected unless you log in to your google account, in that case your choices are linked with your account, for example if you click “like” on a video. |
| _ga | 2 years | This cookie is installed by Google Analytics. The cookie is used to calculate visitor, session, campaign data and keep track of site usage for the site's analytics report. The cookies store information anonymously and assign a randomly generated number to identify unique visitors. |
| _gat_gtag_UA_47200144_1 | 1 minute | This cookie is set by Google and is used to distinguish users. |
| _gid | 1 day | This cookie is installed by Google Analytics. The cookie is used to store information of how visitors use a website and helps in creating an analytics report of how the website is doing. The data collected including the number visitors, the source where they have come from, and the pages visted in an anonymous form. |
| _hjAbsoluteSessionInProgress | session | This cookie is used to count how many times a website has been visited by different visitors. This is done by assigning the visitor an ID, so the visitor does not get registered twice. |
| _hjFirstSeen | 30 minutes | This is set by Hotjar to identify a new user’s first session. It stores a true/false value, indicating whether this was the first time Hotjar saw this user. It is used by Recording filters to identify new user sessions. |
| _hjid | 1 year | This cookie is set by Hotjar. This cookie is set when the customer first lands on a page with the Hotjar script. It is used to persist the random user ID, unique to that site on the browser. This ensures that behavior in subsequent visits to the same site will be attributed to the same user ID. |
| _hjIncludedInPageviewSample | session | This cookie is used to detect whether the user navigation and interactions are included in the website’s data analytics. |
| Cookie | Duration | Description |
|---|---|---|
| IDE | 1 year 24 days | This cookie is used by Google DoubleClick and stores information about how the user uses the website and any other advertisement before visiting the website. This is used to present users with ads that are relevant to them according to the user profile. |
| NID | 6 months | This cookie is used to a profile based on user's interest and display personalized ads to the users. |
| test_cookie | 15 minutes | This cookie is set by doubleclick.net. The purpose of the cookie is to determine if the user's browser supports cookies. |
| VISITOR_INFO1_LIVE | 5 months 27 days | This cookie is set by Youtube it is used to track the information of the embedded YouTube videos on a website. |
| YSC | session | This cookies is set by Youtube and is used to track the views of embedded videos. |
| yt-remote-connected-devices | never | These cookies are set via embedded youtube-videos. |
| yt-remote-device-id | never | These cookies are set via embedded youtube-videos. |
| Cookie | Duration | Description |
|---|---|---|
| qtrans_front_language | 1 year | This cookie is set by qTranslate WordPress plugin. The cookie is used to manage the preferred language of the visitor. |